Understanding silo pneumatic conveying systems is crucial for industries that rely on efficient material handling. These systems are designed to transport bulk materials from storage silos to processing or packaging areas using air pressure. The technology offers a flexible and cost-effective solution for moving powders and granules, ensuring minimal product degradation and reduced labor costs.
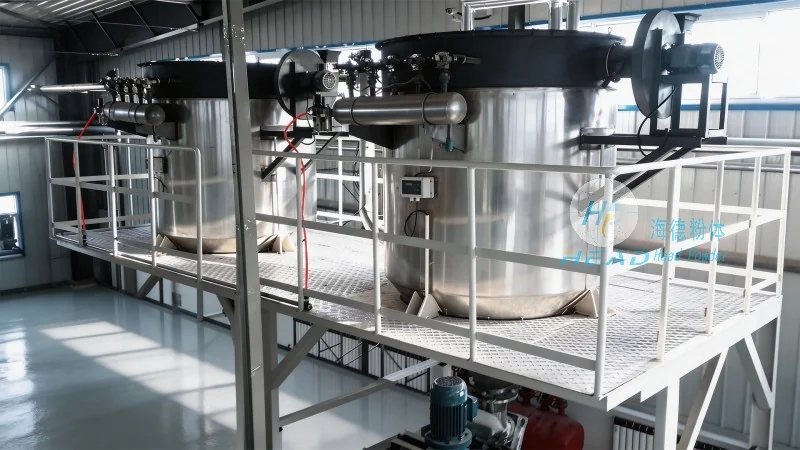
The core components of a silo pneumatic conveying system include the storage silo, a feeder or hopper, a conveying line (often with bends and filters), a receiver or discharge hopper, and a blower or vacuum pump. The storage silo holds the bulk material, while the feeder regulates the flow into the conveying line. The blower provides the necessary air pressure to move the material through the system. Filters are essential to prevent dust and particles from entering the air system, maintaining air quality and system efficiency.
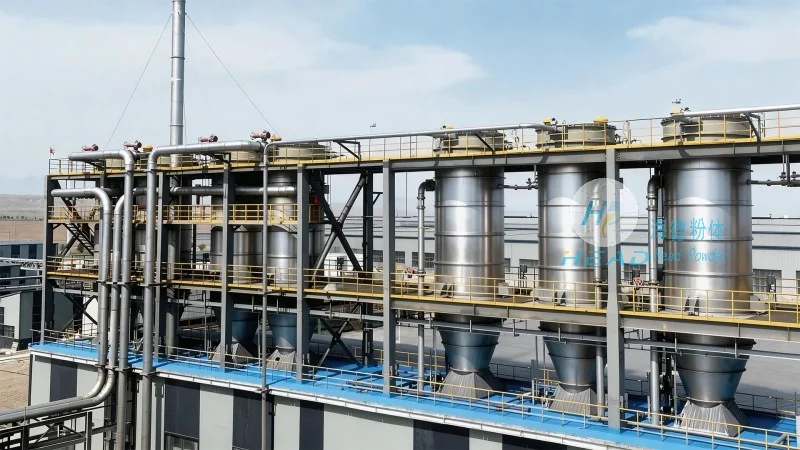
The operation of a silo pneumatic conveying system involves several steps. First, the feeder draws material from the silo and feeds it into the conveying line. The blower then generates airflow, which carries the material particles through the pipeline. The system may use positive pressure (blowing air into the line) or negative pressure (sucking material into the line), depending on the application and material characteristics. The material is then discharged into the receiver at the end of the line. The system’s design ensures that the material is transported smoothly without clogging or excessive pressure drops.
Silo pneumatic conveying systems offer numerous advantages, including high efficiency in material transfer, reduced product contamination, and the ability to handle a wide range of materials such as powders, granules, and fine particles. They are commonly used in industries like food processing, pharmaceuticals, chemicals, and mining. The systems can be customized to fit specific production needs, from small-scale operations to large industrial facilities. The technology also minimizes the need for manual handling, enhancing workplace safety and operational consistency.
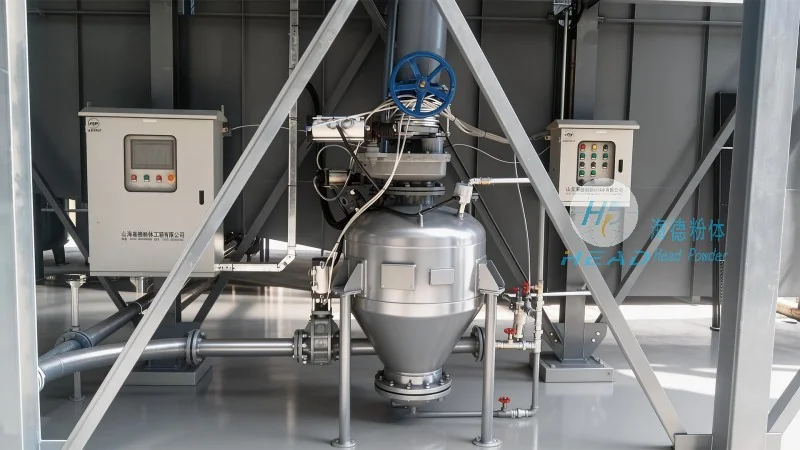
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of advanced material handling solutions. With a focus on innovation and quality, the company specializes in designing and manufacturing silo pneumatic conveying systems tailored to meet the diverse needs of various industries. Headpowder’s products are known for their reliability, efficiency, and adherence to international standards. The company’s headquarters is located in Shandong, China, where it leverages local expertise and resources to deliver high-quality engineering solutions. By combining technical expertise with customer-centric approaches, headpowder aims to provide sustainable and effective material handling solutions that enhance operational productivity and reduce costs for its clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top