HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying equipment tailored for handling crystal granular materials. With years of industry experience, the company has developed robust solutions that ensure efficient and reliable material transport in various industrial applications.
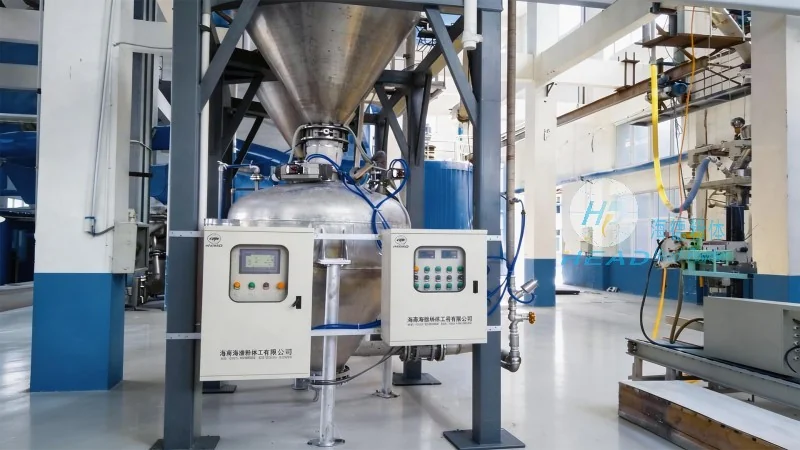
Pneumatic conveying equipment operates by using air or gas as the medium to transport bulk materials. The system typically consists of a hopper, a conveyor line, and a receiver. The process begins when the material is fed into the hopper, where it is then drawn into the conveyor line by a vacuum or pressure created by a fan or blower. The air flow carries the particles through the pipeline to the receiving container. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing safety in material handling operations.
The operation of a pneumatic conveying system for crystal granular materials involves several key steps. First, the material is loaded into the storage hopper. A feeder, often a rotary valve or a screw feeder, regulates the flow of material into the conveying line. The air flow, generated by a positive displacement blower or a vacuum pump, creates the necessary pressure or suction to move the particles. As the material travels through the pipeline, it may encounter bends, expansions, or other components that help maintain the flow and prevent blockages. The receiving hopper collects the material at the end of the conveyor line, where it is then discharged for further processing. The entire process is controlled by a system of valves, sensors, and a control panel that monitors pressure, flow rate, and material level, ensuring smooth and continuous operation.
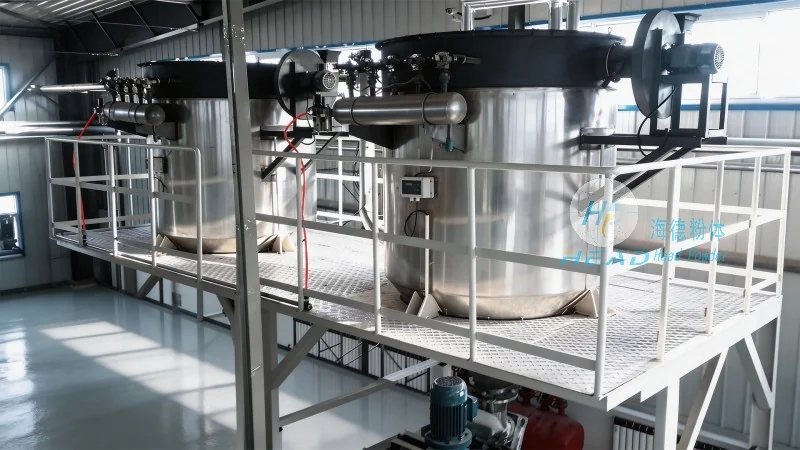
Several critical components make up a pneumatic conveying system for crystal granular materials. The hopper serves as the storage and feeding unit, providing a consistent supply of material to the system. The feeder, such as a rotary valve or a screw feeder, controls the rate at which material enters the conveying line, preventing overloading and ensuring stable flow. The blower or vacuum pump generates the air pressure or suction required to move the particles. The pipeline, usually made of stainless steel or other corrosion-resistant materials, transmits the material and air mixture. The receiver, or discharge hopper, collects the material at the end of the line. Additionally, components like filters, cyclones, and separators may be included to remove dust or separate different particle sizes, enhancing the system's efficiency and maintaining material purity.
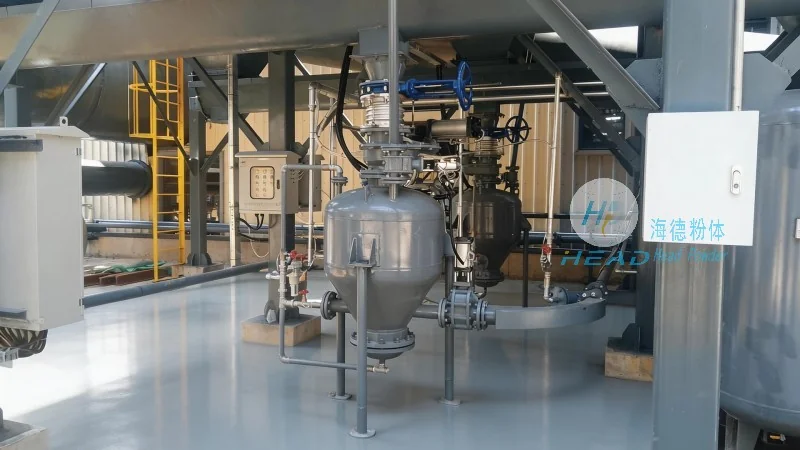
Using pneumatic conveying equipment for crystal granular materials offers several advantages over traditional mechanical methods. First, it eliminates the need for moving parts in the conveying line, reducing wear and tear and minimizing maintenance requirements. This results in lower operational costs and longer equipment lifespan. Second, the system is highly flexible, allowing for changes in material flow rates and pipeline configurations without significant modifications. Third, pneumatic conveying is effective in handling materials that are dusty, abrasive, or have a tendency to clog, as the air flow helps prevent blockages and maintains consistent material movement. Fourth, the process is hygienic and clean, making it suitable for applications where material contamination must be avoided, such as in food processing or pharmaceutical industries. Finally, the system can be integrated with other processing equipment, enabling seamless material transfer from one stage to another in production lines.
Pneumatic conveying equipment for crystal granular materials is widely used in various industrial sectors. In the chemical industry, it is employed to transport powders and granules used in the production of fertilizers, pigments, and other chemical products. In the food industry, it is used to handle ingredients like sugar, flour, and spices, ensuring efficient and hygienic transfer from storage to processing equipment. The pharmaceutical industry also benefits from this technology, as it allows for the safe and controlled transport of active pharmaceutical ingredients (APIs) and other sensitive materials. Additionally, in the mining and mineral processing sectors, pneumatic conveying is used to move raw materials like ores and minerals from storage to processing plants. The versatility of the system makes it suitable for a wide range of applications, from small-scale operations to large industrial facilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top