HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, production, and supply of advanced vacuum suction type material pneumatic conveying machines. These systems are engineered to efficiently transport bulk materials over long distances with minimal operational issues. The following article provides a detailed overview of the operation process and working principles of such equipment, highlighting its key components and functional mechanisms.
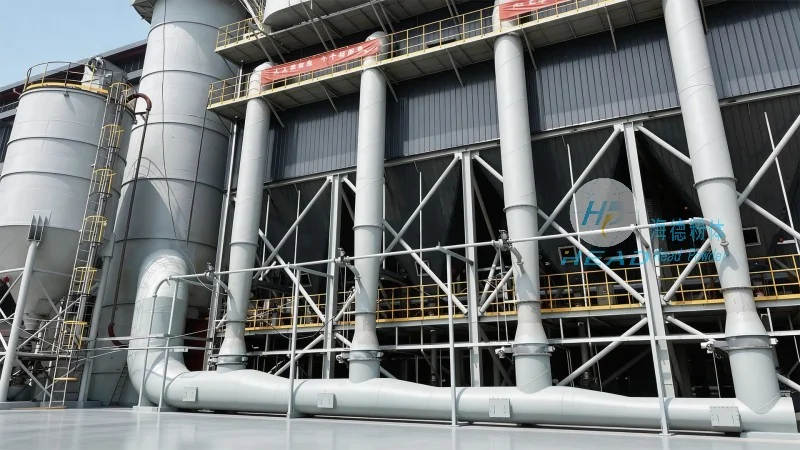
Overview of Vacuum Suction Pneumatic Conveying Systems
Vacuum suction type pneumatic conveying systems are widely used in various industries for the safe and efficient handling of powders, granules, and other bulk materials. Unlike positive pressure systems that use compressed air to push material, vacuum systems operate by creating a negative pressure environment that draws material from the source to the destination. This approach offers several advantages, including lower energy consumption, reduced material degradation, and improved safety in environments where dust is a concern.
Key Components and Their Functions
The vacuum suction pneumatic conveying machine consists of several critical components that work in tandem to achieve material transport. The main parts include the material feed hopper, vacuum pump, conveying line, material separator, and discharge hopper. Each component plays a vital role in the overall system performance:
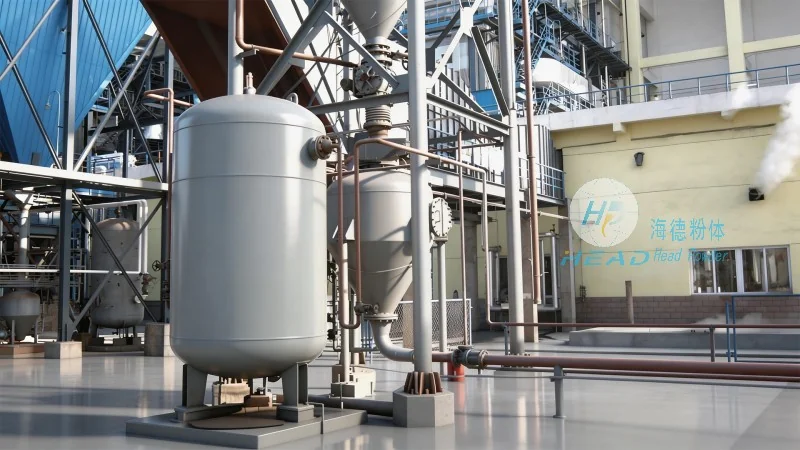
- Material Feed Hopper: This is where the bulk material is stored before being fed into the system. It typically features a hopper with a feeding valve that controls the flow rate of the material. The design of the hopper is crucial to prevent material bridging and ensure a consistent feed.
- Vacuum Pump: The heart of the vacuum system, the pump creates a negative pressure within the conveying line. This pressure differential draws the material from the feed hopper through the pipeline. The choice of pump type (e.g., rotary vane, liquid ring) depends on the material characteristics and system requirements.
- Conveying Line: Made of durable materials like stainless steel or PVC, the conveying line transports the material and air mixture. The line is designed to withstand the pressure differences and material abrasion. Proper sealing and maintenance of the line are essential to prevent air leaks and ensure efficient operation.
- Material Separator: As the material reaches the destination, the separator separates the material from the air stream. This component typically uses cyclonic or bag filter technology to capture the material and return it to the discharge hopper while releasing clean air back into the environment.
- Discharge Hopper: The final container where the conveyed material is collected. It is designed to handle the material flow and prevent spillage, ensuring a smooth end-of-line process.
Operation Process of the Vacuum Suction System
The operation of a vacuum suction type material pneumatic conveying machine follows a systematic process. Here is a step-by-step breakdown of how the system functions:
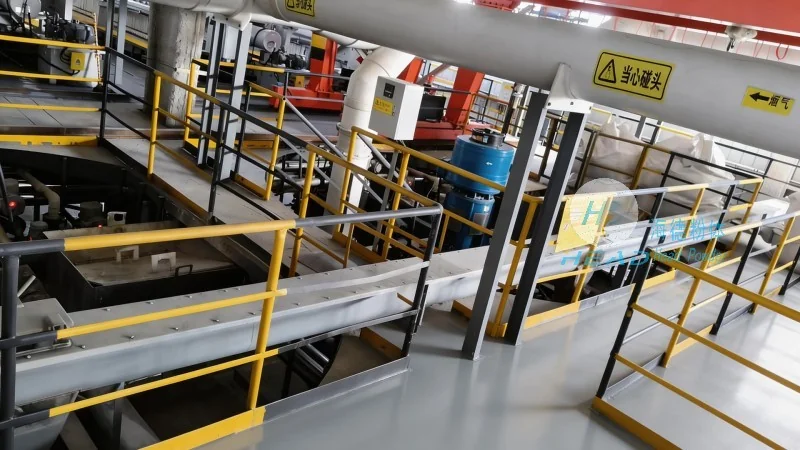
- Material Loading: The bulk material is loaded into the feed hopper. The hopper is equipped with a feeding valve that controls the material flow rate. This step ensures a steady supply of material to the system.
- Vacuum Creation: The vacuum pump is activated, creating a negative pressure in the conveying line. This pressure difference draws the material from the feed hopper into the line.
- Material Transport: As the vacuum is maintained, the material is pulled through the conveying line along with the air. The air acts as a carrier, suspending the material particles and facilitating their movement.
- Material Separation: At the destination, the material separator separates the material from the air stream. The material is collected in the discharge hopper, while the air is filtered and released.
- Cycle Completion: The system continues to operate in a continuous cycle, with the vacuum pump maintaining the pressure differential and the feeding valve controlling the material flow. This cycle ensures efficient and consistent material transport.
Working Principle: How the System Transfers Material
The working principle of the vacuum suction pneumatic conveying machine is based on the principles of fluid dynamics and pressure differentials. The system operates by creating a pressure gradient between the source (feed hopper) and the destination (discharge hopper). The vacuum pump generates a low pressure in the conveying line, which is lower than the atmospheric pressure at the source. This pressure difference causes the material to be drawn into the line by the air flow. The air, acting as a carrier, suspends the material particles and transports them to the destination. The separator then separates the material from the air, completing the process.
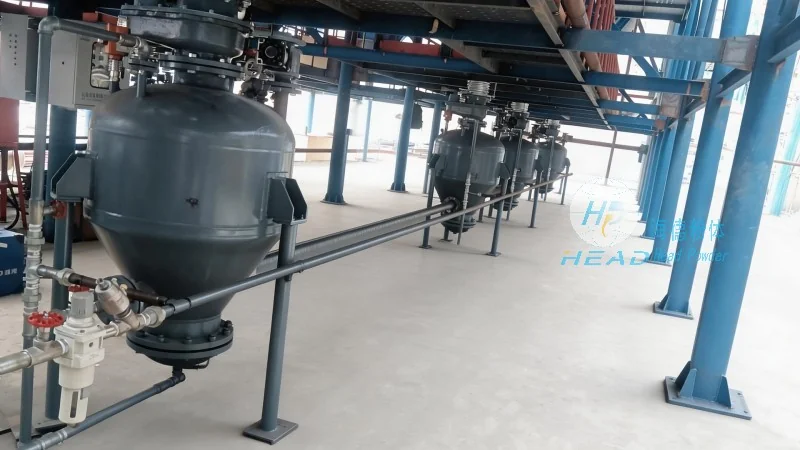
Advantages of Vacuum Suction Pneumatic Conveying
Vacuum suction type material pneumatic conveying systems offer several advantages over other material handling methods. These include:
- Energy Efficiency: The systems consume less energy compared to positive pressure systems, as they rely on the vacuum pump rather than compressed air.
- Reduced Material Degradation: The low pressure and gentle air flow minimize material attrition, making the system suitable for delicate or sensitive materials.
- Improved Safety: The negative pressure environment reduces the risk of dust explosions and inhalation hazards, making it safer for operators and the environment.
- Flexibility in Layout: The system can be configured to handle long-distance or complex layouts, as the vacuum pump can maintain the pressure differential over extended pipelines.
Applications and Industries
Vacuum suction pneumatic conveying machines are used in a wide range of industries, including food processing, pharmaceuticals, chemicals, and mining. They are particularly suitable for applications where material handling needs to be clean, efficient, and safe. Some common applications include transporting flour, sugar, powders, and granules in food processing plants, as well as handling powders and granules in chemical and pharmaceutical manufacturing.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China
