Quantitative weighing pneumatic conveying equipment plays a crucial role in modern industrial processes, particularly in sectors that require precise material handling and transportation. This equipment is designed to efficiently transport bulk materials while ensuring accurate weight measurement, making it indispensable for applications ranging from food processing to chemical manufacturing. The integration of pneumatic conveying technology with precise weighing mechanisms allows for seamless material transfer, enhancing operational efficiency and product quality.
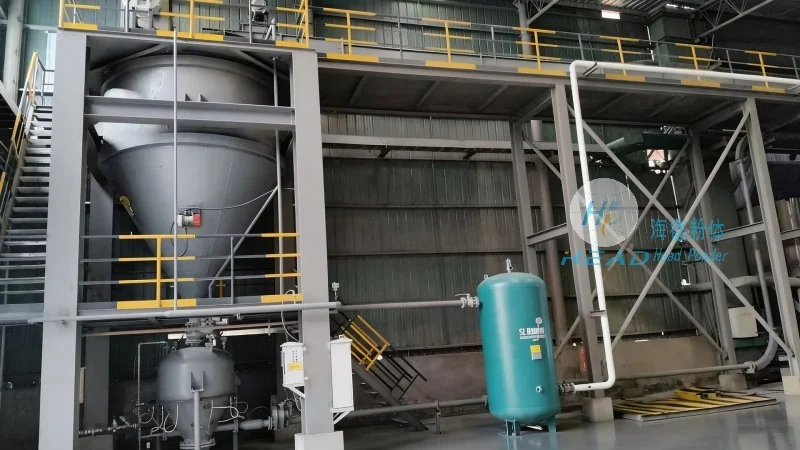
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced pneumatic conveying systems. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for industries seeking reliable and efficient material handling solutions. HeadPowder's expertise lies in creating customized equipment that meets the specific needs of clients, ensuring optimal performance and durability in various operational environments.
The quantitative weighing pneumatic conveying system typically consists of several critical components that work in tandem to achieve precise material transport. These include a hopper for material storage, a weighing scale integrated with the hopper to monitor weight, a pneumatic conveyor system for material transport, and a control unit to regulate the entire process. Each component is engineered to ensure seamless operation and accurate performance, contributing to the overall efficiency of the system.
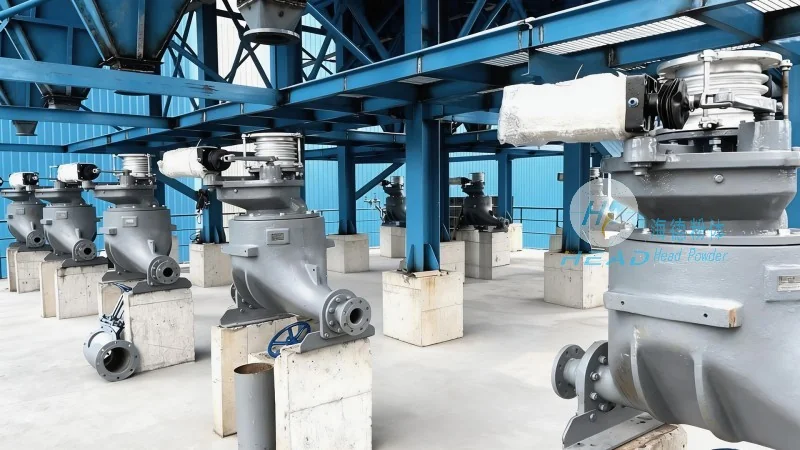
The operation of quantitative weighing pneumatic conveying equipment follows a systematic process that ensures precise material transfer. Initially, bulk materials are loaded into the hopper. The weighing scale then measures the weight of the material in the hopper, providing real-time data to the control unit. Once the desired weight is reached, the control unit activates the pneumatic conveyor system, which uses compressed air to transport the material from the hopper to the discharge point. The system continuously monitors the weight and adjusts the conveying rate as needed to maintain the target weight, ensuring consistent and accurate material delivery.
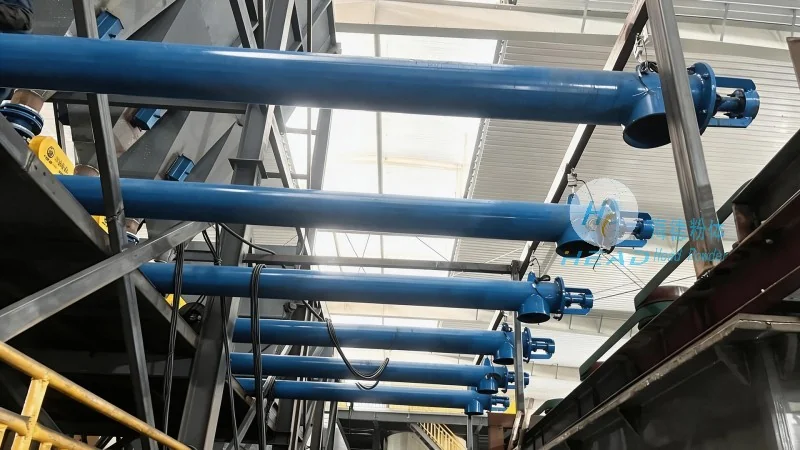
The working principle of quantitative weighing pneumatic conveying equipment is based on the combination of pneumatic conveying technology and precise weighing mechanisms. The pneumatic system uses compressed air to create a flow that propels the material through the conveying lines. Simultaneously, the weighing scale within the hopper measures the material's weight, allowing the control unit to regulate the conveying rate. This integration enables the equipment to deliver materials in precise quantities, eliminating the need for manual intervention and reducing the risk of errors. The system's ability to maintain consistent weight and flow rates makes it ideal for applications where accuracy is paramount.
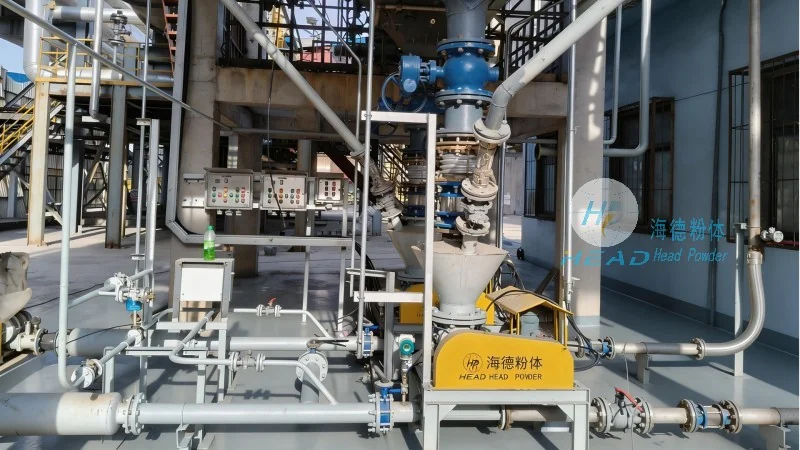
Quantitative weighing pneumatic conveying equipment offers several advantages over traditional material handling methods. Firstly, it provides high accuracy in material weighing, ensuring that the correct amount of material is transported to the destination. Secondly, the pneumatic system allows for continuous and automated material transfer, reducing labor costs and increasing operational efficiency. Additionally, the equipment is suitable for handling a wide range of materials, including powders, granules, and bulk solids, making it versatile for various industrial applications. The integration of weighing and conveying capabilities also minimizes material loss and contamination, enhancing product quality and safety.
Quantitative weighing pneumatic conveying equipment is widely used in various industrial sectors due to its versatility and efficiency. In the food industry, it is used for transporting ingredients such as flour, sugar, and spices with high precision, ensuring consistent product quality. In the chemical industry, the equipment handles chemicals and reagents, maintaining safety and accuracy in material handling. The pharmaceutical industry also benefits from this technology, as it enables the precise transfer of active ingredients and excipients, critical for drug formulation. Furthermore, in the mining and construction sectors, the equipment is used for transporting bulk materials like ores and aggregates, improving operational efficiency and reducing downtime.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top