HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems for transporting cement auxiliary materials. This article provides a detailed overview of the operation process and working principle of such systems, highlighting their efficiency and reliability in industrial applications.
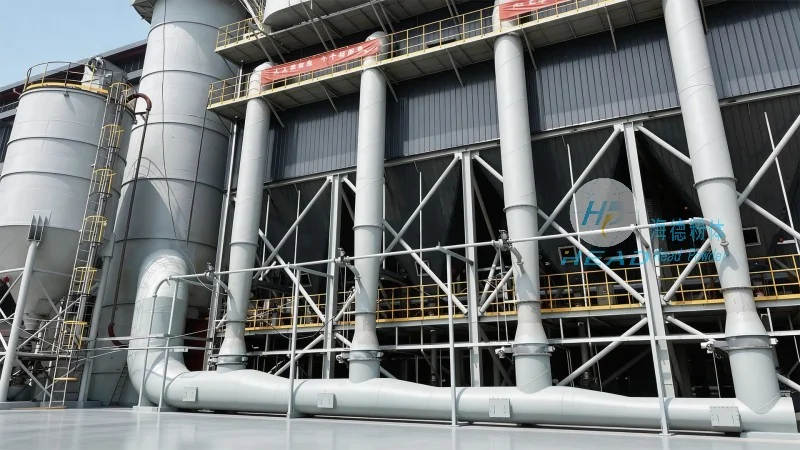
Introduction to Pneumatic Conveying Systems for Cement Auxiliary Materials
Cement auxiliary materials, including limestone, gypsum, and fly ash, are essential components in the production of high-quality cement. Traditional methods like belt conveyors or bucket elevators often face challenges such as material degradation, dust pollution, and high maintenance costs. Pneumatic conveying systems offer a more efficient and hygienic solution by transporting bulk materials through a pipeline using air pressure or suction. HeadPowder's expertise lies in developing customized solutions tailored to the specific needs of cement plants, ensuring optimal performance and minimal operational disruptions.
Working Principle of Pneumatic Conveying Systems
The core of a pneumatic conveying system is the ability to transport solid particles (auxiliary materials) suspended in a stream of air. The system operates based on the principle of fluidization, where the air flow creates a low-density mixture of particles and gas. There are two primary types of pneumatic conveying systems: positive pressure and negative pressure (or vacuum) systems.
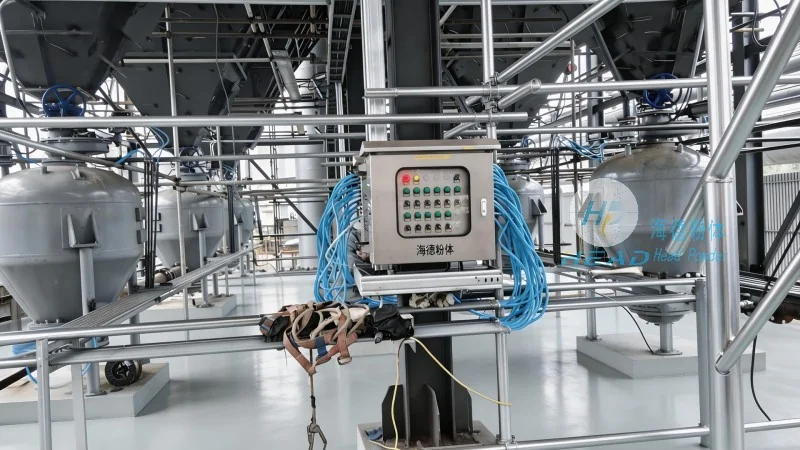
Positive pressure systems use a blower or compressor to generate air pressure, pushing the material through the pipeline. The air is introduced at the inlet, and the material is drawn into the air stream as it moves through the pipeline. This method is suitable for long-distance and high-capacity transport, as it can maintain consistent pressure and flow rates. Negative pressure systems, on the other hand, use a vacuum pump to create a suction effect, drawing the material from the source and transporting it to the destination. These systems are ideal for applications requiring low dust emission and are often used for short-distance or low-capacity transport.
Key Components of a Pneumatic Conveying System
HeadPowder's pneumatic conveying systems consist of several critical components that work in tandem to ensure smooth operation. These include:
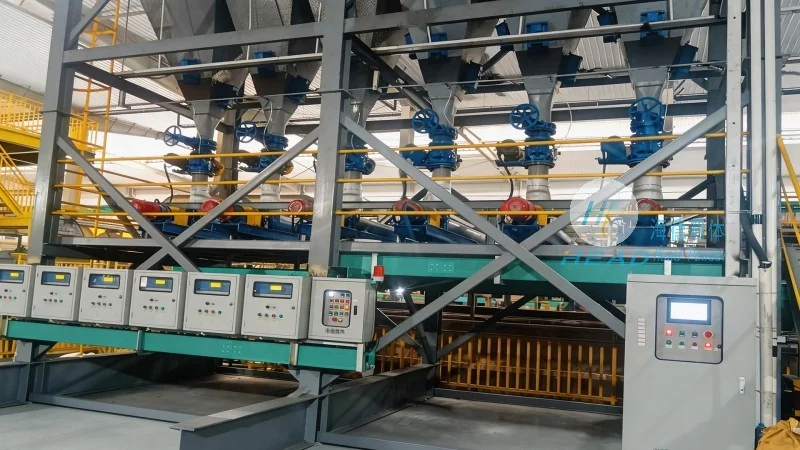
- Feeder: The feeder is responsible for feeding the auxiliary material into the system at a controlled rate. It ensures a consistent flow of material, preventing blockages and maintaining system efficiency.
- Conveying Pipeline: The pipeline is the main channel through which the material and air travel. It is typically made of stainless steel or other corrosion-resistant materials to withstand the abrasive nature of cement particles and prevent material buildup.
- Air Supply Unit: This unit provides the necessary air pressure or vacuum for the system. It includes components such as blowers, compressors, or vacuum pumps, depending on the system type. The air supply unit is designed to deliver clean, dry air to avoid contamination of the material.
- Separation and Collection Equipment: At the end of the pipeline, the material is separated from the air using a separator or cyclone. The separated material is then collected in a hopper or silo, while the air is filtered and discharged or recirculated.
- Control System: A sophisticated control system monitors and regulates the operation of the pneumatic conveying system. It includes sensors for pressure, flow, and level, as well as control valves and actuators. The system ensures that the conveying process is optimized, and any abnormalities are detected and addressed promptly.
Operation Process of a Pneumatic Conveying System
The operation process of a pneumatic conveying system involves several steps, from material feeding to final collection. Here is a step-by-step breakdown:
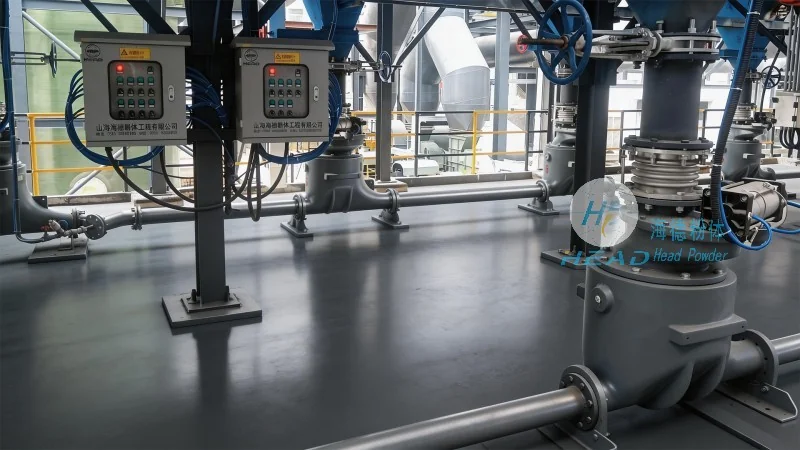
- Material Loading: The auxiliary material is loaded into the feeder hopper. The feeder then dispenses the material at a controlled rate into the conveying pipeline.
- Air Intake: The air supply unit generates the required air pressure or vacuum. In a positive pressure system, the air is introduced at the inlet of the pipeline, while in a negative pressure system, the vacuum is applied at the outlet.
- Material Suspension: The air flow creates a fluidized mixture of material and air, suspending the particles in the air stream. The material is then transported through the pipeline to the destination.
- Transport and Delivery: The material travels through the pipeline to the receiving hopper or silo. The system maintains consistent flow rates and pressure to ensure smooth delivery.
- Separation and Collection: At the end of the pipeline, a separator or cyclone separates the material from the air. The separated material is collected in the receiving hopper, while the air is filtered and discharged or recirculated.
- System Monitoring: The control system continuously monitors the pressure, flow, and level in the system. Any deviations are detected and corrected to maintain optimal operation.
Advantages of Pneumatic Conveying Systems
Pneumatic conveying systems offer several advantages over traditional material handling methods, making them a preferred choice for cement plants:
- Efficiency and Speed: The system can transport materials at high speeds, reducing overall production time and increasing throughput.
- Low Maintenance: With fewer moving parts compared to mechanical conveyors, pneumatic systems require less maintenance and have lower downtime.
- Hygienic and Clean: The enclosed pipeline design prevents dust pollution and contamination, ensuring the material remains clean and free from moisture.
- Customizable Solutions: HeadPowder provides customized systems tailored to the specific requirements of each cement plant, ensuring optimal performance and cost-effectiveness.
- Energy Efficiency: Modern pneumatic systems are designed to be energy-efficient, reducing operational costs and environmental impact.
Conclusion
HeadPowder's pneumatic conveying systems for cement auxiliary materials are designed to deliver reliable, efficient, and cost-effective material handling solutions. By understanding the operation process and working principle of these systems, cement plants can enhance their production processes, improve material quality, and reduce operational costs. With a focus on innovation and customer satisfaction, HeadPowder continues to lead the industry in providing advanced engineering solutions for the cement sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China
