HeadPowder, a prominent engineering firm headquartered in Shandong, China, specializes in the development and implementation of advanced material handling systems. One of their flagship products is the bin pump material pneumatic conveying system, which has become a critical component in various industrial sectors for efficient bulk material transport. This system integrates the functionality of a bin pump with pneumatic conveying technology, enabling reliable and flexible movement of materials across different locations and processes.
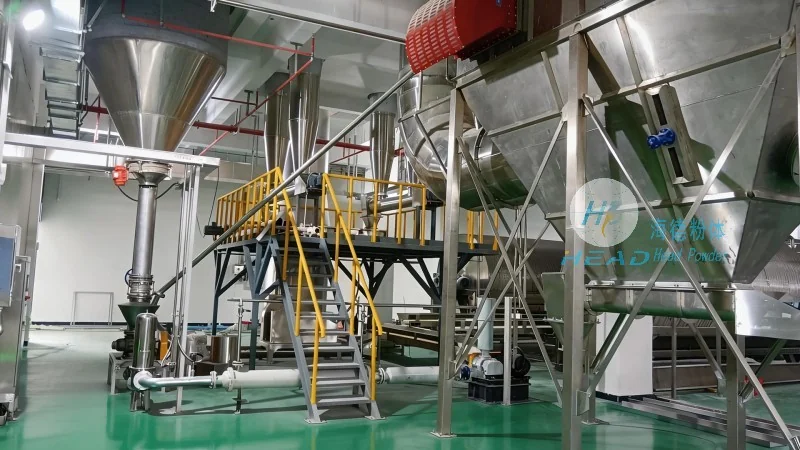
The bin pump material pneumatic conveying system operates by first loading bulk materials into a storage bin or hopper. The system then utilizes a bin pump to create a pressure differential, which draws the material into the conveying line. The material is transported through the pipeline using a combination of air pressure and vacuum, depending on the specific application requirements. This method allows for the movement of materials over long distances and in various orientations, making it suitable for diverse industrial processes such as chemical, food, and pharmaceutical industries.
Key components of the bin pump material pneumatic conveying system include the storage bin, bin pump, conveying pipeline, and control system. The storage bin is designed to hold the bulk material and provide a consistent feed to the bin pump. The bin pump, typically a positive displacement pump, generates the necessary pressure to move the material through the pipeline. The conveying pipeline is made of durable materials such as stainless steel or plastic, ensuring resistance to corrosion and wear from the conveyed material. The control system monitors and regulates the operation of the bin pump and other components, ensuring safe and efficient material transfer by continuously tracking pressure, flow rate, and other critical parameters.
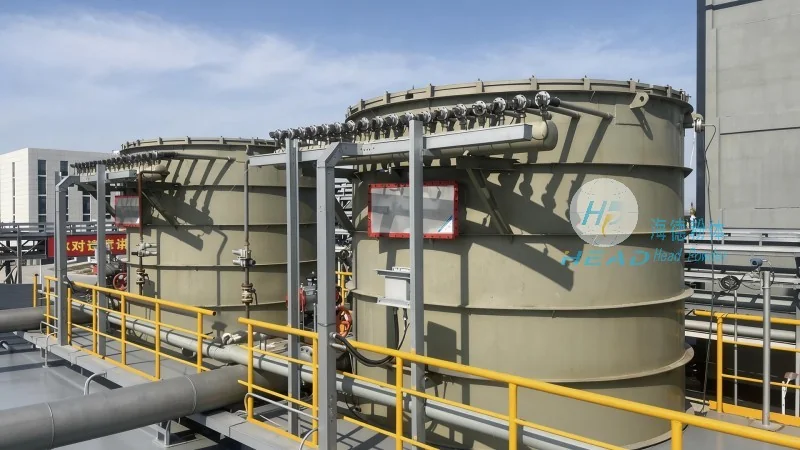
During the operation process, the bin pump material pneumatic conveying system follows a sequence of steps. First, the bulk material is fed into the storage bin from a hopper or silo. The bin pump then starts to operate, creating a vacuum or pressure inside the bin, which draws the material into the pump chamber. The pump then discharges the material into the conveying pipeline under pressure. The material travels through the pipeline to the destination point, where it is discharged into a receiving hopper or silo. The control system continuously monitors the pressure, flow rate, and other parameters to maintain optimal operation and prevent any issues such as blockages or overloading, ensuring that the system runs smoothly and efficiently.
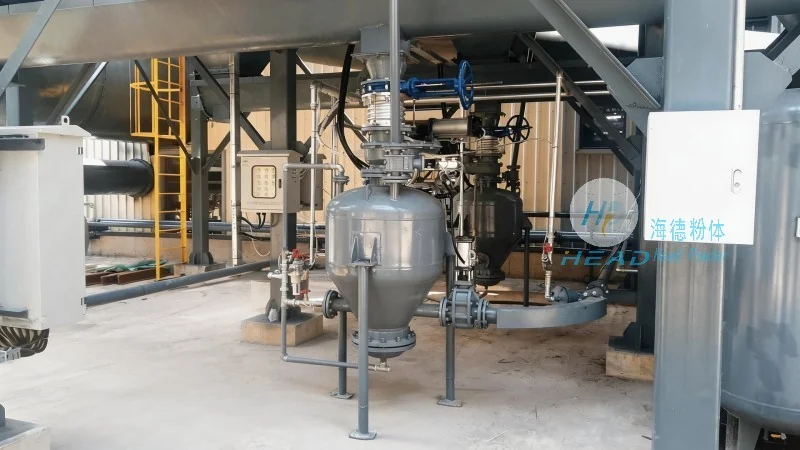
The working principle of the bin pump material pneumatic conveying system is based on the principles of fluid dynamics and material handling. The system utilizes the air as the conveying medium, which is either supplied under pressure or created by a vacuum. The bin pump acts as the primary driver, providing the necessary force to move the material through the pipeline. The material is suspended in the air stream and transported along the pipeline, similar to how a fluid is conveyed. This method is particularly effective for materials that are difficult to handle by other means, such as fine powders, granules, and fine particles, as it allows for uniform and consistent transport without the need for mechanical components that might cause wear or contamination.
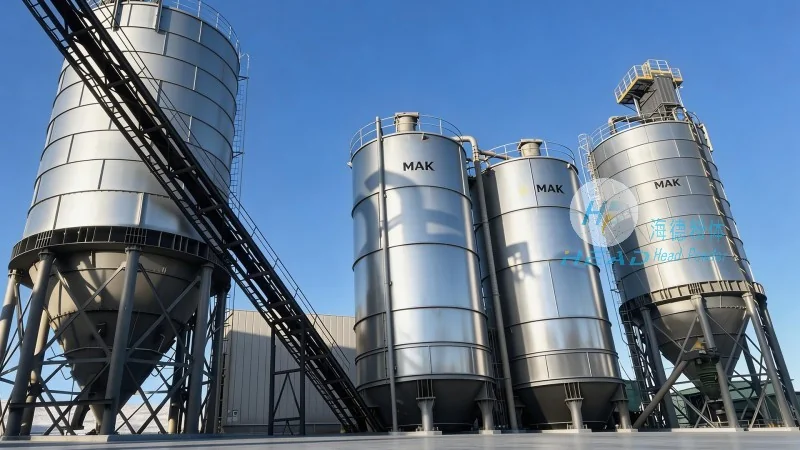
Advantages of the bin pump material pneumatic conveying system include high efficiency, flexibility, and reliability. The system can transport materials over long distances and in various configurations, making it suitable for complex industrial layouts where traditional conveyor systems may not be feasible. It also offers the ability to handle a wide range of materials, from fine powders to bulk granules, without the need for additional equipment such as crushers or screens. The system is also relatively easy to install and maintain, with minimal downtime required for routine maintenance, which helps in reducing operational costs and increasing overall productivity for the end-user.
HeadPowder's expertise in designing and manufacturing bin pump material pneumatic conveying systems ensures that clients receive customized solutions tailored to their specific needs. The company's engineers work closely with clients to understand their material handling requirements and design a system that meets their operational and performance goals. With a focus on quality and innovation, HeadPowder provides reliable and efficient material handling solutions that enhance productivity and reduce operational costs for their clients. By leveraging advanced technology and rigorous testing, HeadPowder ensures that each system is built to withstand the demands of industrial environments and delivers consistent performance over its service life.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top