HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems for cement raw materials. These systems are critical in modern cement production, ensuring efficient and reliable material transport from storage to processing units. This article delves into the operation process and working principles of such systems, highlighting their key components, operational dynamics, and the technological advancements that enhance performance.
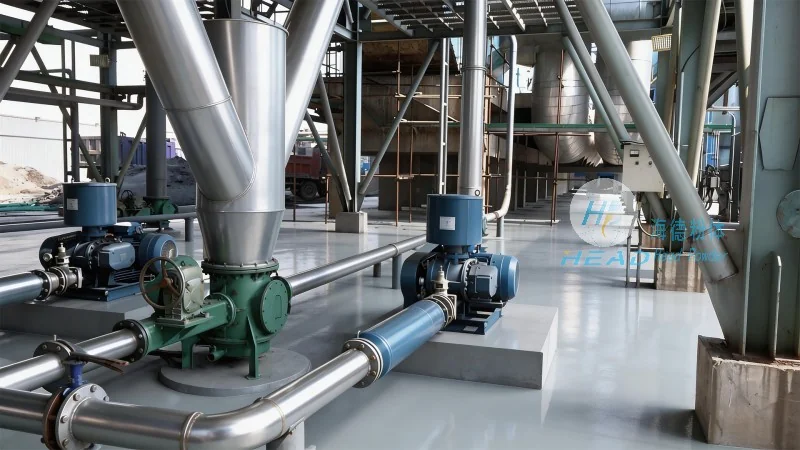
The cement raw material powder pneumatic conveying system consists of several integral components that work in tandem to achieve seamless material transport. The primary components include a material hopper or silo, a feeder (often a rotary valve or screw feeder), a conveying pipeline, a blower or air compressor, and a receiver or discharge hopper. Each component plays a vital role in the overall system's functionality.
1. **Material Hopper/Silo**: This is the storage vessel where raw materials like limestone, clay, and iron ore are stored before being conveyed. The hopper is designed with a conical bottom to facilitate material flow and prevent blockages. 2. **Feeder**: The feeder regulates the flow of material from the hopper into the conveying pipeline. A rotary valve or screw feeder is commonly used to control the feed rate, ensuring a consistent and controlled supply of material. 3. **Conveying Pipeline**: The pipeline, typically made of stainless steel or other corrosion-resistant materials, transports the material through the system. The pipeline is equipped with bends, elbows, and straight sections to guide the material to the processing unit. 4. **Blower/Air Compressor**: This component generates the necessary air pressure to move the material particles through the pipeline. The blower can be either positive displacement or centrifugal, depending on the system's requirements. 5. **Receiver/Discharge Hopper**: The final component where the conveyed material is deposited. This hopper is connected to the processing equipment, such as a raw mill, where the material is further processed into cement clinker.
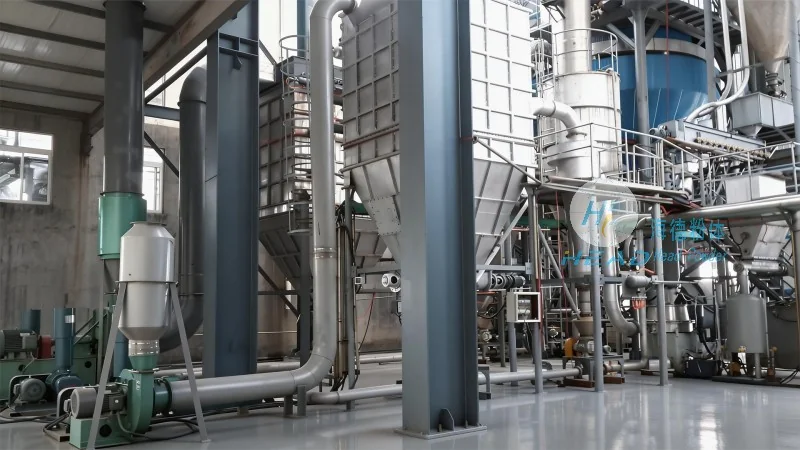
The operation of the cement raw material powder pneumatic conveying system is based on the principle of pneumatic transport, where material particles are suspended and transported by a stream of air. The process begins with the material being discharged from the hopper into the feeder. The feeder then controls the flow rate, ensuring a steady supply of material into the pipeline. Simultaneously, the blower generates a high-pressure air stream that enters the pipeline at the inlet of the feeder.
As the material enters the pipeline, it is entrained by the air stream and becomes suspended in the air. The air velocity within the pipeline must be sufficient to keep the material particles in suspension, preventing them from settling or clogging the pipeline. The conveying pipeline is designed with appropriate dimensions and bends to maintain the required air velocity and pressure. The material travels through the pipeline to the receiver, where the air is separated from the material and discharged through a filter or cyclone. The separated material is then collected in the receiver hopper, ready for further processing.
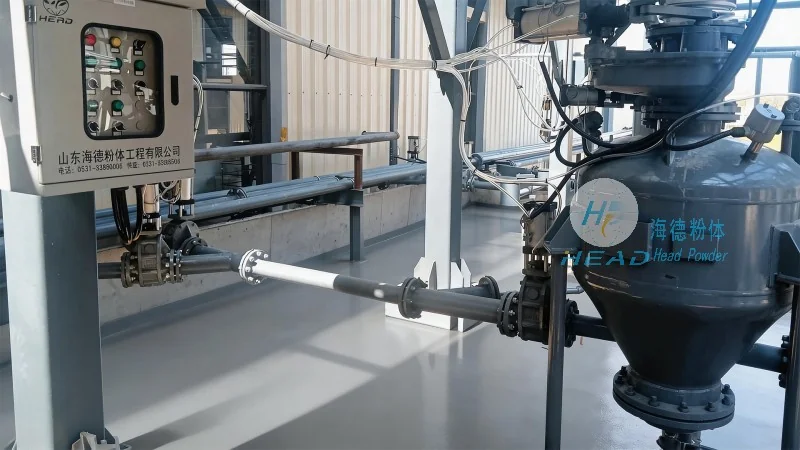
The operation process of the cement raw material powder pneumatic conveying system involves several sequential steps that ensure efficient material transport. The process starts with the preparation of the raw materials in the hopper, followed by the activation of the feeder to control the material flow. The blower is then started, generating the air pressure required for conveying. As the material is fed into the pipeline, it is transported to the receiver, where it is collected. The system operates continuously, with the feeder and blower maintaining a consistent flow rate to meet the processing demands.
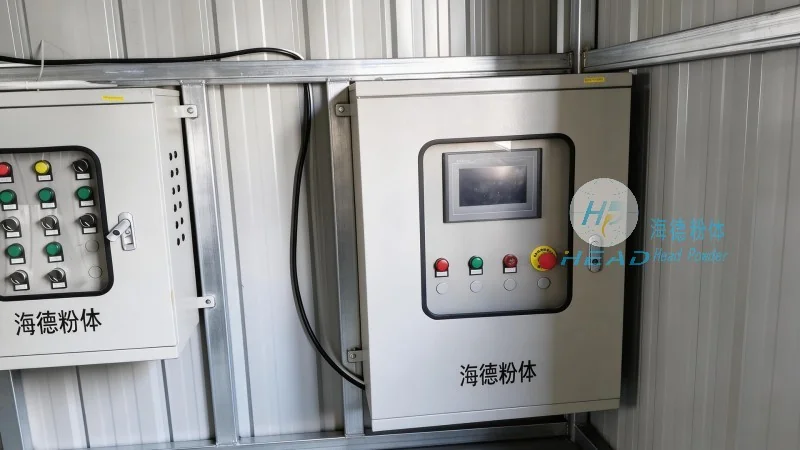
During operation, the system's performance is monitored through various sensors and controls. Pressure sensors in the pipeline monitor the air pressure, while flow meters track the material flow rate. These sensors provide real-time data to the control system, which adjusts the feeder speed or blower pressure as needed to maintain optimal operation. The system is designed to handle different types of raw materials, with adjustments made to the feeder and blower settings to accommodate variations in material properties, such as particle size and density.
Pneumatic conveying systems offer several advantages over traditional mechanical conveying methods for cement raw materials. These advantages include: 1. **Efficiency and Reliability**: The system provides a continuous and reliable flow of material, reducing downtime and improving production efficiency. 2. **Low Maintenance**: Compared to mechanical systems, pneumatic systems have fewer moving parts, resulting in lower maintenance costs and longer service life. 3. **Versatility**: The system can handle a wide range of raw materials, including powders and granules, with minimal adjustments. 4. **Cleanliness and Hygiene**: The enclosed pipeline design prevents dust and contamination, maintaining a clean and safe working environment. 5. **Energy Efficiency**: Modern pneumatic systems are designed to be energy-efficient, with optimized air flow and pressure control reducing energy consumption.
HeadPowder's cement raw material powder pneumatic conveying systems are engineered to meet the demanding requirements of modern cement production. By understanding the operation process and working principles of these systems, manufacturers can optimize their material transport processes, improve efficiency, and reduce operational costs. With a strong presence in Shandong, China, HeadPowder continues to lead in the development of advanced pneumatic conveying solutions, ensuring reliable and efficient material handling for cement production facilities worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top