HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems. Among their core offerings is the negative pressure dilute phase powder conveying system, a technology that efficiently transports fine powders and granular materials through a network of pipes using a vacuum or negative pressure environment. This method is widely recognized for its ability to handle delicate materials with minimal product degradation, making it suitable for various industrial applications such as pharmaceuticals, food processing, and chemical manufacturing.
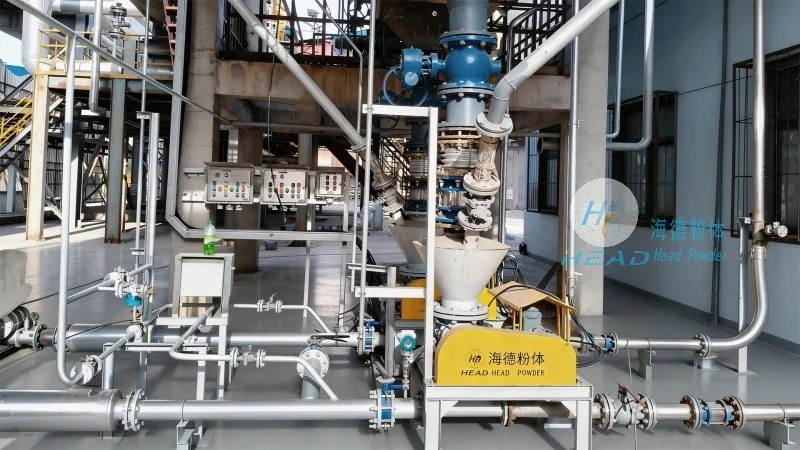
As a prominent player in the powder handling industry, Shandong HeadPowder Engineering Co., Ltd. (commonly known as HeadPowder) has established itself as a trusted partner for businesses seeking reliable and efficient material transport solutions. With a strong commitment to innovation and customer satisfaction, the company leverages years of expertise to develop customized pneumatic conveying systems tailored to the unique needs of each client. HeadPowder's headquarters and primary operations are located in Shandong, China, where the company maintains a state-of-the-art facility dedicated to research, development, and production of advanced powder handling equipment.
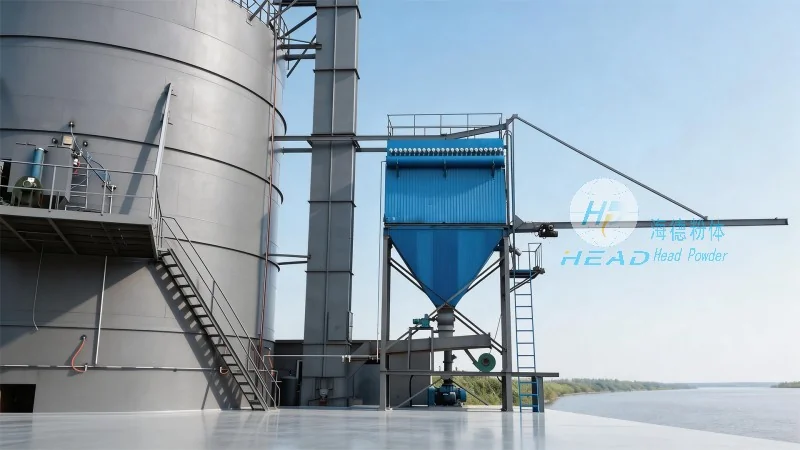
The negative pressure dilute phase powder pneumatic conveying system consists of several critical components that work in concert to ensure smooth and efficient material transport. The primary elements include a vacuum pump or fan that generates the negative pressure required to draw material from the source, a hopper or feeder that stores and meters the powder, a pipeline network that transports the material, and a receiver or discharge unit where the material is deposited. Each component is carefully designed and integrated to optimize performance, minimize energy consumption, and ensure the safe handling of the conveyed material.
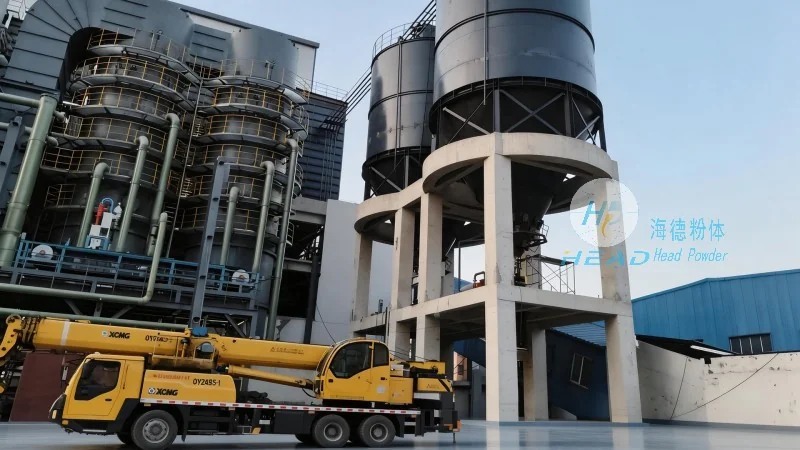
The operation of a negative pressure dilute phase powder conveying system follows a systematic sequence of steps to ensure consistent and reliable material transport. The process begins with the loading of the powder into the hopper or feeder, where the material is stored and prepared for transport. The vacuum pump then activates, creating a negative pressure within the pipeline system. This pressure differential draws the powder from the hopper, where it is entrained by the air flow and carried through the pipeline to the receiver. The material is then discharged from the receiver, completing the transport cycle. The system operates continuously, with the vacuum pump maintaining the necessary pressure to sustain the flow of material. This continuous operation allows for efficient and uninterrupted material handling, reducing downtime and increasing overall productivity.
The working principle of the negative pressure dilute phase powder pneumatic conveying system is based on the fundamental principles of fluid dynamics and particle transport. The system relies on the creation of a negative pressure environment within the pipeline, which is achieved by the operation of a vacuum pump. This negative pressure creates a pressure differential between the source (hopper) and the receiver, causing the powder to be drawn into the pipeline. The powder particles are then entrained by the air flow, forming a dilute phase mixture that is transported through the system. The key to the system's efficiency lies in maintaining the correct air-to-powder ratio, which ensures that the material is transported without excessive pressure drop or particle degradation. The system's design allows for precise control of the air flow and pressure, enabling operators to adjust the conveying rate and ensure optimal performance under varying conditions.
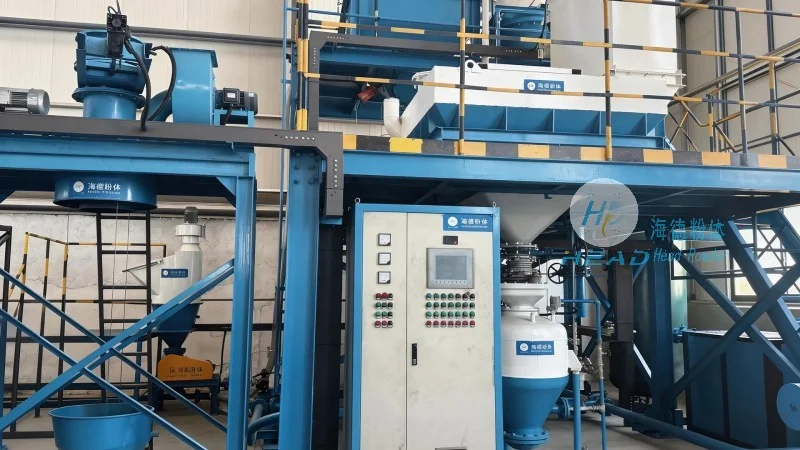
The negative pressure dilute phase powder conveying system offers several advantages that make it a preferred choice for many industrial applications. One of the primary benefits is its ability to handle delicate and sensitive materials without causing damage or degradation. The low pressure environment and gentle handling minimize the risk of particle breakage, caking, or contamination, which is crucial for industries such as pharmaceuticals and food processing where product quality is paramount. Additionally, the system is highly flexible and can be customized to accommodate a wide range of materials, including powders, granules, and fine particles. It is also energy-efficient compared to other conveying methods, as the vacuum pump operates at lower pressures and consumes less energy. The system is widely used in various industries, including chemical manufacturing, where it is used to transport raw materials and finished products; in pharmaceuticals, where it is used to handle active pharmaceutical ingredients (APIs) and excipients; and in food processing, where it is used to transport ingredients and finished food products.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top