Feather material conveying equipment is a specialized device designed to handle and transport feather materials efficiently and safely. As a key component in the processing industry, this equipment plays a crucial role in improving production efficiency and ensuring the quality of feather-based products. Understanding its operation process and working principle is essential for operators and engineers to maintain optimal performance and troubleshoot issues effectively.
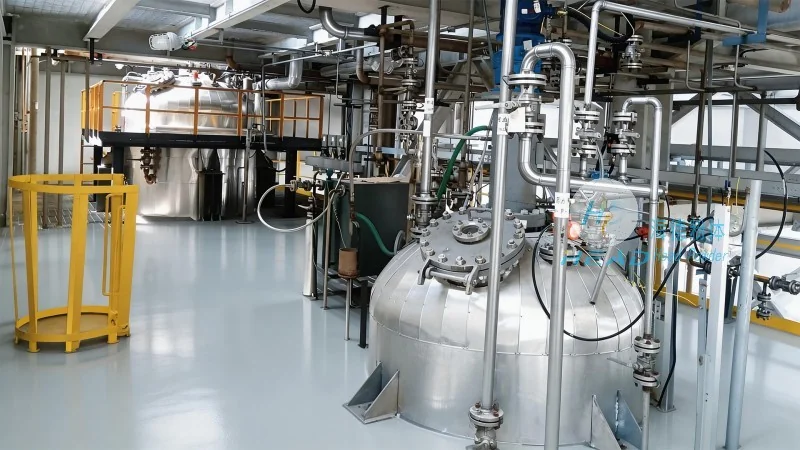
Feather material conveying equipment, commonly used in the poultry processing and feather processing industries, is engineered to handle delicate and lightweight feather materials. The equipment is typically composed of several key components, including feeders, conveyors, and control systems. These components work in harmony to ensure the smooth flow of feather materials from the input point to the output point. The design of such equipment is tailored to minimize damage to the feathers while maximizing throughput, making it an indispensable tool in modern feather processing operations. For instance, the feeder is designed with adjustable gates to control the flow rate, preventing overloading of the conveyor. The conveyor itself may feature a gentle slope or a series of rollers to reduce friction and prevent feather breakage. Control systems, equipped with real-time monitoring capabilities, provide operators with immediate feedback on the system's status, allowing for quick adjustments to maintain optimal performance.
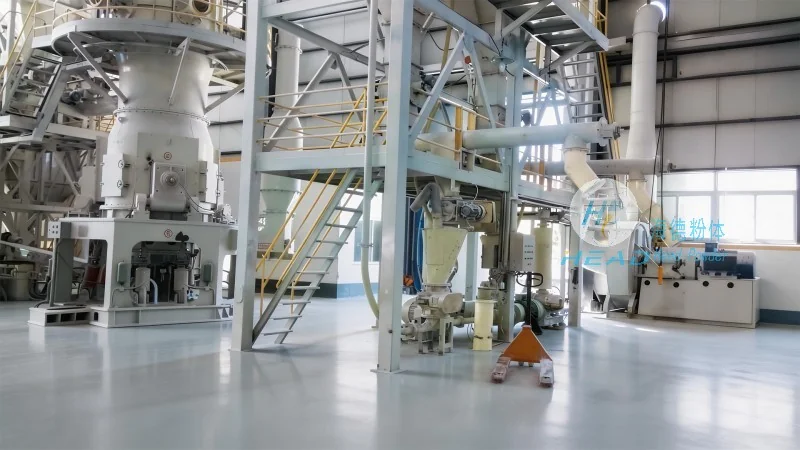
The performance of feather material conveying equipment relies on the proper functioning of its core components. Each part plays a specific role in the overall operation. The feeder is responsible for uniformly distributing the feather material into the conveyor system, preventing blockages and ensuring consistent material flow. It often includes mechanisms such as vibrating plates or rotary valves that help separate clumped feathers and maintain a steady feed. The conveyor, which can be a belt conveyor, screw conveyor, or pneumatic conveyor, transports the feathers through the system. Belt conveyors are particularly common due to their ability to handle delicate materials without causing damage. Screw conveyors are used for vertical or inclined transport, while pneumatic conveyors use air pressure to move feathers, which is ideal for handling fine or dusty materials. Control systems, including sensors and motors, monitor and regulate the speed and direction of the conveyor, adapting to changes in material volume and maintaining operational stability. For example, a load cell sensor can detect the weight of feathers on the conveyor and adjust the motor speed to prevent overloading. This feedback loop ensures that the equipment operates efficiently and safely under varying conditions.
The operation process of feather material conveying equipment involves several sequential steps that ensure the efficient handling of feather materials. The process typically begins with the feeding of raw feather materials into the feeder. The feeder then distributes the material evenly onto the conveyor belt or mechanism. As the conveyor moves, the feathers are transported to the next stage of processing. At this stage, the equipment may include additional components such as classifiers or separators that further process the feathers based on size or quality. For example, a classifier might use a series of screens to separate feathers into different grades, allowing for higher-quality products. The final output is then collected from the discharge point, completing the conveying process. Throughout this process, the equipment operates under controlled conditions, with regular monitoring to ensure that the feathers are handled gently and without damage. Operators may use visual inspections or automated cameras to check for any signs of feather breakage or blockages, ensuring that the process is running smoothly.
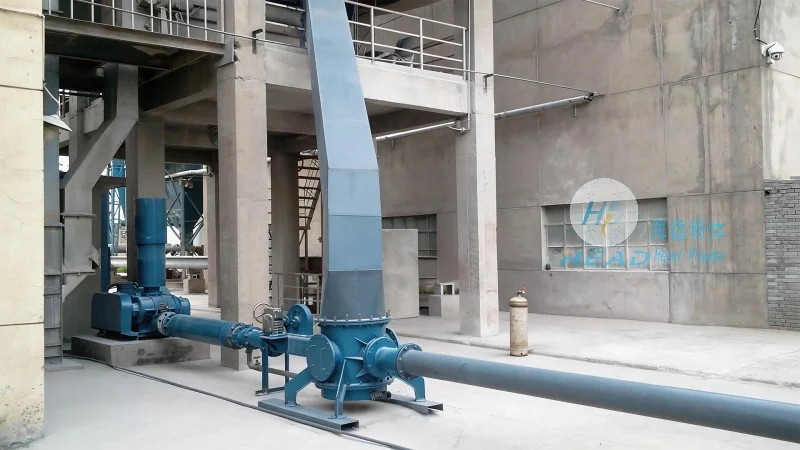
The working principle of feather material conveying equipment is based on mechanical motion and controlled material flow. The equipment utilizes a combination of gravity, friction, and motor-driven mechanisms to move the feathers. The conveyor system, powered by an electric motor, rotates the driving components, which in turn move the conveyor belt or other conveying elements. Sensors are integrated into the system to detect the presence and quantity of feathers, allowing the control system to adjust the conveyor speed accordingly. This dynamic adjustment ensures that the equipment can handle varying loads without overloading or underutilizing its capacity. The overall principle is to create a continuous and controlled flow of feather materials, minimizing downtime and maximizing productivity. For instance, a variable frequency drive (VFD) can adjust the motor speed based on the detected load, ensuring that the conveyor runs at the optimal speed for the current material volume. This technology not only improves efficiency but also reduces energy consumption, making the equipment more cost-effective to operate.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top