The flocculant dry powder material handling system is a critical component in various industrial applications, particularly in water treatment and chemical processing. This system is designed to efficiently transport dry powders, such as flocculants, which are essential for processes like sedimentation and clarification. The system's design ensures reliable and consistent material transport, minimizing downtime and enhancing overall operational efficiency. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in developing and manufacturing such systems, catering to the diverse needs of industrial clients.
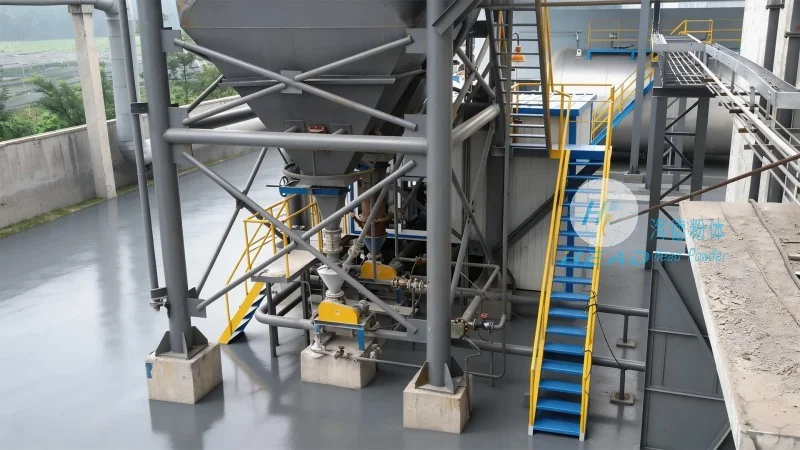
The flocculant dry powder material handling system comprises several key components that work in tandem to ensure smooth operation. These include a hopper for material storage, a feeder to control the flow rate, a conveyor system for transporting the powder, and a control panel for monitoring and adjusting the process. Each component is engineered to handle the specific characteristics of flocculant powders, such as their fine particle size and potential for caking. The hopper is typically made of corrosion-resistant materials to prevent material degradation, while the feeder ensures a uniform and controlled discharge of the powder. The conveyor system may utilize screw conveyors or pneumatic transport lines, depending on the application requirements. The control panel integrates sensors and automation features to maintain optimal operating conditions, such as pressure, flow rate, and temperature.
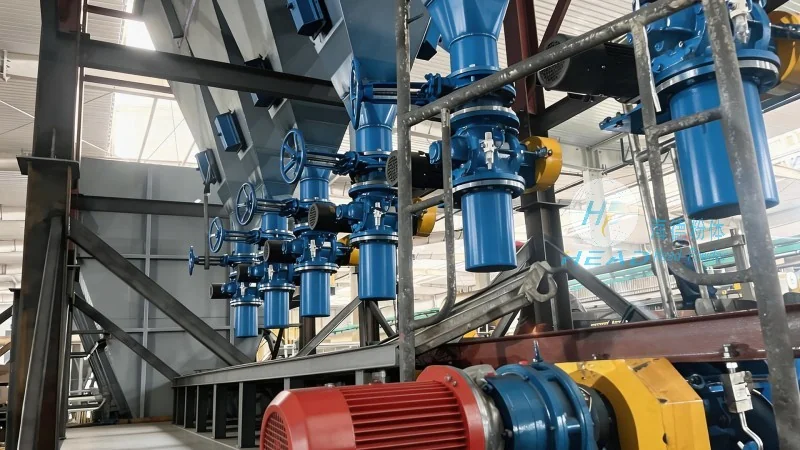
The operation of the flocculant dry powder material handling system follows a systematic process to ensure efficient material transport. The process begins with the loading of flocculant powder into the hopper. The feeder then regulates the flow of powder from the hopper to the conveyor system. The conveyor transports the powder to the destination, such as a storage tank or a processing unit. Throughout the process, the control panel continuously monitors the system's performance, adjusting parameters as needed to maintain consistent flow and prevent blockages. The system is designed to operate with minimal human intervention, thanks to its automated control features. This automation not only enhances efficiency but also reduces the risk of operational errors. The entire process is optimized to handle varying powder loads and flow rates, ensuring reliable performance under different operational conditions.
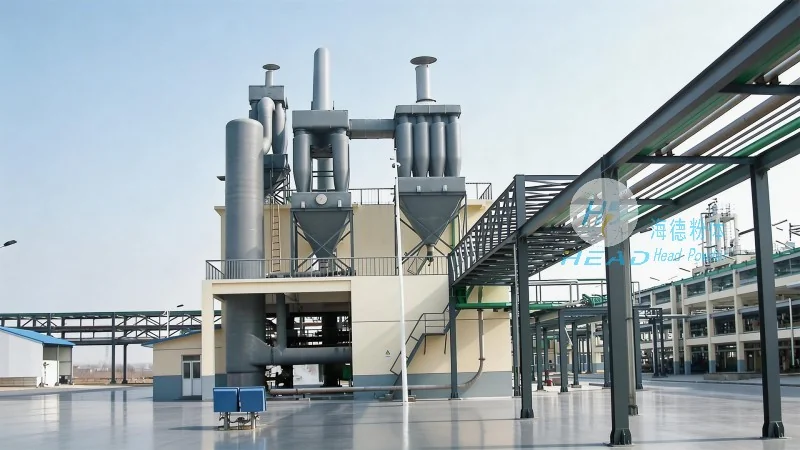
The working principle of the flocculant dry powder material handling system is based on mechanical and pneumatic mechanisms to transport dry powders. The system utilizes a combination of gravity and mechanical force to move the powder from the hopper to the conveyor. The feeder, often a rotary or vibratory type, controls the discharge rate by adjusting the speed or vibration frequency. The conveyor system, such as a screw conveyor, uses rotating blades to push the powder forward. For applications requiring longer distances or more complex routes, pneumatic transport systems may be employed, where the powder is carried by a stream of air. The control panel plays a crucial role in regulating the system's operation by monitoring sensors that detect pressure, flow, and level. These sensors provide real-time data to the control system, which adjusts the feeder speed or conveyor speed accordingly. The system's design also incorporates safety features, such as pressure relief valves and emergency stop buttons, to prevent accidents and ensure safe operation. By integrating these components and mechanisms, the system achieves efficient and reliable transport of flocculant powders, meeting the demands of industrial applications.
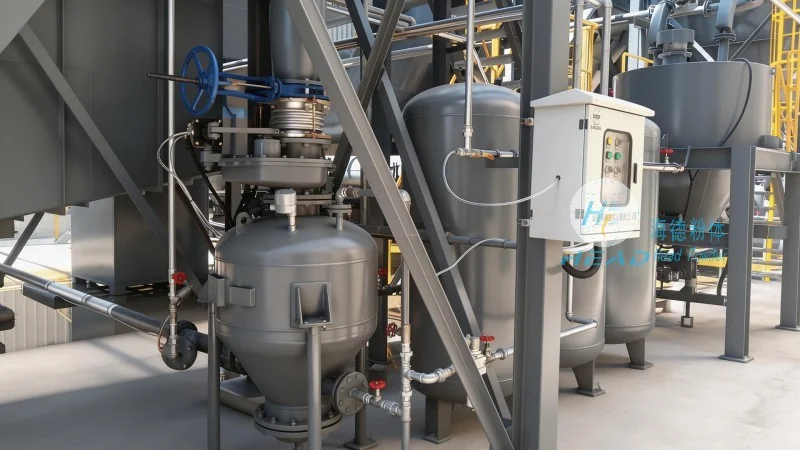
The flocculant dry powder material handling system offers several benefits that make it an essential solution for industrial processes. One of the primary benefits is its ability to handle fine and cohesive powders like flocculants without clogging or degradation. The system's design minimizes material loss and ensures consistent quality of the transported powder. Another benefit is its high efficiency, which reduces operational costs by minimizing downtime and maximizing throughput. The system is also versatile, suitable for various applications including water treatment plants, chemical manufacturing facilities, and mining operations. In water treatment, the system ensures a steady supply of flocculant to the clarifiers, improving the efficiency of sedimentation and clarification processes. In chemical manufacturing, it facilitates the transport of raw materials to processing units, enhancing production line efficiency. The system's reliability and durability also contribute to its widespread adoption in industries where consistent performance is critical.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top