Multi-hopper pneumatic conveying systems are advanced industrial equipment designed for efficient and reliable powder handling. These systems are widely used in various industries such as food, pharmaceuticals, chemicals, and minerals, where the transportation of bulk powders requires precision and control. The core of such a system is the multi-hopper pump, which enables the sequential or simultaneous feeding of different powder materials through a network of pipelines and air compressors.
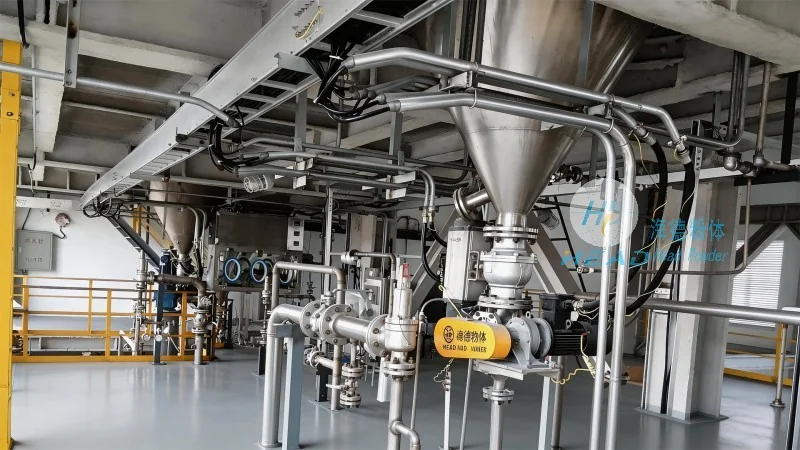
Before delving into the operation process, it's essential to understand the main components of a multi-hopper powder conveying line. The system typically consists of several key parts: multiple hoppers for storing different powder types, a series of air compressors or vacuum pumps to generate the necessary pressure or suction, a network of stainless steel or plastic pipelines for transporting the powders, and control panels for monitoring and regulating the system's performance. Each hopper is equipped with a feeding valve and a pressure sensor to ensure accurate material discharge. The pipelines are often equipped with check valves, filters, and flow meters to maintain system integrity and prevent material blockages.
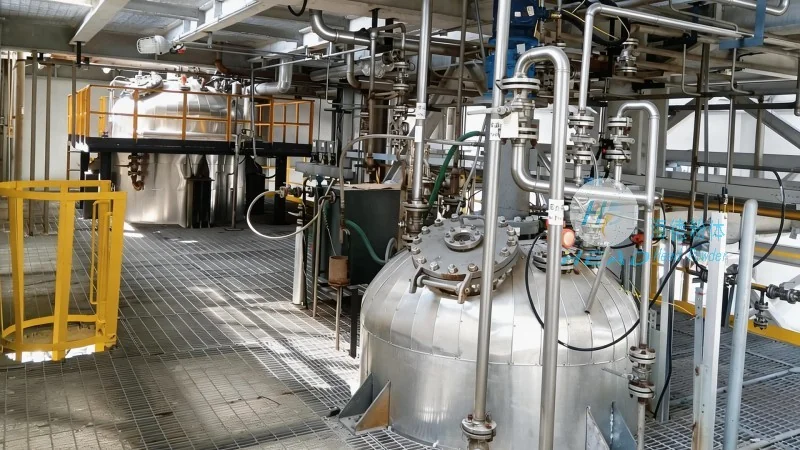
The working principle of a multi-hopper powder conveying system is based on the principles of pneumatic transport. When the system operates, air is compressed or drawn into the pipelines, creating a flow that moves the powder particles along with it. The multi-hopper design allows for the simultaneous or sequential discharge of different powders from separate hoppers into a common or separate pipeline. The system can operate under pressure (positive pressure) or suction (negative pressure), depending on the application requirements. In positive pressure systems, compressed air pushes the powder through the pipeline, while in negative pressure systems, vacuum pulls the powder from the hoppers. The control system adjusts the air pressure and flow rate to maintain a consistent conveying velocity, ensuring that the powder is transported without degradation or segregation.
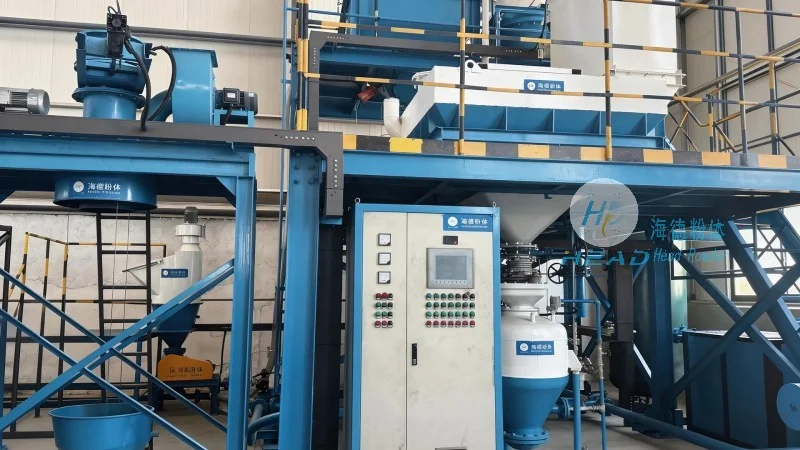
The operation process of a multi-hopper powder conveying line involves several sequential steps, each carefully controlled to ensure optimal performance. The process typically begins with the loading of powders into each hopper. Once the hoppers are filled, the control panel initiates the conveying cycle. First, the system checks the pressure and flow parameters to ensure they are within the safe operating range. Then, the feeding valve of the first hopper opens, and the powder is discharged into the pipeline under the influence of compressed air. The powder is carried by the air stream to the destination point, such as a silo, storage tank, or processing unit. After the first hopper's material is fully conveyed, the control system signals the next hopper to start its discharge, and the cycle repeats. The system continues to alternate between hoppers until all materials are transported to their respective destinations. The control panel monitors the entire process, adjusting the air pressure and flow rate as needed to maintain a stable conveying rate. In case of any anomalies, such as a blockage or pressure drop, the system automatically shuts down and alerts the operator, preventing material loss or equipment damage.
Multi-hopper powder conveying systems offer several advantages over traditional conveying methods. Firstly, they provide high efficiency and reliability, as the system can handle multiple powder types simultaneously without cross-contamination. The stainless steel construction ensures hygiene and compliance with industry standards, making it suitable for food and pharmaceutical applications. The system also reduces labor costs and increases production throughput by automating the powder handling process. Additionally, the multi-hopper design allows for flexible material handling, enabling the system to adapt to changing production requirements. The applications of these systems are diverse, including the transportation of flour, sugar, cement, and other bulk powders in the food and construction industries. They are also used in the pharmaceutical industry for the handling of active pharmaceutical ingredients (APIs) and excipients, where precision and contamination control are critical.
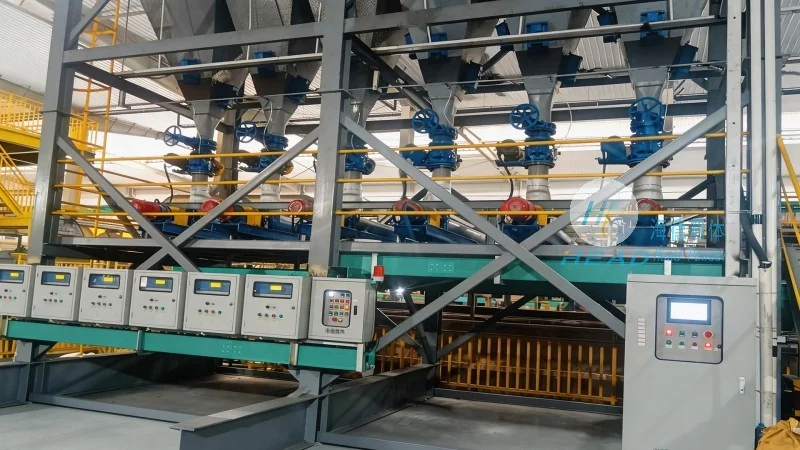
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of multi-hopper powder conveying systems and related industrial equipment. With a strong focus on innovation and quality, HeadPowder has established itself as a trusted partner in the powder handling industry. The company is headquartered in Shandong, China, and has a team of experienced engineers and technicians dedicated to developing advanced solutions for its clients. HeadPowder's products are designed to meet the specific needs of various industries, ensuring high performance, reliability, and durability. The company adheres to international standards and provides comprehensive after-sales support, including installation, maintenance, and technical assistance. By leveraging its expertise and commitment to excellence, HeadPowder continues to deliver cutting-edge solutions that enhance the efficiency and safety of powder handling operations worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top