For those in the material handling industry, understanding the operation process and working principle of advanced pneumatic conveying systems is crucial for optimizing material transport efficiency and reliability. Among these systems, capsule pneumatic conveyors stand out due to their unique design and capabilities. This article, provided by Shandong HeadPowder Engineering Co., Ltd. (headpowder), a leading manufacturer of material handling equipment, provides a detailed exploration of how capsule pneumatic conveying equipment operates, focusing on the technical aspects and practical applications that make it a preferred choice for various industries.
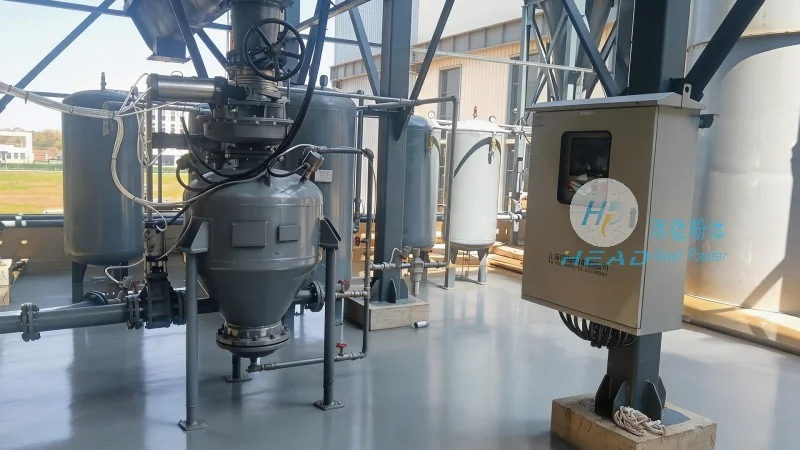
Capsule pneumatic conveyors, also known as rotary valve or rotary airlock pneumatic conveyors, are specialized equipment used for the transport of bulk materials in a closed system. These systems are widely used in industries such as pharmaceuticals, food processing, chemical manufacturing, and more, where maintaining product integrity, controlling dust, and ensuring a clean environment are paramount. The design of capsule conveyors incorporates a series of rotating capsules or valves that create airtight seals, allowing for the controlled movement of materials from a source to a destination without exposure to the external environment.
Before delving into the operation process, it is essential to understand the core components that make up a capsule pneumatic conveying system. These components work in tandem to ensure smooth and efficient material transport. The primary components include:
1. Feeder/Inlet Hopper: This component is responsible for receiving bulk materials from a storage silo or hopper. The inlet hopper is designed to feed material into the first capsule in the system, ensuring a consistent flow of material.
2. Capsule Rotating Valve: The heart of the capsule conveyor is the rotating valve, which consists of a series of airtight capsules or segments. As the valve rotates, each capsule sequentially opens and closes, allowing air to enter and push the material forward. The rotation speed and timing of the valve are critical for controlling the flow rate and preventing material blockages.
3. Pneumatic Pipeline: The material is conveyed through a network of pipelines under pressure. The pipeline is typically made of stainless steel or other corrosion-resistant materials to accommodate various material types and maintain hygiene standards, especially in industries like food and pharmaceuticals.
4. Receiver/Outlet Hopper: The material is discharged into a receiver hopper at the end of the conveying line. This hopper collects the material and can be connected to downstream processes or storage units.
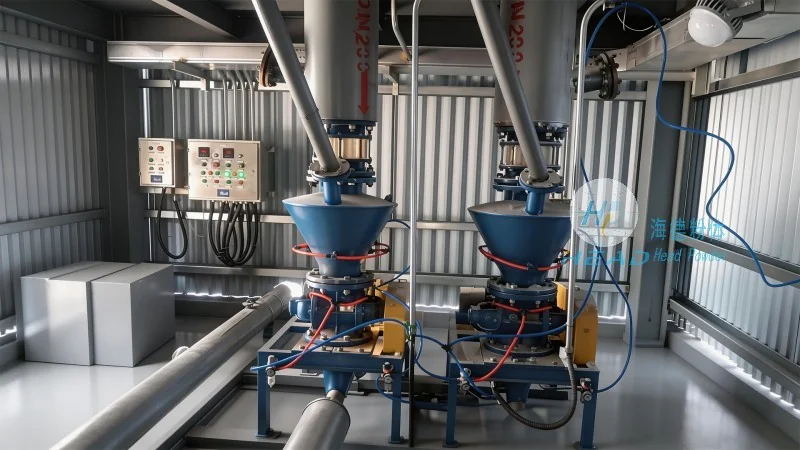
5. Compressor and Air Treatment System: A compressor provides the necessary air pressure to move the material through the pipeline. The air treatment system, including filters and dryers, ensures that the air used is clean and free of contaminants, preventing material contamination and maintaining system efficiency.
The working principle of capsule pneumatic conveying is based on the principle of air pressure and airtight sealing. The system operates by creating a pressure differential between the inlet and outlet of the pipeline. As the compressor supplies compressed air, it enters the pipeline and pushes the material forward. The rotating capsule valve controls the timing of air entry and material release, ensuring that each capsule is filled with material and then sealed to prevent backflow.
When a capsule is in the open position, it allows material to enter from the inlet hopper. Once the capsule rotates and seals, the compressed air from the pipeline enters the capsule, pushing the material forward to the next capsule in the sequence. This sequential opening and closing of capsules creates a continuous flow of material through the system. The speed of the capsule rotation and the air pressure can be adjusted to control the flow rate, making the system versatile for different material types and conveying distances.
The operation process of a capsule pneumatic conveying system involves several sequential steps that ensure efficient material transport. Here is a step-by-step breakdown of the process:
1. Material Loading: Bulk materials are loaded into the inlet hopper from a storage silo or bulk container. The hopper is designed to maintain a consistent material level, preventing overfilling or underfilling that could affect the conveying process.
2. Initial Air Pressure Application: The compressor is activated, and compressed air is introduced into the pipeline. The air pressure is set according to the material characteristics and conveying distance to ensure sufficient force to move the material.
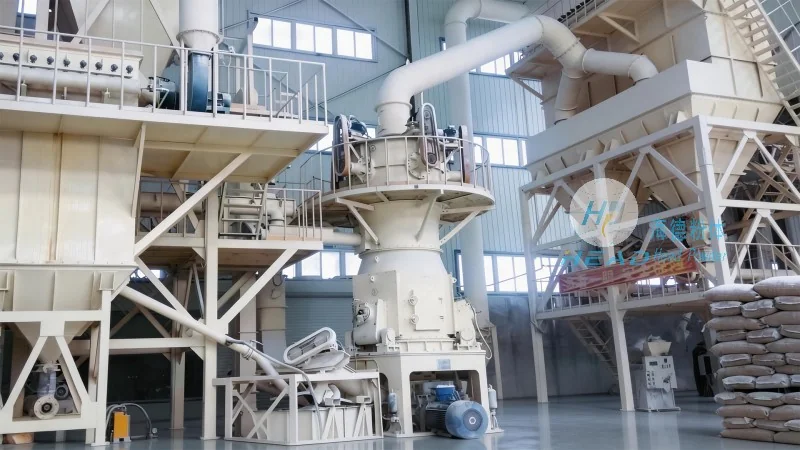
3. Capsule Valve Rotation: The rotating capsule valve begins to turn. As each capsule rotates to the open position, it allows material to enter from the inlet hopper. The valve then rotates to the closed position, sealing the material inside the capsule.
4. Material Conveying: With the capsule sealed, compressed air from the pipeline enters the capsule, pushing the material forward to the next capsule in the sequence. This process repeats as the capsule rotates, moving the material along the pipeline.
5. Material Discharge: At the end of the conveying line, the last capsule opens, allowing the material to be discharged into the receiver hopper. The receiver hopper then collects the material and can be connected to downstream processes or storage.
6. System Monitoring and Control: Modern capsule pneumatic conveying systems are equipped with control panels that monitor parameters such as air pressure, material flow rate, and valve rotation speed. These controls allow operators to adjust the system in real-time to maintain optimal performance and prevent issues like blockages or overpressure.
Capsule pneumatic conveying systems offer several advantages over traditional conveying methods. These benefits make them a preferred choice for industries that require high levels of product integrity and environmental control. Key advantages include:
1. Closed System Operation: The airtight design of the capsule valve prevents dust and material from escaping into the environment, maintaining a clean and safe working environment. This is particularly important in industries like food and pharmaceuticals where contamination control is critical.
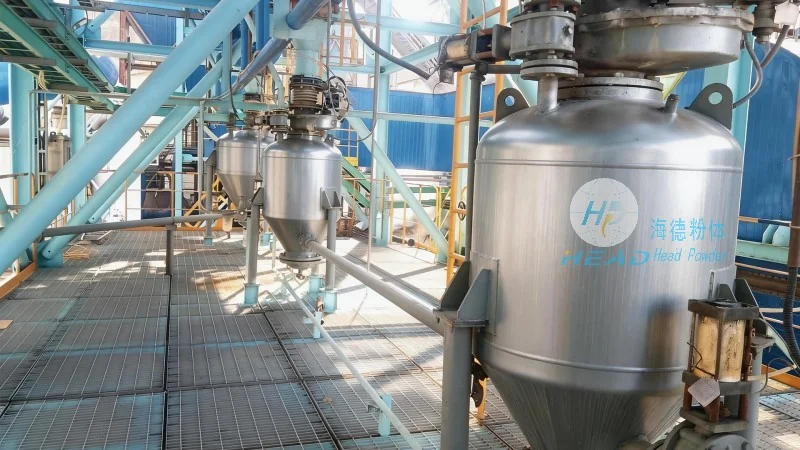
2. Hygienic and Clean Design: The stainless steel construction and smooth surfaces of the capsule conveyor make it easy to clean and maintain. This reduces the risk of cross-contamination and ensures compliance with industry regulations.
3. Versatility in Material Handling: Capsule conveyors can handle a wide range of materials, including powders, granules, and bulk solids. The system can be adjusted to accommodate different material densities, flow rates, and conveying distances.
4. Reduced Maintenance: The rotating valve design minimizes the need for frequent maintenance compared to other pneumatic conveying systems. The airtight seals and robust construction ensure long-term reliability and low maintenance costs.
5. Energy Efficiency: By optimizing air pressure and flow rates, capsule pneumatic conveying systems can be designed to operate efficiently, reducing energy consumption and operational costs.
The versatility of capsule pneumatic conveying equipment makes it suitable for a wide range of applications across various industries. Some common applications include:
1. Pharmaceutical Industry: In pharmaceutical manufacturing, capsule conveyors are used to transport raw materials and finished products, ensuring that the materials remain sterile and free from contamination. The closed system design and hygienic construction meet the stringent requirements of the pharmaceutical industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top