Desulfurization and denitrification are critical processes in modern industrial applications, particularly in power generation and chemical manufacturing. The efficient handling of desulfurization and denitrification agents is essential for maintaining optimal performance and environmental compliance. Pneumatic conveying equipment has emerged as a reliable solution for transporting these materials, offering advantages such as dust-free operation, low maintenance, and flexibility in system design. This article provides an in-depth look at the operation process and working principle of such equipment, highlighting its significance in industrial applications.
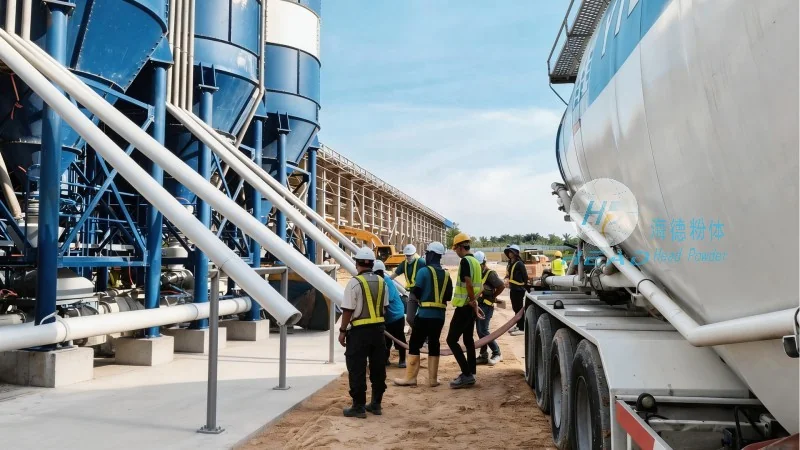
Pneumatic conveying systems are widely used in the transportation of desulfurization agents, which are typically powders or granules that require precise handling to prevent degradation or contamination. The equipment is designed to move these materials from storage silos or hoppers to processing units or reactors. The core components of a typical pneumatic conveying system include a hopper, a rotary valve, a conveyor line, a dust collector, and a control system. Each component plays a vital role in ensuring the smooth and efficient operation of the entire process.
The hopper serves as the storage container for the desulfurization agent, providing a consistent feed to the system. It is equipped with a level indicator to monitor the material inventory and a discharge valve to control the flow rate. The rotary valve, often referred to as a feeder, is responsible for regulating the material flow from the hopper into the conveyor line. It ensures a steady and controlled discharge of the powder, preventing blockages and maintaining system pressure. The conveyor line, which can be either a flexible hose or a rigid pipe, transports the material through the system. The choice of material for the conveyor line depends on the properties of the desulfurization agent, such as its abrasiveness and moisture content. A dust collector is integrated into the system to capture any airborne particles, ensuring a clean and safe working environment. The control system manages the operation of all components, including the rotary valve, conveyor speed, and dust collector, based on set parameters and feedback from sensors.
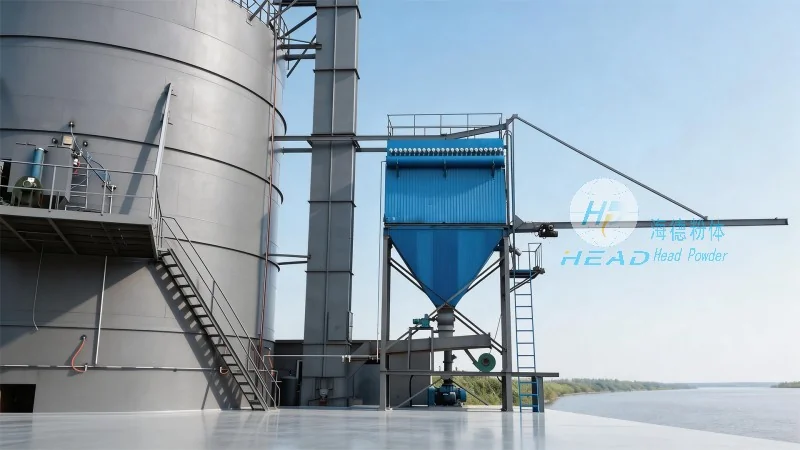
The operation of pneumatic conveying equipment for desulfurization agents involves several sequential steps. The process begins with the material being discharged from the hopper into the conveyor line through the rotary valve. Simultaneously, a vacuum or pressure is applied to the conveyor line, depending on the system design. In a vacuum system, the air is drawn through the conveyor line, pulling the material along with it. In a pressure system, compressed air is introduced into the line, pushing the material forward. The material travels through the line to the processing unit, where it is either mixed with other chemicals or directly introduced into the reactor. The control system continuously monitors the pressure, flow rate, and material level, making adjustments as needed to maintain optimal performance. The dust collector operates in parallel, capturing any particles that escape from the conveyor line and returning them to the hopper for reprocessing.
The working principle of the pneumatic conveying system is based on the interaction between the material and the air flow. In a vacuum system, the air flow creates a negative pressure that pulls the material particles into the conveyor line. The particles are carried by the air stream, maintaining a suspension that prevents clogging. The air velocity is critical; it must be high enough to keep the particles suspended but not so high as to cause excessive wear on the system components. In a pressure system, compressed air is used to push the material through the line. The air pressure is maintained at a level that ensures the material moves smoothly without causing excessive pressure drops or energy consumption. The system's efficiency depends on the balance between air flow and material flow, which is achieved through precise control of the rotary valve and conveyor speed.
Pneumatic conveying equipment offers several advantages over traditional methods like belt conveyors or bucket elevators. One of the primary benefits is the ability to handle materials in a dust-free environment, which is crucial for desulfurization agents that are sensitive to moisture or contamination. The system is also flexible, allowing for changes in material flow rate and direction without major modifications. Additionally, it requires less space compared to other conveying systems, making it suitable for compact industrial setups. The low maintenance requirements and long service life of the equipment further enhance its economic viability. These advantages make pneumatic conveying an ideal choice for industrial applications where efficiency, safety, and environmental compliance are paramount.
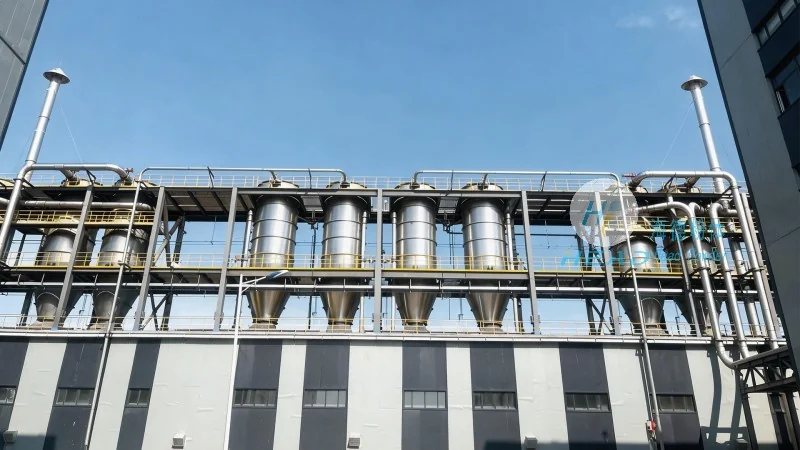
The pneumatic conveying equipment is specifically designed to support the desulfurization and denitrification processes, which are integral to reducing sulfur dioxide (SO2) and nitrogen oxides (NOx) emissions from industrial sources. In power plants, for example, desulfurization agents like limestone or lime are conveyed to the flue gas desulfurization (FGD) system. The equipment ensures that these agents are delivered to the reactor in the correct quantity and at the right time, optimizing the removal of sulfur compounds from the exhaust gases. Similarly, in chemical manufacturing, denitrification agents are transported to the denitrification reactors, where they facilitate the reduction of nitrogen oxides. The consistent and reliable operation of the pneumatic conveying system is essential for maintaining the efficiency of these processes and meeting environmental regulations.
Pneumatic conveying equipment for desulfurization and denitrification agents is a sophisticated and efficient solution for material handling in industrial applications. By understanding the operation process and working principle of such equipment, industries can optimize their processes, improve safety, and enhance environmental performance. The technology, supported by companies like Shandong HeadPowder Engineering Co., Ltd., continues to evolve, offering advanced solutions tailored to the specific needs of modern industrial operations. As environmental regulations become more stringent, the importance of efficient material handling systems like pneumatic conveyors will only grow, making them a critical component in sustainable industrial practices.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top