HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and implementation of advanced pneumatic conveying systems tailored for the handling of rare earth materials. These systems are engineered to efficiently transport fine powders and granules, ensuring minimal loss, high purity, and consistent flow rates essential for industrial applications.
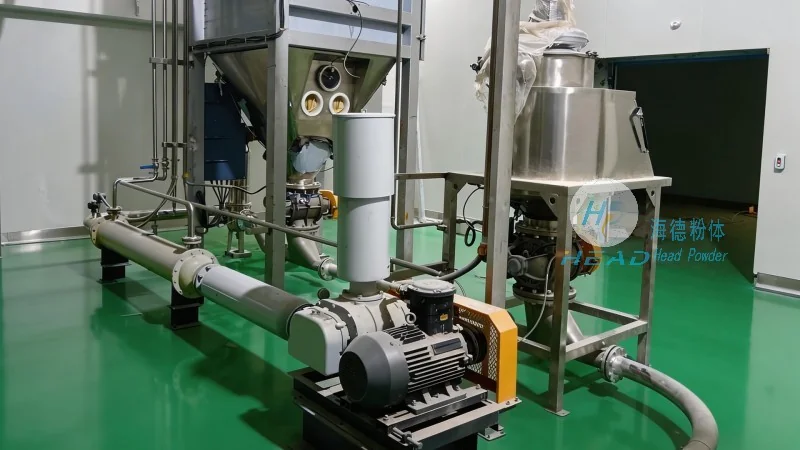
A typical rare earth pneumatic conveying system comprises several critical components that work in tandem to achieve reliable material transport. The main elements include a material feed hopper, a conveying line (often equipped with pressure vessels or vacuum pumps), a control valve system, and a discharge unit. The feed hopper is designed to store and meter the rare earth material, while the conveying line facilitates the movement of the material under pressure or vacuum. The control valve system regulates the flow and pressure, ensuring smooth operation and preventing blockages. The discharge unit then delivers the material to the target location, such as a storage silo or processing equipment.
The operation of a rare earth pneumatic conveying system follows a systematic process that ensures efficient and safe material handling. The process begins with the loading of the rare earth material into the feed hopper. The material is then metered and fed into the conveying line, where it is propelled by either compressed air (in pressure systems) or vacuum (in suction systems). The conveying line may include components like cyclones or filters to separate any entrained air or dust from the material. The material is then discharged at the receiving end, completing the transport cycle. This process is typically automated, with sensors and control systems monitoring pressure, flow rate, and material level to maintain optimal performance.
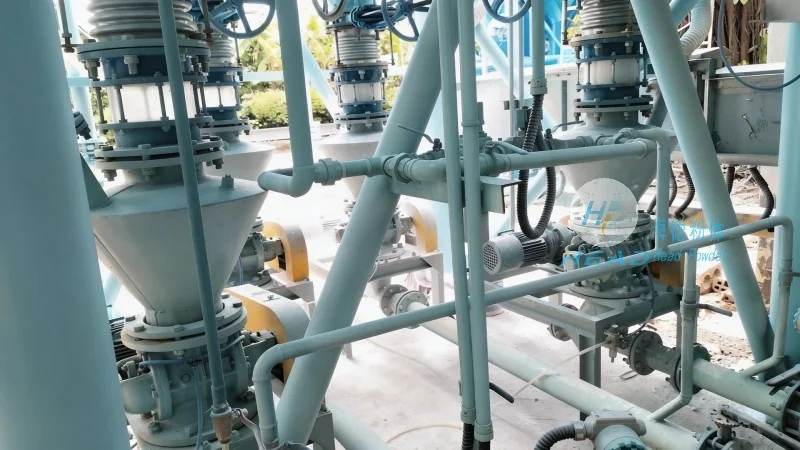
The working principle of rare earth pneumatic conveying systems is based on the fundamental physics of fluid dynamics and particle transport. In pressure systems, compressed air is introduced into the conveying line, creating a high-pressure environment that forces the rare earth material to move through the pipeline. The air and material mixture travels at high velocity, ensuring that the material is suspended and transported efficiently. In suction systems, a vacuum pump creates a low-pressure zone that draws the material from the feed hopper into the conveying line. The material is then carried by the air flow to the discharge point. The choice between pressure and suction systems depends on factors such as the distance to be covered, the material's properties (e.g., dustiness, moisture content), and the required flow rate. Both systems are designed to minimize material degradation and maintain product integrity throughout the conveying process.
Employing pneumatic conveying systems for rare earth materials offers several advantages over traditional methods like belt conveyors or bucket elevators. Firstly, pneumatic systems provide a closed-loop transport, which significantly reduces dust emissions and contamination, ensuring the purity of the rare earth material. This is particularly critical for rare earth elements, which are often used in high-tech applications where even minor impurities can affect performance. Secondly, these systems offer high flexibility in terms of layout and installation, as they can be easily integrated into existing production lines without extensive modifications. Thirdly, pneumatic conveying systems can handle a wide range of material characteristics, including fine powders, granules, and even sticky or abrasive materials, without causing wear or damage to the equipment. Additionally, the automated control systems in modern pneumatic conveying systems enhance operational efficiency, reduce labor costs, and improve safety by minimizing human intervention in the material handling process.
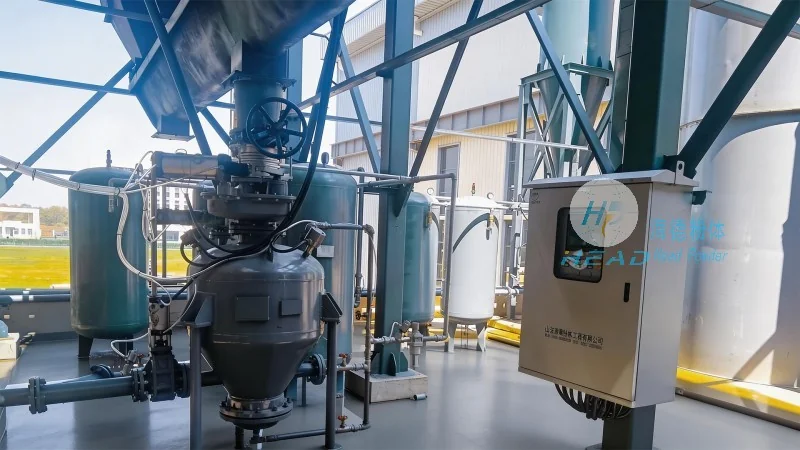
Rare earth pneumatic conveying systems are widely used in various applications within the rare earth industry. For instance, in the production of rare earth magnets, these systems are employed to transport fine rare earth oxides from storage silos to processing equipment, such as ball mills or sintering furnaces. In the manufacturing of rare earth compounds, pneumatic conveying is used to move raw materials like rare earth ores or concentrates to the extraction and purification units. Additionally, in the recycling of rare earth materials from electronic waste, pneumatic systems help in the efficient collection and transport of fine particles, ensuring a consistent feed for the recycling process. These applications highlight the versatility and reliability of pneumatic conveying systems in handling rare earth materials, which are often characterized by their fine particle size and high value.
Proper maintenance and operational considerations are essential to ensure the long-term performance and reliability of rare earth pneumatic conveying systems. Regular inspection and cleaning of the conveying line, cyclones, and filters are crucial to prevent blockages and maintain efficient material transport. The air filtration system should be checked and replaced as needed to avoid contamination of the rare earth material. Additionally, the pressure and vacuum levels should be monitored regularly to ensure they are within the optimal range for the system. The control valves and sensors should be calibrated periodically to maintain accurate flow control. Proper training of operators on the system's operation and emergency procedures is also important to ensure safe and efficient operation. By adhering to these maintenance and operational guidelines, companies can maximize the lifespan of their pneumatic conveying systems and minimize downtime, ensuring consistent and reliable material handling for their rare earth production processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top