Automatic bulk bag unloading pneumatic conveying equipment is a specialized system designed to efficiently handle the transfer of bulk materials from large flexible containers, such as super sacks or big bags, into processing or storage facilities. This equipment integrates advanced technology to streamline material handling operations, ensuring high efficiency, reliability, and minimal human intervention. The system is particularly valuable in industries where large volumes of dry or granular materials are processed, offering a solution that enhances operational productivity and reduces labor costs.
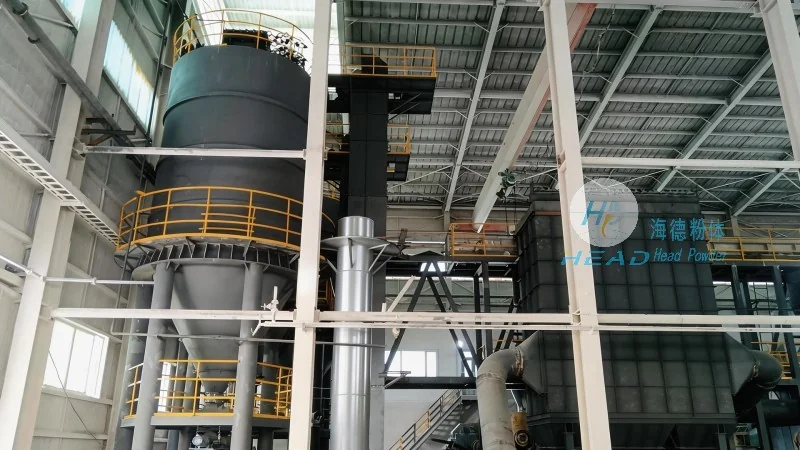
The fundamental principle of automatic bulk bag unloading pneumatic conveying equipment revolves around the use of air as the primary medium to transport materials. The system typically consists of several key components, including a bulk bag unloader, a hopper, a pneumatic conveying line, and a dust collection system. The process begins with the placement of a super sack containing the material onto the unloader. The unloader then opens the bag, allowing the material to flow into the hopper. Simultaneously, compressed air is introduced into the conveying line, creating a pressure differential that propels the material through the pipeline to the destination point. This pneumatic transport method ensures that materials are moved in a controlled manner, minimizing spillage and contamination. The system may also incorporate features like vacuum or pressure modes, depending on the specific material and application requirements. The integration of these components allows for a seamless and automated material transfer process, which is crucial for maintaining consistent production flow.
The working scene characteristics of automatic bulk bag unloading pneumatic conveying equipment are tailored to meet the diverse needs of industrial environments. These systems are commonly employed in sectors such as chemical, food, pharmaceutical, and mining industries, where the handling of bulk materials is a critical operational step. The equipment is designed to operate in various settings, from indoor processing plants to outdoor storage facilities, adapting to different spatial constraints and environmental conditions. In industrial settings, the equipment is often integrated into existing production lines, complementing other machinery like mixers, reactors, or storage silos. This integration enhances overall workflow efficiency, as materials can be transferred directly from the unloading point to the next processing stage without manual intervention. The working scene also emphasizes safety and compliance with industry standards, as the equipment is engineered to minimize dust emissions and ensure proper containment of materials. Additionally, the system's modular design allows for flexibility in installation, enabling it to be adapted to different facility layouts and operational scales. This adaptability makes the equipment suitable for both small-scale operations and large-scale industrial applications, providing a versatile solution for material handling challenges.
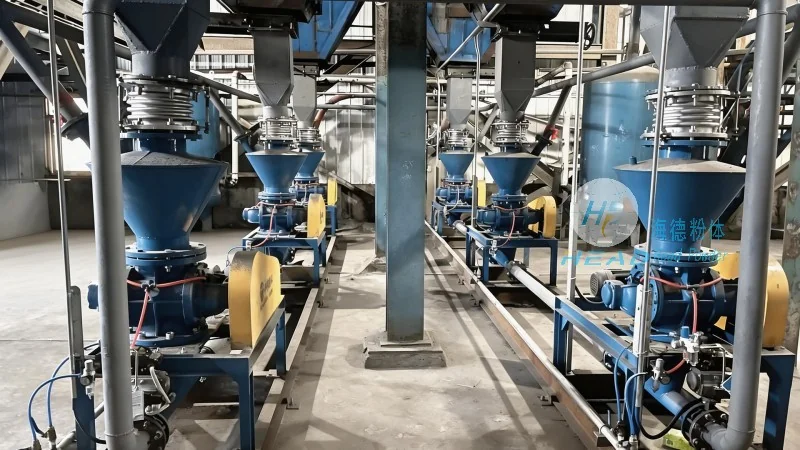
Automatic bulk bag unloading pneumatic conveying equipment offers several key features and advantages that make it a preferred choice for material handling in various industries. One of the primary advantages is its ability to handle a wide range of materials, including powders, granules, and fine particles, with minimal degradation or loss. The system's design ensures that materials are transferred gently, preserving their quality and preventing agglomeration or segregation. Another significant benefit is the reduction in labor requirements, as the equipment operates automatically, reducing the need for manual handling of heavy and bulky super sacks. This not only lowers labor costs but also enhances workplace safety by minimizing the risk of injuries associated with manual lifting and moving of bags. The equipment also contributes to improved operational efficiency through its consistent and reliable performance, ensuring that material transfer processes are completed within specified timeframes. Furthermore, the integration of dust collection systems helps maintain a clean and safe working environment, complying with environmental regulations and improving air quality in the facility. The modular and scalable nature of the system allows for easy expansion or modification as production needs evolve, providing long-term value and adaptability to changing operational requirements.
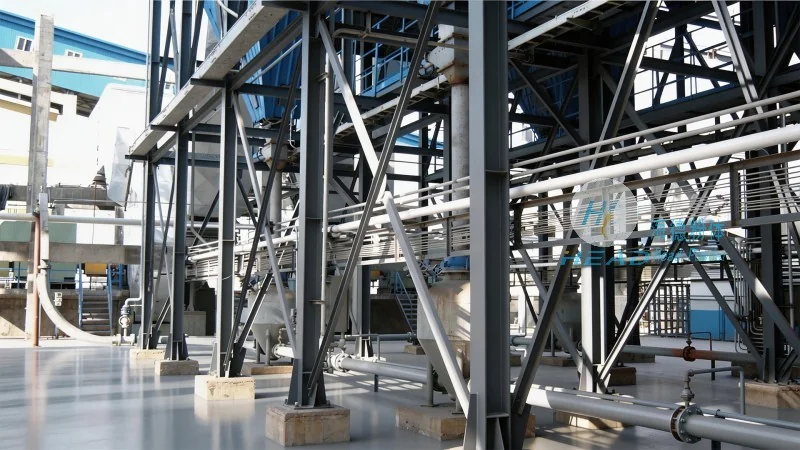
Real-world applications of automatic bulk bag unloading pneumatic conveying equipment illustrate its effectiveness in diverse industrial scenarios. For instance, in the chemical industry, the equipment is used to transfer raw materials like powders and granules from super sacks into processing reactors, ensuring a continuous and controlled supply of materials. In the food and pharmaceutical sectors, the system is employed to handle ingredients and raw materials with high standards of hygiene and purity, maintaining strict contamination control measures. The mining industry utilizes these systems to transport bulk minerals and ores from storage bags to crushing or processing equipment, enhancing the efficiency of material handling in mining operations. Each application leverages the equipment's ability to handle large volumes of materials with precision and reliability, contributing to improved production output and reduced downtime. The adaptability of the system to different material types and operational conditions makes it a versatile solution for various industrial challenges, demonstrating its practical utility in real-world settings.
Automatic bulk bag unloading pneumatic conveying equipment represents a sophisticated solution for efficient material handling in modern industrial operations. By integrating advanced pneumatic technology with automated unloading mechanisms, the system addresses the challenges of handling large volumes of bulk materials while maintaining operational efficiency and safety. The working scene characteristics and key features of this equipment make it an ideal choice for industries requiring reliable and consistent material transfer processes. As production demands continue to evolve, the adaptability and scalability of these systems ensure they remain a valuable asset for enhancing operational productivity and reducing costs. The implementation of such equipment by companies like Shandong HeadPowder Engineering Co., Ltd. reflects a commitment to leveraging advanced technology to improve industrial processes and meet the evolving needs of the market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top