For cement production facilities, the efficient and reliable transportation of dry fly ash materials is crucial for maintaining production efficiency and ensuring environmental compliance. Pneumatic conveying equipment, specifically designed for handling cement dry fly ash, plays a vital role in this process. This equipment is engineered to handle the unique characteristics of dry fly ash, such as its fine particle size, low bulk density, and tendency to generate dust during handling. By utilizing air as the primary medium for material transport, these systems offer a solution that minimizes manual labor, reduces the risk of material contamination, and enhances overall operational safety.
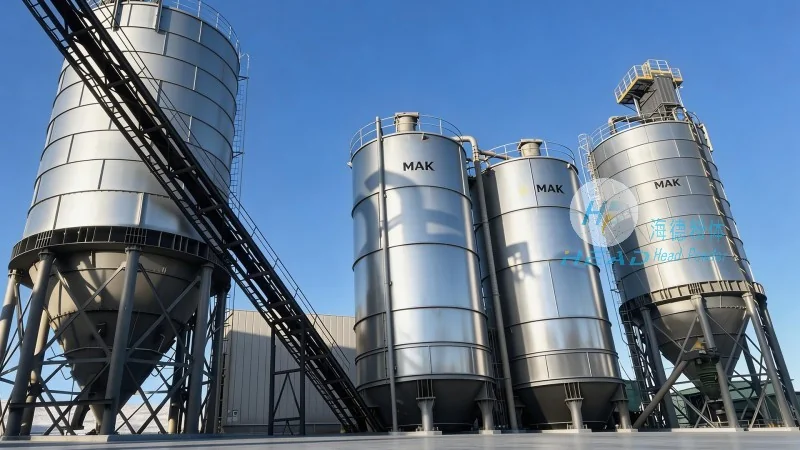
The core principle of pneumatic conveying for cement dry fly ash involves the use of air pressure to move solid particles through a sealed pipeline. There are two primary types of pneumatic conveying systems: positive pressure and negative pressure. In a positive pressure system, a high-pressure fan forces air into the conveying line, creating a positive pressure that propels the dry fly ash material forward. The material is typically fed into the system at the inlet, where it mixes with the air stream and is carried to the discharge point. Conversely, a negative pressure system operates by drawing air out of the pipeline, creating a vacuum that pulls the dry fly ash material into the system. The fan is located at the discharge end, and the material is drawn from the source (e.g., a storage silo or a dust collector) into the pipeline.
For cement dry fly ash, positive pressure systems are often preferred due to their ability to handle larger quantities of material and their suitability for long-distance transport. These systems are equipped with components such as feeders, airlocks, and filters to ensure consistent material flow and prevent air leakage. The feeders, typically screw or rotary types, meter the dry fly ash into the conveying line at a controlled rate, while the airlocks maintain airtight seals between the feeder and the pipeline. Filters are essential to capture any fine particles that may escape, protecting the fan and downstream equipment from damage.
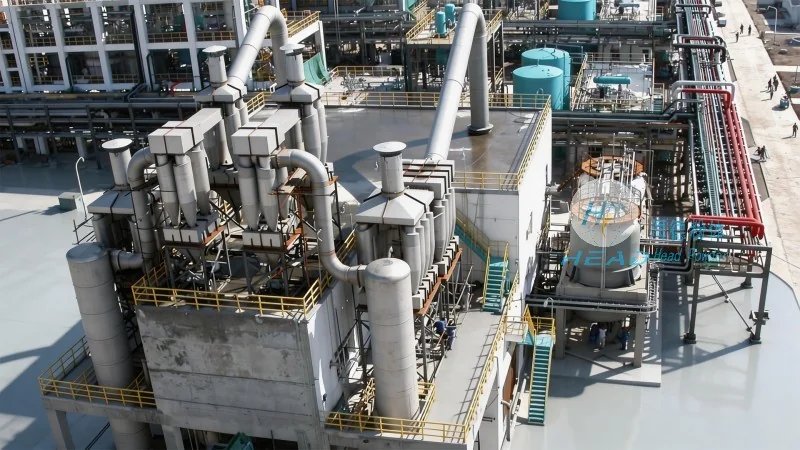
HeadPowder's pneumatic conveying equipment for cement dry fly ash is designed with several key features that address the specific challenges of handling this material. One of the primary advantages is the high efficiency in material transport, as the system can move large volumes of dry fly ash over significant distances with minimal energy consumption compared to traditional methods like truck or belt conveyors. The equipment also offers excellent dust control, as the entire process is enclosed within a sealed system, preventing the release of fine particles into the environment. This not only improves air quality but also reduces the risk of material loss and contamination.
Another critical feature is the adaptability of the system to varying material characteristics. Cement dry fly ash can have different particle sizes, moisture contents, and bulk densities depending on the source and processing conditions. The equipment is engineered to accommodate these variations through adjustable parameters such as air pressure, flow rate, and feeder speed. This flexibility ensures consistent performance even with changes in the material being handled.
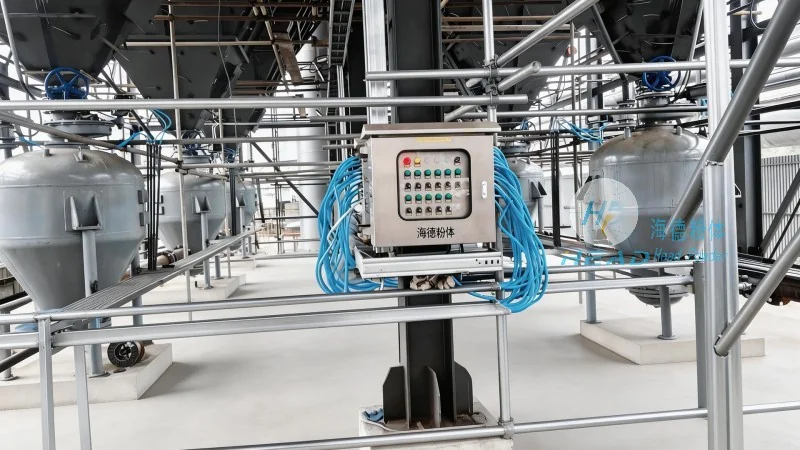
The equipment also contributes to operational safety and maintenance efficiency. By eliminating the need for manual handling of dry fly ash, the risk of respiratory issues or skin irritation from dust exposure is significantly reduced. Additionally, the sealed system design minimizes the need for frequent cleaning and maintenance, as the internal components are protected from direct contact with the material. The use of durable materials, such as stainless steel or corrosion-resistant alloys, further enhances the longevity of the equipment, reducing the need for frequent replacements and lowering long-term operational costs.
In the cement industry, the application of pneumatic conveying equipment for dry fly ash is widespread and essential for optimizing production processes. One common scenario is the recovery and transport of fly ash from the kiln system. In cement production, fly ash is generated as a byproduct from the combustion of coal or other fuels in the kiln. This fly ash is collected from the kiln exhaust system and processed into a dry powder. The pneumatic conveying equipment then transports this dry fly ash from the dust collection system to a storage silo or directly to the cement production line, where it can be used as a supplementary cementitious material (SCM) to improve the properties of the final cement product.
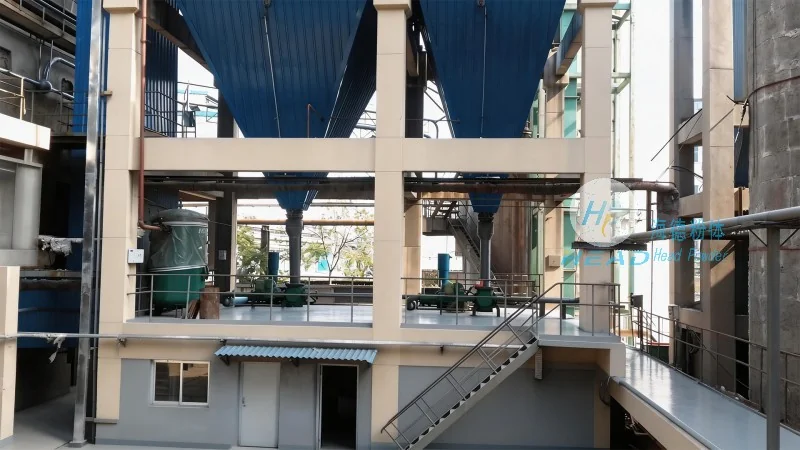
Another application is the transfer of dry fly ash from storage silos to the production facilities. In many cement plants, dry fly ash is stored in large silos after initial processing. The pneumatic conveying system is used to move the material from the storage silo to the blending or grinding equipment, ensuring a continuous and consistent supply of fly ash for cement production. This application is particularly important for plants that rely on fly ash as a key ingredient in their cement mix, as it helps to reduce the consumption of natural raw materials and lower the overall cost of production.
Furthermore, the equipment is used in scenarios where dry fly ash needs to be transported between different parts of the cement plant, such as from the raw material handling area to the kiln or from the clinker processing area to the storage area. The ability to handle long-distance transport without the need for intermediate storage or manual handling makes the pneumatic conveying system ideal for these applications. By integrating this equipment into the overall production workflow, cement plants can achieve greater operational efficiency, reduce downtime, and improve the overall quality of their cement products.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top