HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems for handling magnesium sulfate. This article delves into the fundamental principles behind such systems and highlights the key characteristics of their operational scenarios, providing a comprehensive overview for industry professionals and potential clients.
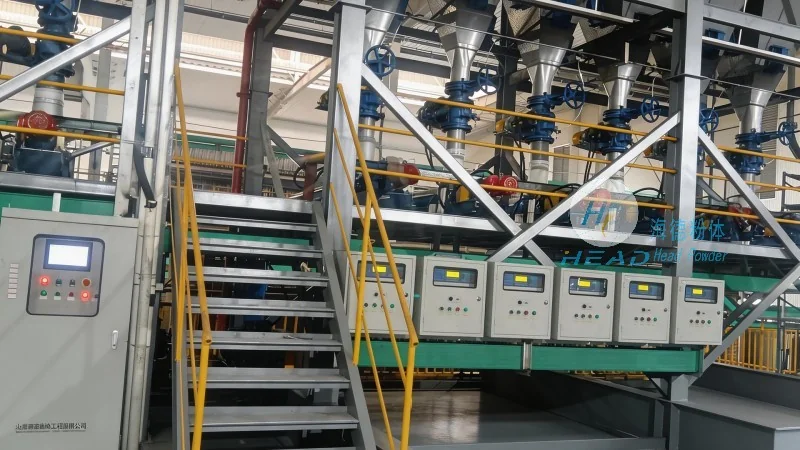
The pneumatic conveying system for magnesium sulfate operates on the principle of transporting bulk materials through a pipeline using a stream of pressurized air or other gas. Unlike traditional mechanical conveyors, this method eliminates the need for moving parts in contact with the material, reducing wear and maintenance costs. The system typically consists of a hopper, a feeder, a conveying line, and a receiver. The hopper stores the magnesium sulfate, and the feeder controls the material flow into the conveying line. The pressurized air or gas is introduced at the inlet of the line, creating a low-pressure zone that draws the material into the pipeline. As the material travels through the line, it is suspended and transported to the receiver, where it is deposited. This process is highly efficient for handling fine or dusty materials like magnesium sulfate, which can be prone to caking or segregation in traditional systems. Specifically, magnesium sulfate is hygroscopic, meaning it absorbs moisture from the air, which can affect its flowability and handling characteristics. Therefore, the system design must consider moisture control and material conditioning to ensure consistent performance. The use of air filters and moisture separators in the system helps maintain the material's quality and prevents blockages in the pipeline.
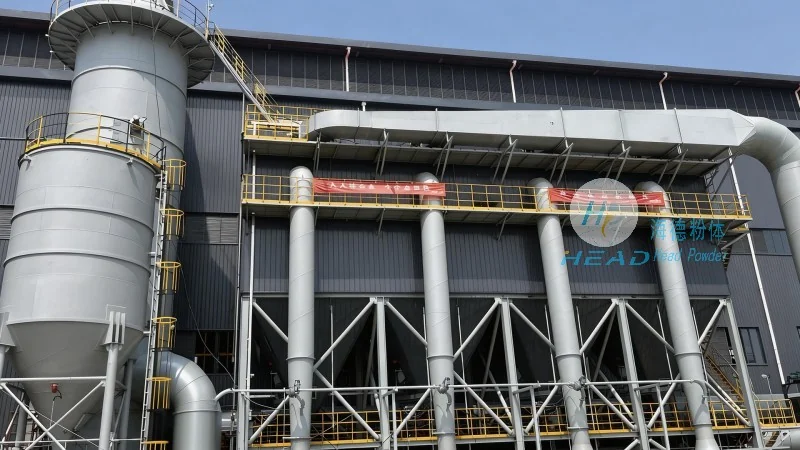
The operational characteristics of magnesium sulfate pneumatic conveying systems are tailored to specific industrial environments, ensuring optimal performance and safety. One of the primary characteristics is the ability to handle varying material properties, such as different particle sizes, moisture content, and flowability. The system's design allows for adjustments in air velocity and pressure to accommodate these variations, maintaining consistent material transport rates. Another critical characteristic is the system's flexibility in terms of layout and integration with existing facilities. It can be configured for both short-distance and long-distance transport, and can be integrated with other processing equipment, such as storage silos, mixers, or packaging lines. This adaptability makes it suitable for diverse applications, from small-scale laboratory operations to large-scale industrial production lines. For instance, in a pharmaceutical manufacturing plant, the system can be integrated with a granulation unit to transport magnesium sulfate for use as an excipient, ensuring precise dosing and uniform mixing. In a chemical processing facility, the system may be used to transport magnesium sulfate from a drying unit to a packaging line, where it is used as a raw material for other chemical products.
In industrial settings, the pneumatic conveying system for magnesium sulfate offers several advantages that enhance operational efficiency and product quality. For instance, in pharmaceutical or food processing industries, where material purity is paramount, the system minimizes contamination risks by avoiding direct contact with metal parts or other materials. The enclosed pipeline design also helps in controlling dust emissions, ensuring compliance with environmental regulations. In chemical manufacturing, the system's ability to handle corrosive or reactive materials, such as magnesium sulfate, is particularly valuable. The use of appropriate materials for the conveying line, such as stainless steel or special plastics, prevents material degradation and equipment corrosion. Additionally, the system's energy efficiency is a significant benefit, as it requires less power compared to mechanical conveyors, leading to lower operational costs over time. The pressurized air system can be optimized to use minimal energy while maintaining the required transport capacity, contributing to overall cost savings and environmental sustainability.
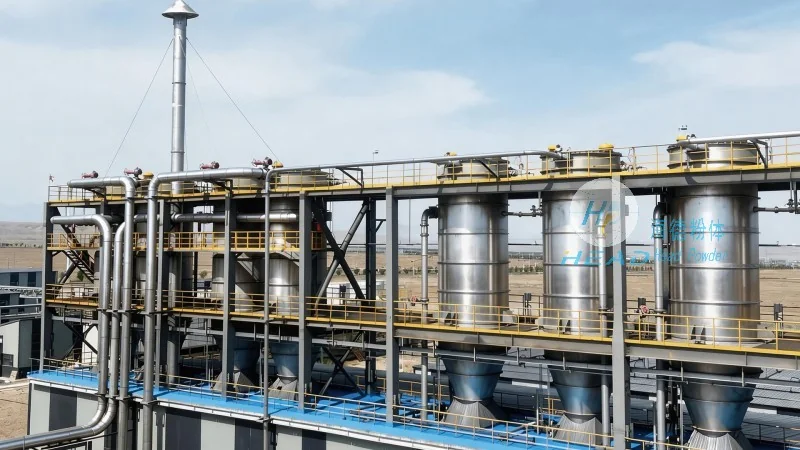
HeadPowder has successfully implemented magnesium sulfate pneumatic conveying systems in various industrial applications. For example, in a chemical plant producing magnesium sulfate heptahydrate, the system was designed to transport raw material from storage silos to a reaction vessel. The system's high capacity and reliability ensured a continuous supply of material, reducing downtime and increasing production output. The system was configured with a variable speed feeder to control the material flow rate, matching the reaction process requirements. In another case, a food processing facility used the system to convey magnesium sulfate for use as a food additive. The system's hygienic design and easy cleaning features met the stringent food safety standards, providing a safe and efficient solution. The use of stainless steel components and CIP (Clean-In-Place) compatible parts ensured that the system could be sanitized without disassembly, maintaining product purity. These examples illustrate the system's versatility and effectiveness in different operational contexts, demonstrating its value to industries that require reliable and efficient material handling solutions. The successful implementations by HeadPowder highlight the company's expertise in tailoring pneumatic conveying systems to meet the specific needs of clients, ensuring optimal performance and long-term operational benefits.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top