For industrial operations involving the transport of bulk powder materials, pneumatic conveying systems offer a versatile and efficient solution. Understanding the underlying principles and diverse application scenarios of these systems is crucial for selecting the right technology for specific operational needs. This article explores the fundamental principles of powder material pneumatic conveying and highlights key characteristics of various working scenarios, providing insights into how these systems enhance material handling processes.
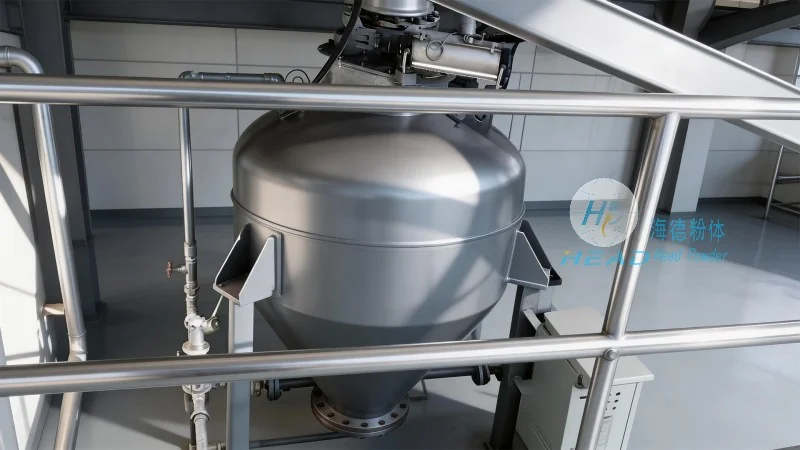
Pneumatic conveying relies on the use of air or other gases to transport solid particles through a pipeline. The core principle involves creating a pressure differential or utilizing suction to move the powder from the source to the destination. There are primarily two types of pneumatic conveying systems: pressure and vacuum systems. Pressure systems operate by blowing air or gas into the pipeline, pushing the powder forward, while vacuum systems create a negative pressure at the receiving end, drawing the material through the line.
The effectiveness of a pneumatic conveying system depends on several key factors, including the particle size, density, and flowability of the material, as well as the design of the conveying line, including pipe diameter, length, and bends. Proper system design ensures that the powder is conveyed efficiently without clogging or degradation. For example, in pressure systems, the air velocity must be sufficient to keep the particles suspended and prevent deposition, while in vacuum systems, the suction rate needs to match the material's flow characteristics to maintain a stable flow.
The application of pneumatic conveying systems varies widely across different industries, each with distinct requirements and operational conditions. Understanding these scenarios helps in optimizing system performance and ensuring reliability in material handling processes.
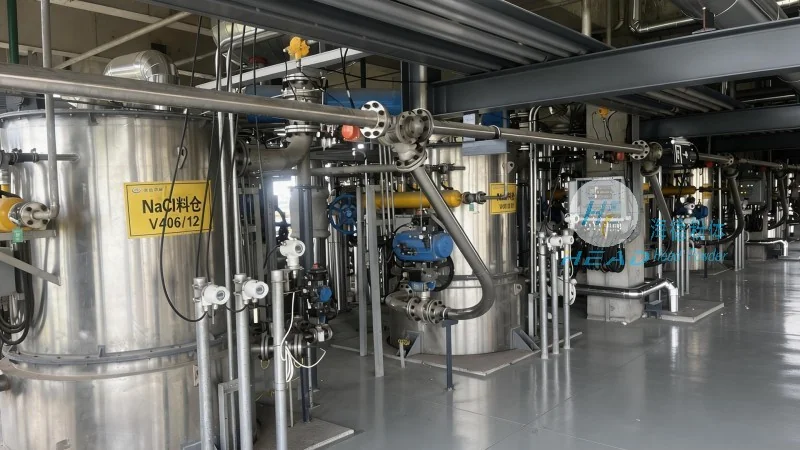
In industrial manufacturing, pneumatic conveying is commonly used for transporting raw materials, intermediate products, and finished goods. For instance, in the pharmaceutical industry, it is employed to move powders such as active pharmaceutical ingredients (APIs) and excipients with high purity requirements. The systems are designed to minimize contamination and ensure product integrity, often incorporating closed-loop or sterile conveying options. Similarly, in the chemical and petrochemical sectors, pneumatic conveying handles a wide range of powders, from fine chemicals to bulk raw materials, supporting continuous production lines.
The food and beverage industry utilizes pneumatic conveying for handling powders like flour, sugar, and spices. The primary considerations in this sector include hygiene, safety, and product quality. Systems are typically constructed from food-grade materials and designed to prevent cross-contamination. The conveying process is often integrated with other processing steps, such as mixing and packaging, to streamline production. For example, in a bakery, pneumatic conveying can efficiently transport flour from storage silos to mixing machines, ensuring consistent product quality and reducing manual handling risks.
In the construction industry, pneumatic conveying is used for transporting bulk materials like cement, sand, and gravel. These materials are often heavy and abrasive, requiring robust system components to withstand wear and tear. The systems are designed with larger pipe diameters and high-pressure capabilities to handle the high flow rates and particle sizes typical of construction applications. Additionally, the conveying lines are often integrated with storage silos and mixing equipment to support on-site production and reduce material handling time.
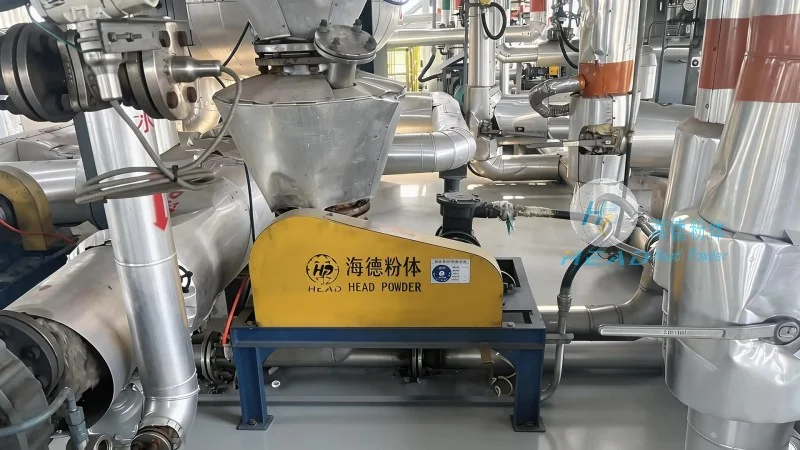
Pneumatic conveying plays a vital role in environmental and waste management applications, such as the transport of fly ash from power plants and the handling of industrial waste materials. These systems help in reducing the need for manual handling and transportation, improving safety and efficiency. The design of these systems often includes dust collection and filtration to minimize environmental impact and comply with regulatory standards. For instance, in a power plant, pneumatic conveying is used to transport fly ash from the boiler to storage silos, enabling the reuse of the material in cement production and reducing landfill waste.
Each working scenario presents unique advantages and considerations for pneumatic conveying systems. In industrial manufacturing, the ability to handle high volumes and maintain product purity is critical, making pressure systems with closed-loop designs preferred. In the food industry, hygiene and safety are paramount, leading to the use of stainless steel components and positive pressure systems to prevent contamination. In construction, durability and high flow rates are key, resulting in the adoption of robust pressure systems with large pipe diameters. In environmental applications, the focus is on efficiency and environmental compliance, often incorporating dust control measures and material recycling options.
Pneumatic conveying systems offer a flexible and efficient solution for the transport of powder materials across various industries. By understanding the underlying principles and adapting to different working scenarios, these systems enhance operational efficiency, reduce costs, and improve product quality. As industries continue to evolve, the demand for advanced pneumatic conveying technologies will likely increase, driven by the need for more sustainable and efficient material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top