Quartz stone powder, a crucial material in various industrial applications such as construction, manufacturing, and chemical processing, requires efficient and reliable transportation methods to ensure smooth production workflows. The quartz stone powder pneumatic conveying machine has emerged as a sophisticated solution to address the challenges associated with handling fine powders, offering a hygienic, dust-free, and energy-efficient alternative to traditional bulk material handling systems. This article delves into the fundamental principles of these machines and explores the distinct working scene characteristics that make them ideal for quartz stone powder applications.
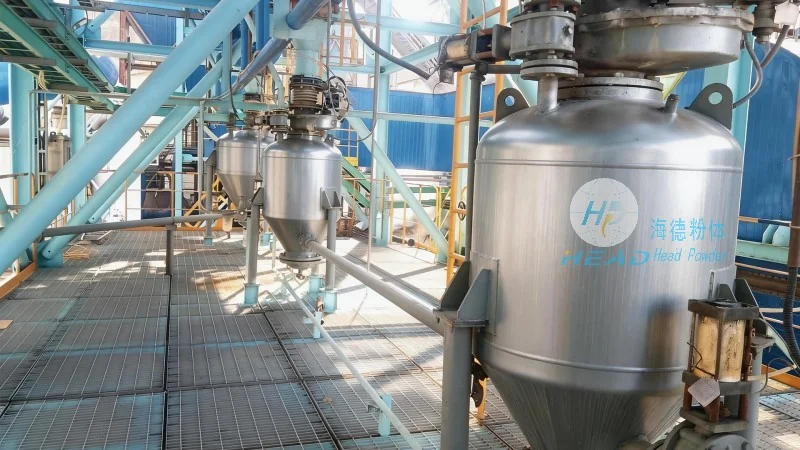
At the heart of quartz stone powder pneumatic conveying machines lies the principle of transporting solid particles through a pipeline using a pressurized or vacuum air stream. This method, known as pneumatic conveying, eliminates the need for mechanical components like belts or buckets, reducing maintenance requirements and minimizing the risk of material contamination. The process typically involves a hopper where quartz stone powder is fed into the system, followed by an air compressor that generates the necessary pressure to move the powder through the pipeline. The air stream carries the powder particles, ensuring consistent flow and preventing clogging or blockages that are common in traditional systems. For quartz stone powder, which is often fine and abrasive, this method is particularly advantageous as it prevents particle degradation and maintains the material's integrity throughout the conveying process.
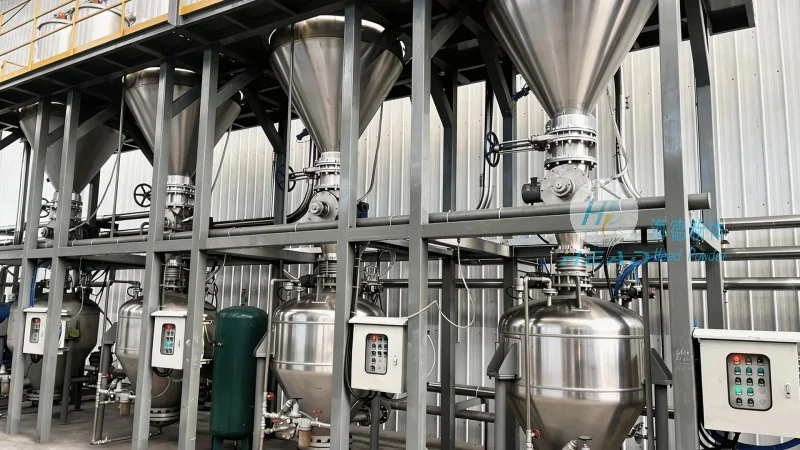
The working scene characteristics of quartz stone powder pneumatic conveying machines are tailored to meet the specific demands of industrial environments where quartz stone powder is processed. These characteristics include: 1. Hygienic and Dust-Free Operation, which is critical in food processing, pharmaceuticals, and other industries where contamination control is paramount. The enclosed system prevents dust dispersion, ensuring a clean working environment and compliance with regulatory standards. 2. Flexibility in Layout and Integration, as the pneumatic conveying system can be easily integrated into existing production lines or reconfigured to accommodate changes in workflow. This adaptability is essential in dynamic industrial settings where production requirements may evolve over time. 3. Energy Efficiency and Cost-Effectiveness, as the system minimizes energy consumption compared to traditional methods, leading to lower operational costs and reduced environmental impact. The use of air as the conveying medium is also more economical than other bulk handling solutions, making it a cost-effective choice for long-term operation. 4. Scalability and Capacity, allowing the system to handle varying volumes of quartz stone powder, from small-scale laboratory applications to large-scale industrial production. This scalability ensures that the machine can grow with the needs of the business, providing a long-term investment with high return on investment (ROI).
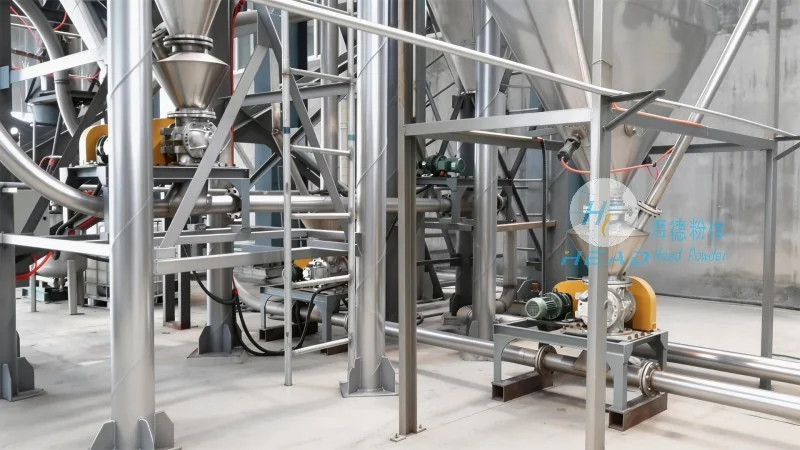
Quartz stone powder pneumatic conveying machines are widely used across various industries due to their versatility and efficiency. In the construction industry, these machines are employed to transport quartz stone powder for concrete mixing, tile manufacturing, and other building material production. The consistent flow and dust-free operation ensure that the quality of the final product is maintained, leading to higher durability and performance of the constructed materials. In the chemical industry, quartz stone powder is used as a filler or additive in the production of coatings, adhesives, and plastics. The pneumatic conveying system ensures that the powder is delivered to the processing equipment without any contamination, which is crucial for maintaining the purity of the final chemical products. Additionally, in the manufacturing of electronic components and optical devices, quartz stone powder is used for polishing and grinding applications. The precise control of the conveying system allows for the delivery of the powder to the processing tools with minimal variation, enhancing the quality of the finished products.
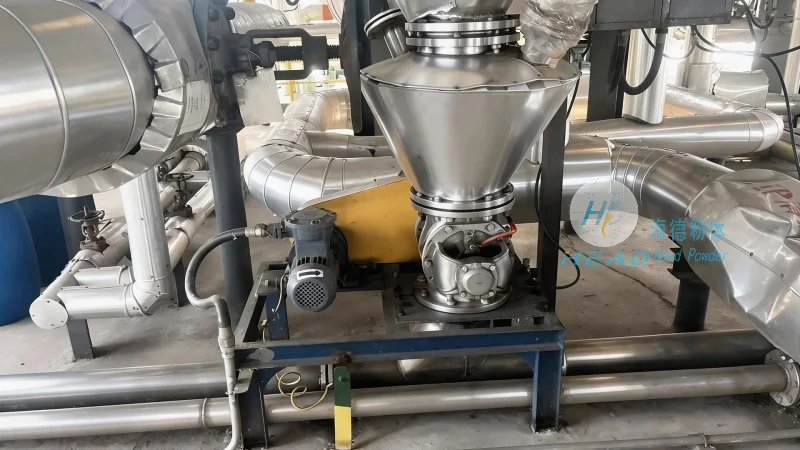
For businesses seeking reliable and efficient quartz stone powder pneumatic conveying solutions, Shandong HeadPowder Engineering Co., Ltd. (headpowder) stands out as a leading provider of industrial equipment. With a strong commitment to quality and innovation, headpowder specializes in designing and manufacturing customized pneumatic conveying systems tailored to the unique needs of each client. The company's expertise in material handling technology ensures that their machines are built to withstand the demands of quartz stone powder, which is often abrasive and fine. Headpowder's products are known for their durability, low maintenance requirements, and energy efficiency, making them a cost-effective choice for long-term operation. The company's team of engineers and technicians work closely with clients to understand their specific requirements, providing tailored solutions that enhance productivity and reduce operational costs. Headpowder's focus on customer satisfaction and technical support ensures that clients receive not only high-quality equipment but also the necessary guidance to maximize the benefits of their investment. By choosing headpowder, businesses can rely on a trusted partner that delivers reliable, efficient, and cost-effective quartz stone powder pneumatic conveying solutions, helping them achieve their production goals with minimal disruptions and maximum efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top