HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for handling dust and powder materials. This article delves into the fundamental principles of dust collection powder body pneumatic conveying machines and explores the key characteristics of their operational environments.
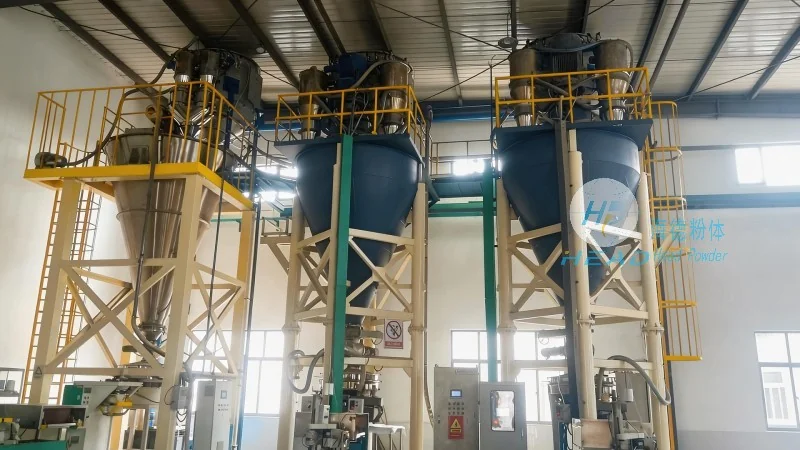
The pneumatic conveying machine operates on the principle of using compressed air to transport bulk materials like dust and powders through a pipeline. In the context of dust collection, these systems efficiently capture and transport collected powders from industrial processes, such as cement production, chemical manufacturing, or mining operations. The core mechanism involves creating a pressure differential within the pipeline, where air is introduced at one end to generate a flow that pulls the powder particles along. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and enhancing safety in hazardous environments.
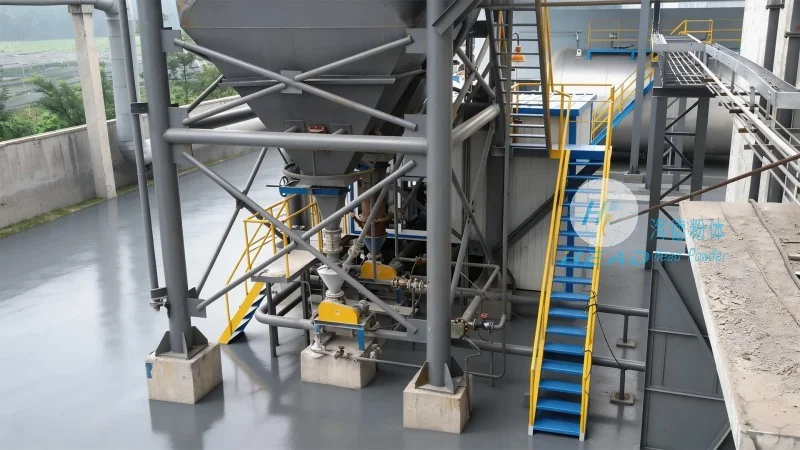
The operational characteristics of these machines are closely tied to the specific industrial applications they serve. For instance, in cement plants, the system must handle high volumes of fine powders while maintaining consistent flow rates to prevent blockages. In chemical processing facilities, the equipment may need to accommodate corrosive or abrasive materials, requiring specialized materials for the pipeline and components. Additionally, the design of the conveying system must consider the dust's particle size distribution, moisture content, and bulk density to ensure optimal performance. The working scene often involves integration with existing dust collection systems, such as baghouses or electrostatic precipitators, to streamline material handling and improve overall process efficiency.
One of the primary advantages of dust collection powder body pneumatic conveying machines is their ability to handle materials that are difficult to transport using traditional methods. Unlike screw conveyors or bucket elevators, pneumatic systems can transport powders over long distances without the risk of material degradation or contamination. This makes them ideal for applications where product purity is critical, such as in pharmaceutical or food processing industries. Furthermore, the enclosed pipeline design minimizes dust emissions, contributing to better air quality and compliance with environmental regulations. The flexibility of the system allows for easy integration into existing production lines, reducing downtime and increasing operational efficiency.
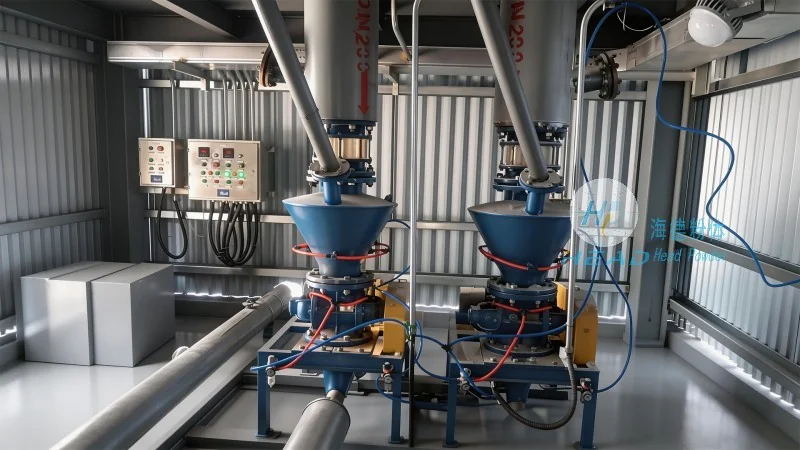
HeadPowder offers customized solutions to meet the unique requirements of each client's operational environment. The company's engineers work closely with clients to design systems that align with specific material properties, flow rates, and distance requirements. The equipment is constructed using high-quality materials, such as stainless steel or special alloys, to withstand the rigors of continuous operation and resist corrosion from aggressive powders. Regular maintenance is essential to ensure the longevity and reliability of the system. This includes checking air pressure, inspecting pipeline for blockages, and replacing worn components. By adhering to a proper maintenance schedule, users can maximize the lifespan of the pneumatic conveying machine and minimize operational disruptions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top