The desulfurization sodium bicarbonate material handling system is a specialized equipment designed for the efficient transport and management of sodium bicarbonate, a key reagent in flue gas desulfurization processes. This system is engineered to meet the demanding requirements of industrial applications, ensuring reliable and safe material transfer from storage to processing units. The system's design integrates advanced control mechanisms and robust construction to handle the unique properties of sodium bicarbonate, which is often used in power plants and other industrial facilities to reduce sulfur dioxide emissions.
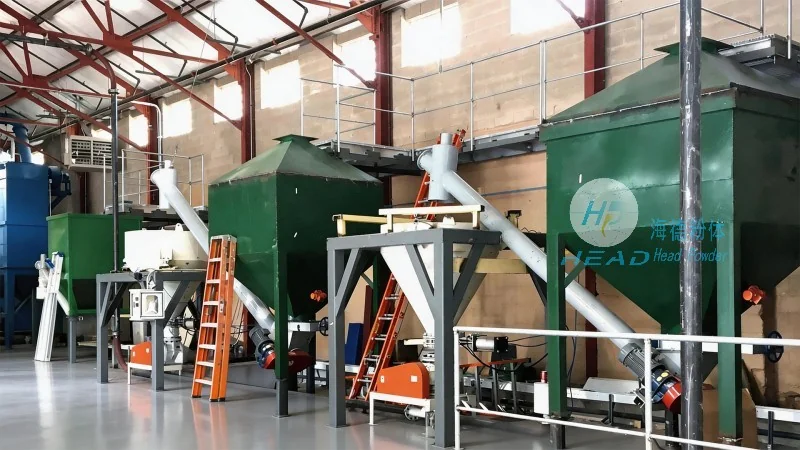
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer and supplier of industrial material handling solutions. With operations based in Shandong, China, the company specializes in developing customized equipment for various chemical and industrial sectors. HeadPowder's expertise lies in understanding the specific challenges of material transport in high-purity and high-temperature environments, which is crucial for applications like flue gas desulfurization where precision and reliability are paramount.
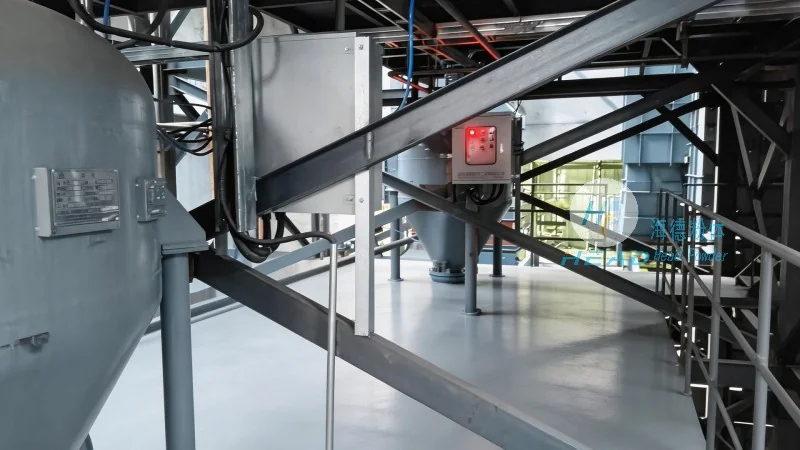
The desulfurization sodium bicarbonate material handling system operates on a combination of mechanical and pneumatic principles to ensure seamless material transfer. The system typically includes storage silos, conveyor systems, and dosing mechanisms that work in tandem to deliver the correct amount of sodium bicarbonate to the desulfurization reactor. Key components such as rotary valves, screw conveyors, and pneumatic feeders are integrated to handle the bulk material efficiently. The control system, often equipped with PLC (Programmable Logic Controller) technology, monitors and adjusts the flow rate based on real-time process parameters, ensuring optimal performance and minimal waste. This integrated approach minimizes the risk of material degradation and ensures consistent quality in the final product or process output.
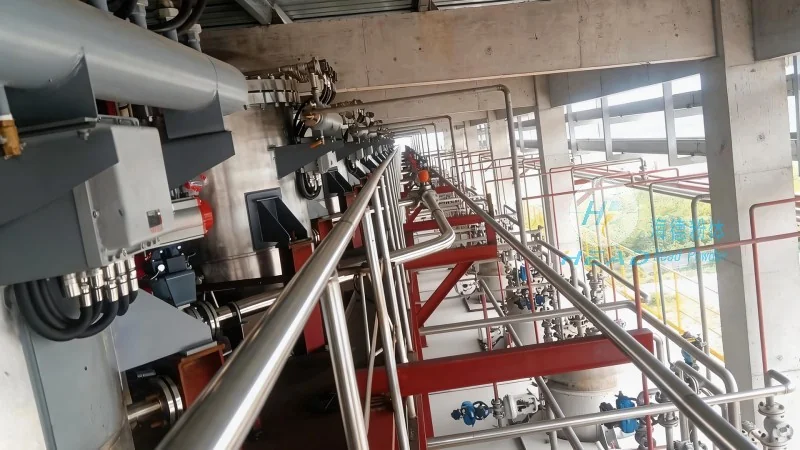
The desulfurization sodium bicarbonate material handling system is widely used in power generation plants, chemical manufacturing facilities, and other industrial settings where flue gas desulfurization is a critical component of emissions control. The system's design is tailored to handle the high volume and continuous operation required in these environments. For instance, in coal-fired power plants, the system ensures a steady supply of sodium bicarbonate to the scrubber system, which neutralizes sulfur dioxide in the exhaust gases. The system's robust construction and corrosion-resistant materials make it suitable for harsh industrial conditions, where exposure to moisture, temperature fluctuations, and chemical residues is common. Additionally, the system's modular design allows for easy integration with existing infrastructure, reducing installation time and costs for new or upgraded facilities. This adaptability makes the system a versatile solution for various industrial applications, from small-scale pilot plants to large-scale commercial operations.
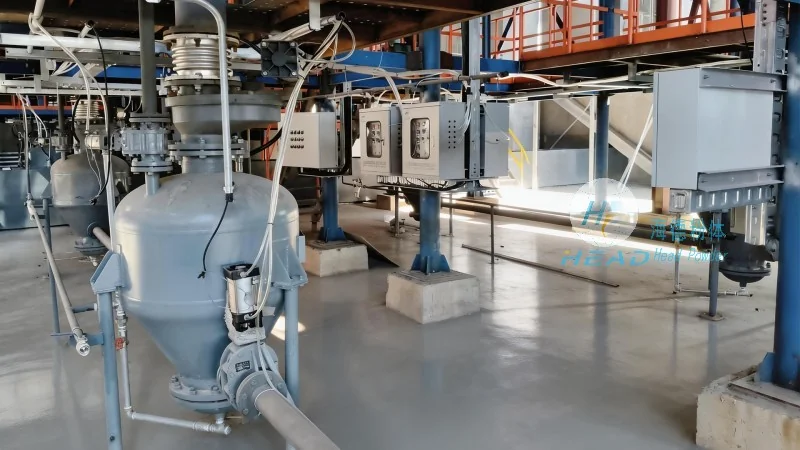
HeadPowder's desulfurization sodium bicarbonate material handling system offers several advantages that enhance operational efficiency and reduce maintenance costs. The system's high-capacity design can handle large volumes of sodium bicarbonate, minimizing downtime and ensuring continuous operation. The use of advanced materials, such as stainless steel and corrosion-resistant alloys, extends the equipment's service life and reduces the need for frequent replacements. The integrated control system provides real-time monitoring and data logging, enabling operators to track performance metrics and identify potential issues before they escalate. This proactive approach to maintenance improves system reliability and reduces unplanned downtime. Furthermore, the system's energy-efficient design reduces operational costs by optimizing power consumption during material transport. These advantages make the system a cost-effective solution for industrial facilities seeking to improve their material handling processes and comply with environmental regulations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top