HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced material handling solutions. This article delves into the fundamental principles and operational characteristics of sintered dust material conveying systems, highlighting how these systems efficiently manage and transport fine particulate materials in industrial settings.
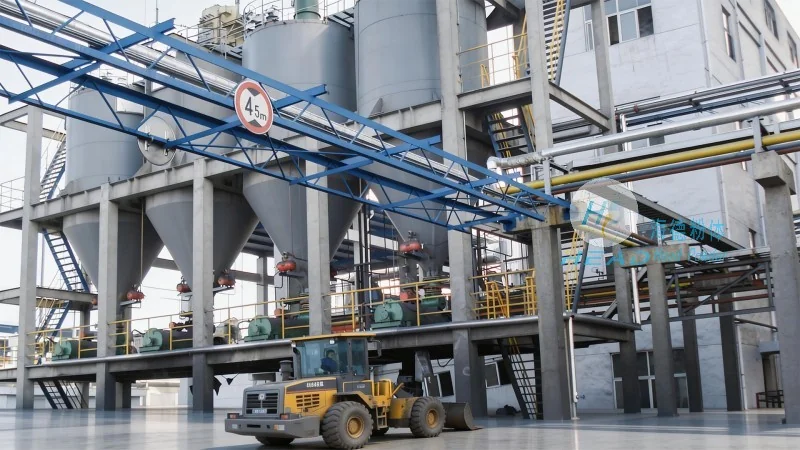
The sintered dust material conveying system is engineered to handle fine, dry powders and dust particles commonly encountered in industrial processes such as sintering, mining, and chemical production. The system operates on the principle of pneumatic or mechanical transport, utilizing specialized components to ensure efficient material movement while maintaining safety and environmental compliance. Key components include dust collection hoppers, conveying pipes, air or mechanical drive mechanisms, and discharge units. The design prioritizes minimizing dust dispersion, ensuring that the material is transported with minimal loss and optimal control over particle size distribution.
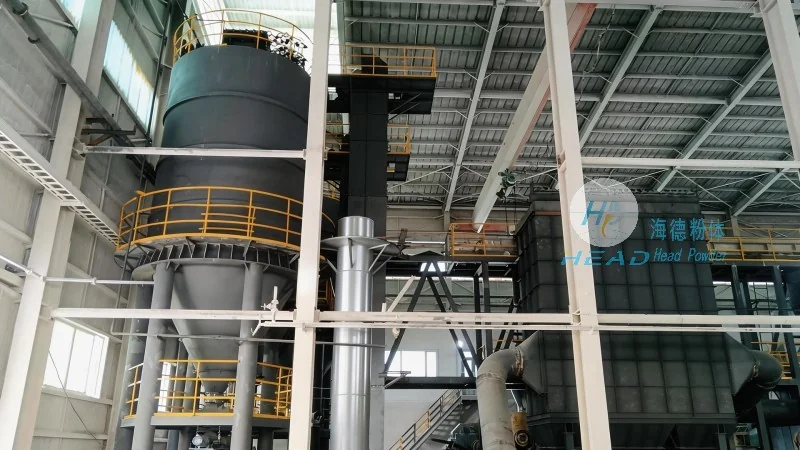
These conveying systems are deployed in diverse industrial environments, each with unique operational requirements. For instance, in sintering plants, the system efficiently transports sintered dust from processing units to storage or recycling facilities, ensuring a continuous material flow. In mining operations, it handles fine ore dust, reducing the risk of dust-related hazards and improving workplace safety. The systems are also used in chemical and pharmaceutical industries for transporting fine powders, where precision and contamination control are critical. The working scene characteristics include high material throughput, low maintenance requirements, and adaptability to varying particle sizes and moisture content. The systems are designed to operate in both indoor and outdoor settings, with options for enclosed or open-air configurations depending on the specific application needs.
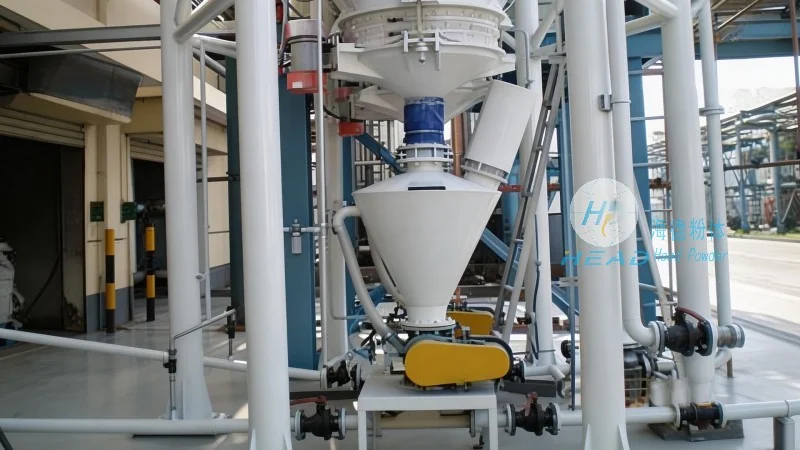
HeadPowder's sintered dust material conveying systems offer several advantages that make them ideal for demanding industrial applications. The systems are built for durability, with robust materials and components that withstand continuous operation and harsh environmental conditions. They provide high efficiency in material transport, reducing downtime and operational costs. Additionally, the systems are designed with safety features such as dust suppression mechanisms and emergency shut-off valves, ensuring compliance with industrial safety standards. Technical specifications vary based on the specific model, but common features include adjustable conveying speeds, variable pressure control, and modular design for easy integration into existing production lines. The systems are capable of handling a wide range of particle sizes, from fine powders to small granules, making them versatile for multiple industrial processes.
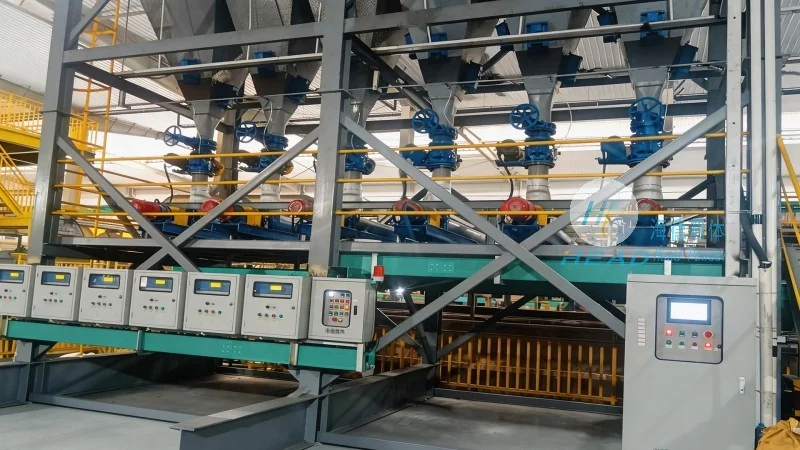
HeadPowder's sintered dust material conveying systems exemplify advanced engineering solutions tailored to the unique challenges of industrial material handling. By combining efficient transport mechanisms with robust design and safety features, these systems enhance operational efficiency, reduce environmental impact, and improve workplace safety. With a strong presence in Shandong, China, HeadPowder continues to provide reliable and innovative solutions for industries relying on the consistent and safe transport of fine materials. The company's commitment to quality and customer satisfaction ensures that clients receive systems that meet their specific operational requirements and contribute to long-term productivity and sustainability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top