HeadPowder, a leading provider of industrial material handling solutions, specializes in the design and manufacturing of advanced corn cobs material conveying systems. These systems are engineered to efficiently transport corn cobs, a byproduct of corn processing, from one location to another within agricultural and food processing facilities. The core of such systems lies in their ability to handle the unique physical properties of corn cobs, ensuring minimal damage and optimal throughput.
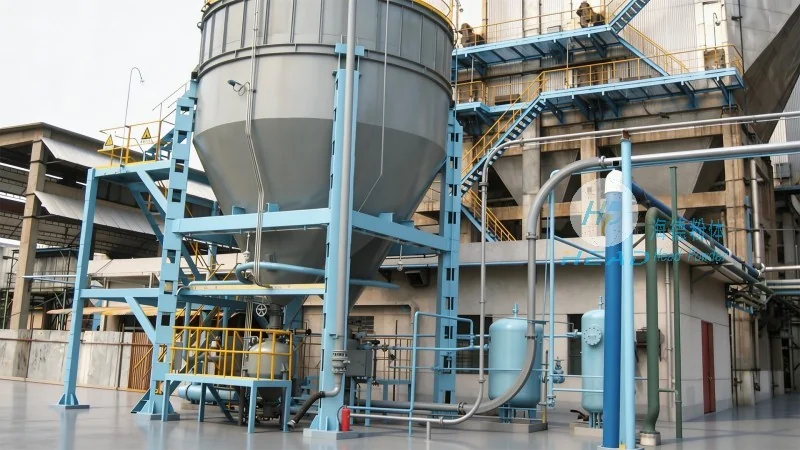
The fundamental principle behind corn cobs material conveying systems is the utilization of mechanical force to move bulk materials. These systems typically employ a combination of components such as feed hoppers, conveyor belts, or screw conveyors, depending on the specific application and the characteristics of the corn cobs. The feed hopper is designed to collect and store the corn cobs, ensuring a consistent flow into the conveyor mechanism. The conveyor system then transports the material along a designated path, often with adjustable speed and direction controls to match the operational requirements of the processing plant.
Key components of the system include the drive mechanism, which provides the necessary power to move the conveyor, and the idler rollers or pulleys that support the conveyor belt or screw. The drive mechanism may be electric, hydraulic, or mechanical, depending on the system's capacity and the operational environment. Additionally, the system incorporates safety features such as emergency stop buttons and overload protection to prevent accidents and ensure smooth operation.
HeadPowder's corn cobs material conveying systems are tailored for diverse working environments, including large-scale corn processing plants, feed mills, and agricultural storage facilities. The primary working scene characteristics are centered around the need for high efficiency, reliability, and adaptability to varying corn cob sizes and moisture content. In corn processing plants, these systems are often integrated into the overall production line, where they connect the corn cobs collection area to the subsequent processing stages, such as drying or grinding.
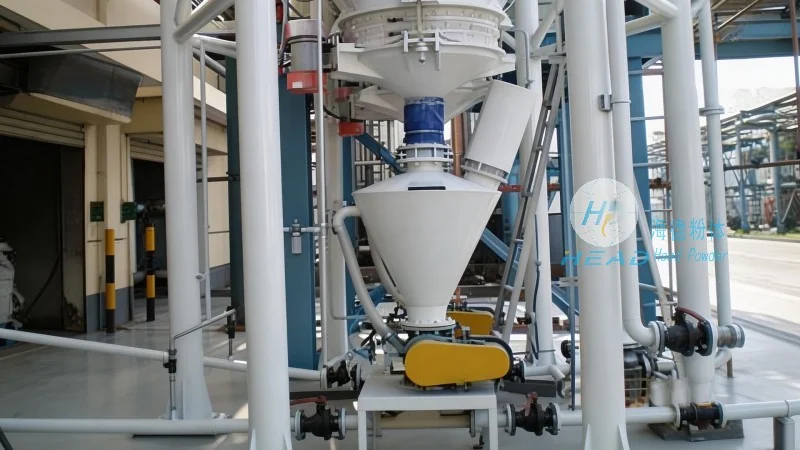
In feed mills, the conveying systems play a crucial role in transporting corn cobs to storage silos or processing units, ensuring a steady supply of raw material for animal feed production. The working environment in these settings is characterized by high humidity and temperature fluctuations, which the system's robust construction and corrosion-resistant materials can withstand. Agricultural storage facilities also benefit from these systems, as they facilitate the movement of corn cobs from fields to storage areas, optimizing space utilization and reducing manual labor.
HeadPowder's corn cobs material conveying systems offer several technical advantages that enhance operational efficiency. The systems are designed with low maintenance requirements, featuring durable components that can withstand the abrasive nature of corn cobs. This reduces downtime and operational costs for the end-user. Additionally, the adjustable speed and direction controls allow for precise control over the material flow, enabling operators to match the conveyor's output with the processing capacity of downstream equipment.
The systems also incorporate advanced monitoring and control features, such as variable frequency drives (VFDs), which adjust the motor speed based on the load, optimizing energy consumption. This not only reduces electricity costs but also extends the lifespan of the motor and other components. Furthermore, the modular design of the conveying systems allows for easy installation and customization, enabling HeadPowder to adapt the system to the specific layout and requirements of each client's facility.
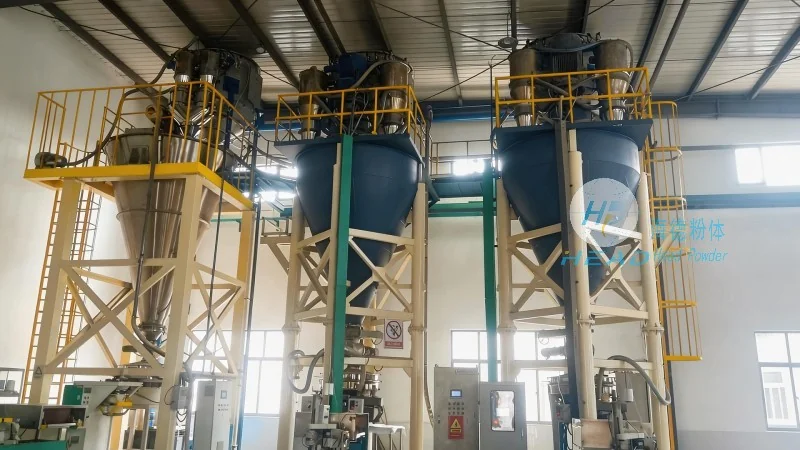
HeadPowder recognizes that each corn processing facility has unique operational needs, which is why their corn cobs material conveying systems are designed with flexibility in mind. The company offers customized solutions that address specific challenges, such as handling large volumes of corn cobs or processing cobs with varying moisture levels. For instance, some systems may include additional cleaning mechanisms to remove debris or dust from the corn cobs before conveyance, ensuring a cleaner feedstock for downstream processes.
Customization also extends to the system's dimensions and capacity. HeadPowder works closely with clients to assess their material handling requirements, including the volume of corn cobs to be processed per hour and the distance the material needs to be transported. Based on this assessment, the company designs a system with the appropriate conveyor width, length, and drive power to meet the client's production goals. This tailored approach ensures that the conveying system operates at peak efficiency, minimizing waste and maximizing productivity.
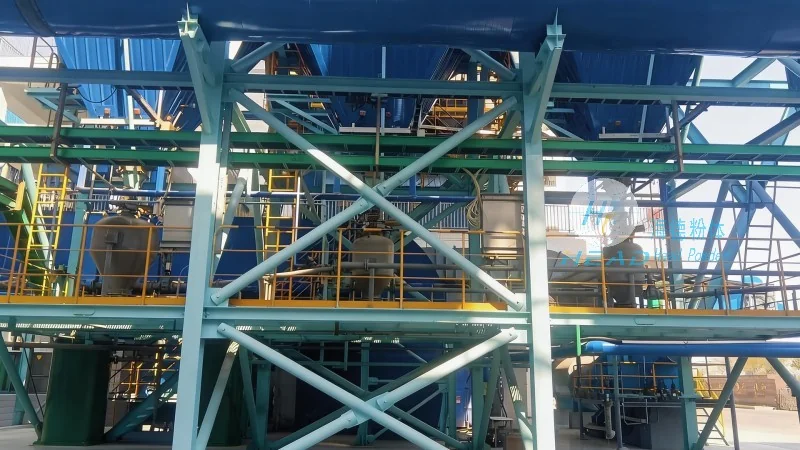
Reliability is a critical factor in industrial material handling, and HeadPowder's corn cobs material conveying systems are built to withstand the rigors of continuous operation. The systems are constructed using high-quality materials, such as stainless steel and heavy-duty plastics, which are resistant to corrosion and wear from the corn cobs. This durability ensures that the system maintains its performance over an extended period, reducing the need for frequent repairs or replacements.
The company's commitment to quality is evident in the rigorous testing and quality control processes applied to each system. Before delivery, the conveying systems undergo comprehensive performance tests to verify that they meet the specified operational parameters. This includes testing the system's load capacity, speed, and material handling efficiency under various conditions. By ensuring that each system is reliable and durable, HeadPowder provides its clients with a long-term solution that enhances their operational efficiency and reduces overall costs.
HeadPowder's corn cobs material conveying systems represent a sophisticated solution for the efficient and reliable transport of corn cobs in industrial settings. By integrating advanced mechanical principles with robust construction and customizable features, these systems address the unique challenges of corn processing and feed production. With a focus on operational efficiency, durability, and client-specific customization, HeadPowder continues to be a trusted partner in providing high-quality material handling solutions to the agricultural and food processing industries. Based in Shandong, China, HeadPowder Engineering Co., Ltd. leverages its expertise and local manufacturing capabilities to deliver systems that meet the evolving needs of its global clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top