Carbonaceous particle material conveying equipment is a specialized system designed to handle and transport carbon-based granular materials efficiently. This equipment plays a crucial role in various industrial applications where the reliable movement of carbon particles is essential for production processes. The design and functionality of such systems are tailored to meet the specific demands of industries dealing with carbonaceous materials, ensuring optimal performance and safety.
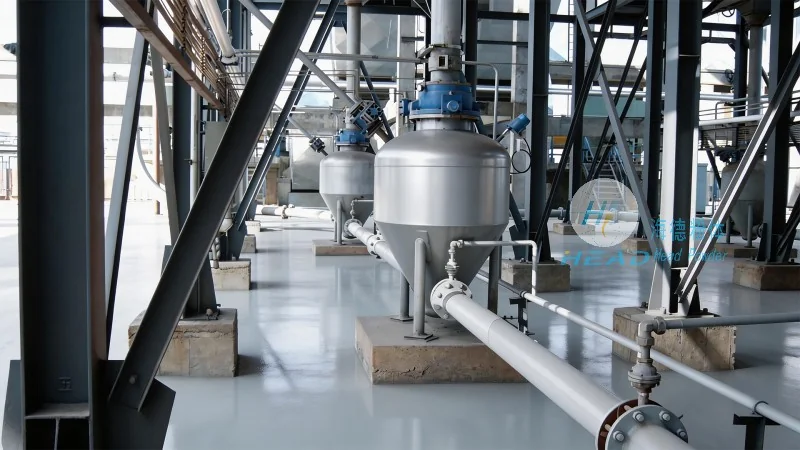
The core principle of carbonaceous particle material conveying equipment revolves around the use of mechanical or pneumatic systems to transport granular carbon materials from one location to another. These systems are engineered to handle materials like carbon black, graphite, and other carbon-based powders or granules. The primary mechanisms include screw conveyors, pneumatic conveyors, and belt conveyors, each offering unique advantages depending on the material characteristics and operational requirements.
Screw conveyors utilize rotating screws to move materials along a tube or trough, providing a continuous and controlled flow. This method is particularly effective for materials that are free-flowing and non-abrasive. Pneumatic conveyors, on the other hand, use air pressure to transport materials through a pipeline, making them suitable for fine powders and materials that are sensitive to mechanical stress. Belt conveyors offer a more straightforward approach, using a moving belt to transport larger granules or bulk materials over longer distances.
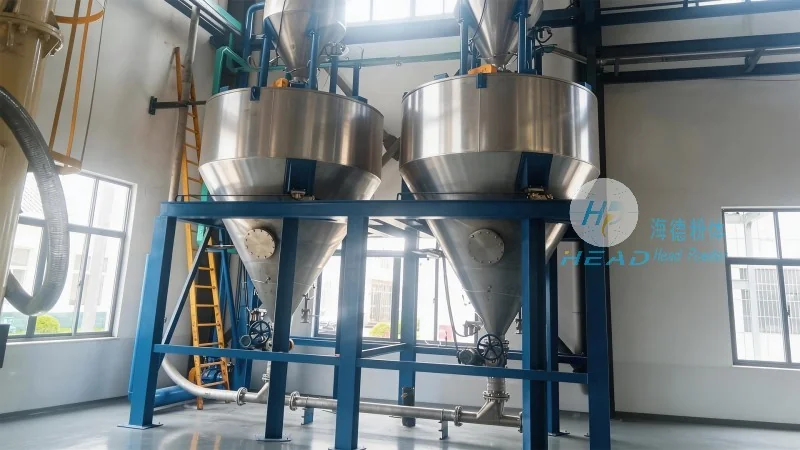
The working scene characteristics of carbonaceous particle material conveying equipment are influenced by several factors, including the type of material being handled, the environment of the operation, and the specific requirements of the industrial process. For instance, in the production of carbon black, the conveying equipment must be capable of handling fine, abrasive particles without causing excessive wear or blockages. This often requires the use of high-quality materials for the conveyor components and robust sealing systems to prevent dust emissions.
In graphite processing facilities, the conveying equipment may need to accommodate materials with varying degrees of moisture content and different particle sizes. The design of the system must ensure that the material is transported without agglomeration or degradation, which could affect the quality of the final product. Additionally, the working environment, such as high temperatures or chemical exposure, may necessitate the use of specialized materials for the conveyor components to maintain durability and performance.
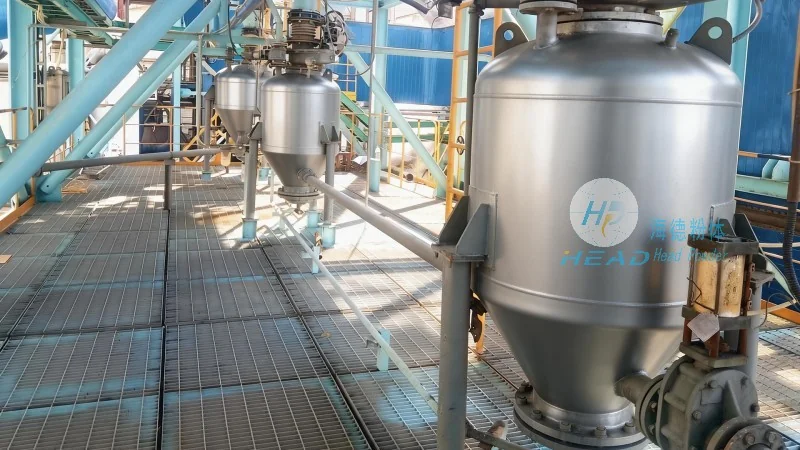
Carbonaceous particle material conveying equipment is widely used in various industrial sectors, including the production of carbon black, graphite, and other carbon-based products. In these applications, the equipment is integrated into production lines to ensure a seamless flow of materials from raw material storage to processing units. The efficiency of the conveying system directly impacts the overall productivity and cost-effectiveness of the operation. For example, in a carbon black manufacturing plant, the conveying equipment must handle large volumes of carbon black powder while maintaining consistent flow rates to avoid bottlenecks in the production process.
Another key aspect is the ability of the conveying equipment to handle different material properties, such as varying particle sizes, moisture content, and bulk density. This adaptability is crucial for maintaining operational efficiency and minimizing downtime. The design of the system often includes features like adjustable speed controls, material feeders, and cleaning mechanisms to address these variations and ensure smooth operation.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of carbonaceous particle material conveying equipment, specializes in providing customized solutions for various industrial needs. With a strong focus on innovation and quality, the company has developed advanced systems that meet the stringent requirements of modern industrial applications. The company's headquarters is located in Shandong, China, where it leverages local resources and expertise to deliver high-performance conveying equipment.
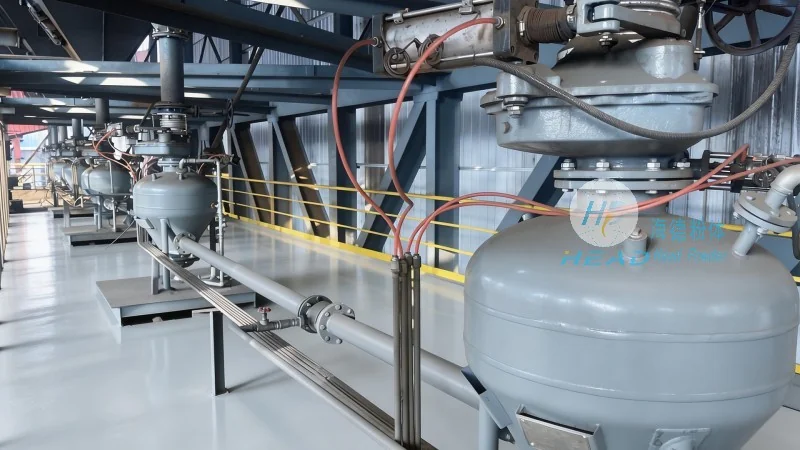
HeadPowder Engineering Co., Ltd. employs a team of experienced engineers and technicians who are dedicated to understanding the unique challenges faced by industries dealing with carbonaceous materials. Through continuous research and development, the company has developed conveyor systems that are not only efficient but also environmentally friendly, reducing dust emissions and improving workplace safety. The company's commitment to customer satisfaction and technical excellence has made it a trusted partner for businesses seeking reliable material handling solutions.
The company's products are designed to be durable, low-maintenance, and cost-effective, providing long-term value to its clients. By incorporating the latest technologies and materials, HeadPowder Engineering Co., Ltd. ensures that its conveying equipment can withstand the harsh conditions of industrial environments while delivering consistent performance. The company's dedication to quality control and customer support has helped it build a strong reputation in the market, making it a preferred choice for businesses in the carbon and graphite industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top