HeadPowder, a leading provider of industrial material handling equipment, specializes in systems designed for the efficient transport of carbon black and coal powder. Based in Shandong, China, the company has established itself as a trusted partner for businesses requiring reliable solutions to manage these fine, abrasive materials. This article explores the core principles behind their material handling systems and the key working scene characteristics that make them suitable for various industrial applications, focusing on the technical aspects and practical implementation of these critical equipment.
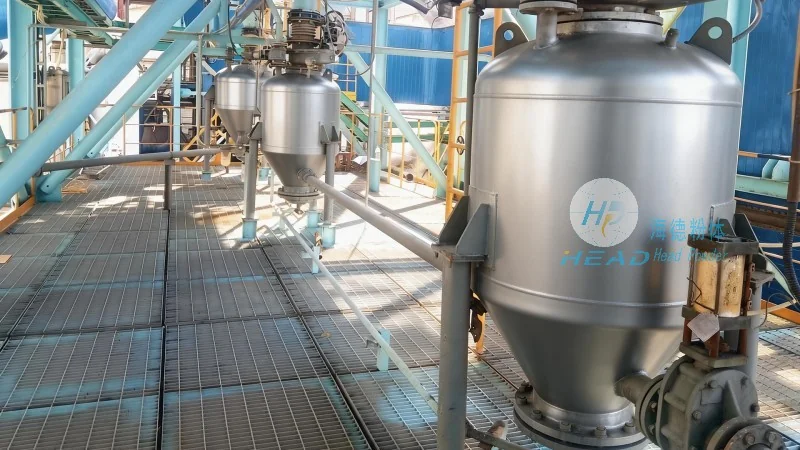
The primary principle of HeadPowder's material handling systems is to ensure safe, efficient, and consistent transport of carbon black and coal powder from storage to processing or packaging areas. These systems are engineered to handle the unique properties of these materials, such as their fine particle size, high density, and potential for dust generation. The design focuses on minimizing material degradation, preventing equipment wear, and maintaining a controlled environment to avoid health and safety risks. Key components typically include feeders, conveyors, and dust control mechanisms, all working in tandem to achieve seamless material flow. The feeders are designed to regulate the flow rate of the material, ensuring a consistent feed to the conveyor system. The conveyors, often using belt or screw mechanisms, transport the material over long distances with minimal loss. Dust control systems, such as baghouses or cyclones, are integrated to capture and filter airborne particles, protecting both the environment and personnel. This integrated approach ensures that the entire system operates smoothly, with each component contributing to the overall efficiency and safety of the material handling process.
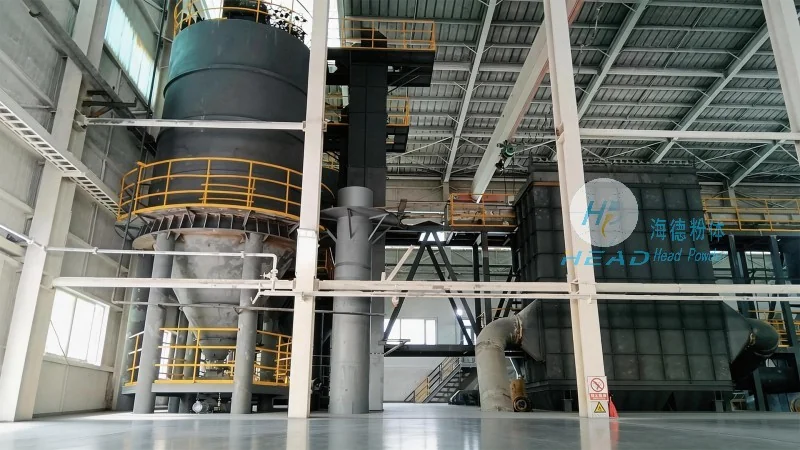
HeadPowder's systems are tailored to meet the demands of diverse industrial environments, each with distinct operational requirements. The working scene characteristics are critical in determining the system's effectiveness and suitability. For instance, in manufacturing plants where carbon black is used as a pigment or coal powder in energy production, the systems must handle high volumes of material while maintaining precision. In such scenarios, the equipment is designed for continuous operation, with features like variable speed drives and robust construction to withstand heavy usage. Additionally, the systems are often integrated with dust collection and filtration systems to comply with environmental regulations and ensure workplace safety. The adaptability of the design allows for customization based on the specific application, whether it's for bulk storage, intermediate handling, or final discharge. For example, in a rubber manufacturing facility, the system might include a hopper for bulk storage, a screw feeder for controlled discharge, and a belt conveyor for transporting the material to the mixing plant. In a coal-fired power plant, the system could involve a silo for coal storage, a pneumatic conveyor for transporting coal powder to the boiler, and a dust collector to manage emissions. These variations highlight how the working scene characteristics dictate the system's configuration, ensuring optimal performance in each specific environment.
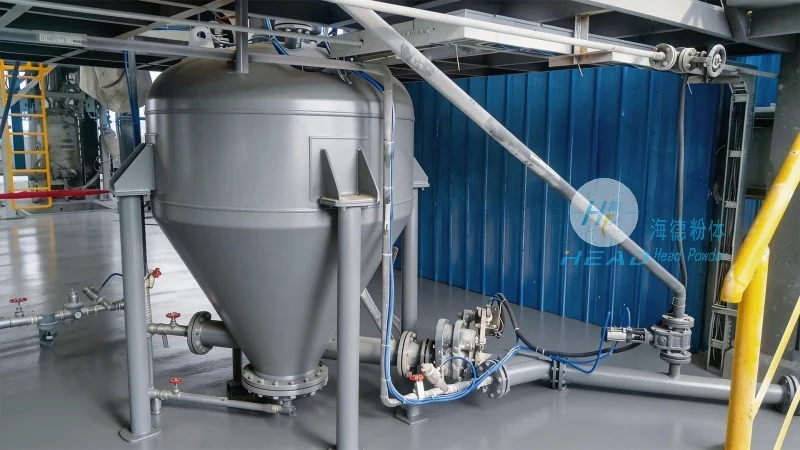
Real-world applications of HeadPowder's material handling systems are evident in industries such as rubber manufacturing, plastics, and power generation. In rubber production, carbon black is a critical additive that enhances the durability and color of products. The systems ensure that the carbon black is delivered to the mixing equipment without clumping or degradation, which is crucial for maintaining product quality. The use of high-quality materials and precise engineering in the feeders and conveyors prevents material agglomeration, ensuring a uniform feed to the mixing process. This leads to consistent product quality and reduced waste. Similarly, in coal-fired power plants, the efficient transport of coal powder to boilers is essential for consistent energy output. The systems in these settings are designed to handle large quantities of material with minimal downtime, contributing to overall operational efficiency. The robust construction of the equipment, including corrosion-resistant components and wear-resistant liners, extends the lifespan of the system and reduces maintenance costs. The integration of monitoring systems allows for real-time tracking of material flow and equipment performance, enabling proactive maintenance and preventing unexpected breakdowns. This focus on operational efficiency and reliability makes HeadPowder's systems a preferred choice for industries where downtime is costly and material quality is paramount.
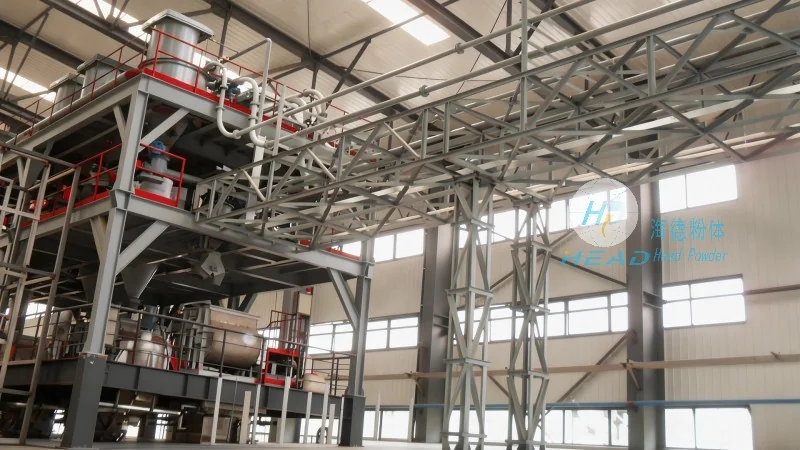
HeadPowder's carbon black and coal powder material handling systems exemplify the company's commitment to providing innovative, reliable solutions for industrial material transport. With a strong presence in Shandong, China, the company leverages its expertise to develop systems that meet the specific needs of its clients. The principles and working scene characteristics discussed highlight the importance of tailored engineering in ensuring the efficiency and safety of material handling processes. By focusing on the unique properties of carbon black and coal powder, HeadPowder continues to deliver systems that enhance productivity and compliance in various industrial sectors. The company's dedication to quality, safety, and customer satisfaction is reflected in the design and implementation of its material handling solutions, making it a trusted partner for businesses seeking to optimize their material transport operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top