Catalyst material handling systems are critical components in industrial processes where catalysts are used, such as in chemical manufacturing, petrochemical plants, and pharmaceutical production. These systems are designed to efficiently transport catalyst powders and granules from storage to reaction units, ensuring consistent and reliable supply for optimal process performance. The design and operation of these systems directly impact the efficiency, safety, and cost-effectiveness of catalyst handling operations.
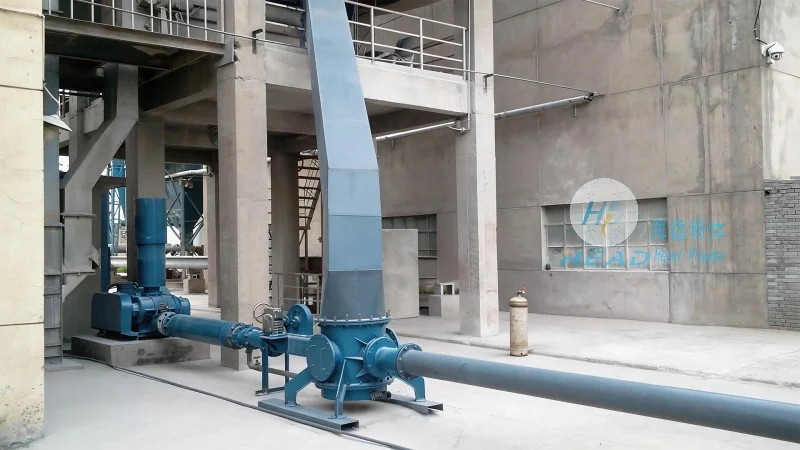
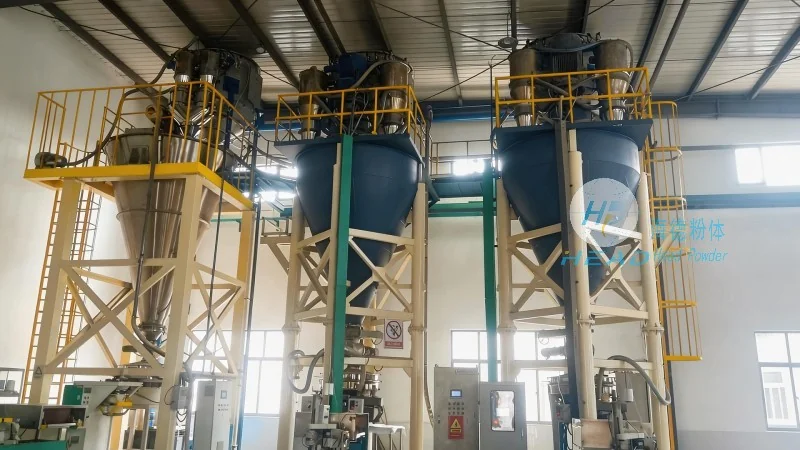
The fundamental principles of catalyst material handling systems revolve around several key aspects. First, the system must maintain the integrity of the catalyst material, preventing contamination, degradation, or agglomeration during transport. This is achieved through specialized equipment like screw conveyors, pneumatic conveyors, and bucket elevators, which are engineered to handle the specific physical properties of catalysts—such as particle size, moisture content, and reactivity. Second, the system must ensure precise control over flow rates and pressure, as catalysts are often sensitive to handling conditions that could affect their activity. Third, safety is paramount, as many catalysts may be hazardous or require controlled environments. The design incorporates features like explosion-proof mechanisms, dust suppression systems, and material flow monitoring to mitigate risks.
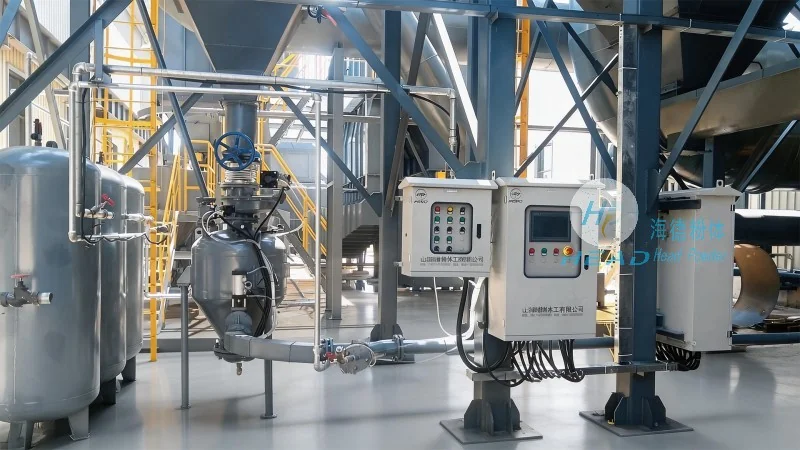
The working scene characteristics of catalyst material handling systems vary significantly based on the specific industrial application. In chemical manufacturing, for example, these systems are often integrated into large-scale production lines where catalysts are used in continuous reaction processes. The systems must handle high volumes of material with minimal downtime, requiring robust and reliable equipment that can operate continuously for extended periods. In petrochemical plants, catalysts are used in processes like hydrocracking and reforming, where the material handling system must be able to handle high temperatures and corrosive environments. The equipment is typically constructed from materials resistant to chemical exposure, such as stainless steel or specialized alloys, to ensure longevity and performance. In pharmaceutical production, the focus is on maintaining high purity and sterility, so the system includes features like closed-loop transport and filtration to prevent contamination. The working scene also includes considerations for space constraints, as plants often have limited room for large equipment, leading to compact and efficient designs that maximize space utilization.
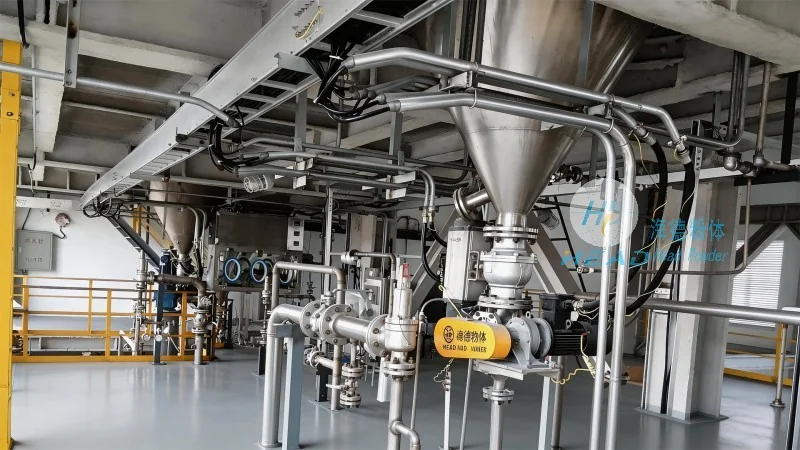
Shandong HeadPowder Engineering Co., Ltd., a leading provider of catalyst material handling solutions, specializes in designing and manufacturing systems tailored to the unique needs of industrial clients. With a focus on innovation and quality, the company has developed a range of equipment that adheres to international standards while meeting the specific requirements of catalyst handling. The company’s headquarters is located in Shandong, China, where it leverages local expertise and resources to deliver comprehensive solutions. HeadPowder Engineering emphasizes customer collaboration, working closely with clients to understand their operational challenges and provide customized solutions that enhance efficiency and safety. The company’s commitment to research and development ensures that its products remain at the forefront of technology, addressing evolving industry demands and improving overall process performance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top