Efficient material handling is a critical component in various industrial processes, particularly in the processing of agricultural byproducts like corn cobs. The principles and working scene characteristics of corn cob material conveying systems are essential for optimizing workflow, ensuring safety, and maximizing operational efficiency. This article explores the fundamental mechanisms behind corn cob material conveying, along with the specific characteristics of different working environments where such systems are applied.
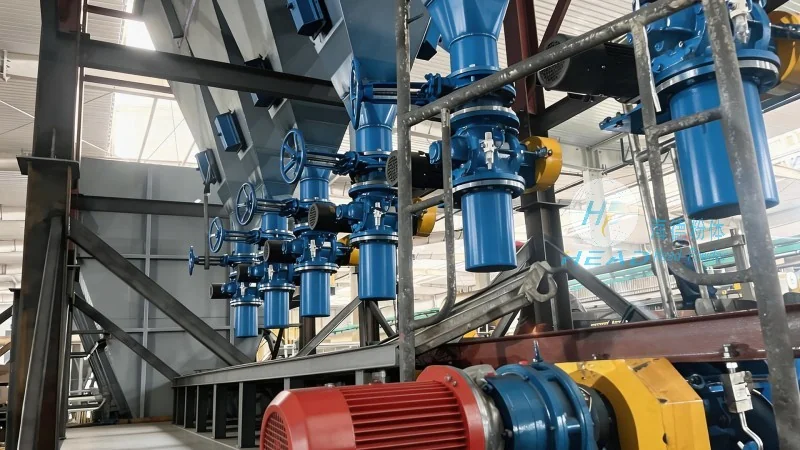
At the heart of corn cob material conveying systems lies a combination of mechanical and gravitational forces designed to transport bulk materials from one location to another. The primary goal is to move corn cobs—often in bulk or as part of a mixed feedstock—throughout processing facilities with minimal energy consumption and maximum reliability. Several key principles underpin these systems, including:
First, the use of specialized equipment such as belt conveyors, screw conveyors, and pneumatic conveyors. Belt conveyors, for instance, utilize a continuous loop of material to carry corn cobs horizontally or at slight inclines, making them ideal for long-distance transport in feed mills or biomass processing plants. Screw conveyors, on the other hand, rely on a rotating helical screw to push materials forward, which is particularly effective for vertical or inclined movement in compact processing areas. Pneumatic conveyors employ air pressure to move corn cobs through a pipeline, offering flexibility in routing but requiring careful control of air pressure and material flow to prevent blockages.
Second, the importance of material properties in determining the most suitable conveying method. Corn cobs are typically dry, lightweight, and irregularly shaped, which influences the choice of equipment. For example, their low density and tendency to create air pockets make pneumatic conveyors less efficient unless equipped with air agitation or pressure boosters. Conversely, their relatively rigid structure allows screw conveyors to handle them without excessive wear, making them a common choice in feed processing where durability is key.
Third, the role of system integration in optimizing conveying efficiency. Modern corn cob material conveying systems often integrate multiple components, such as feed hoppers, material separators, and control panels, to ensure smooth operation. This integration allows for real-time monitoring of material flow rates, pressure levels, and system performance, enabling operators to make adjustments promptly and prevent downtime. For instance, a conveyor system might include a sensor that detects blockages and automatically triggers a reverse cycle to clear the obstruction, reducing the risk of equipment damage and material loss.
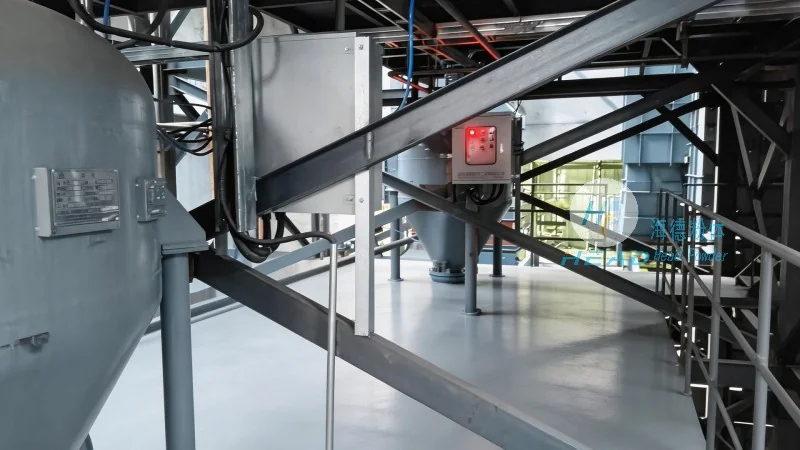
The working scene characteristics of corn cob material conveying systems vary significantly based on the industry and specific application. Understanding these characteristics is crucial for selecting the right equipment and ensuring optimal performance in different environments.
One common working scene is in feed manufacturing facilities, where corn cobs are often processed as part of animal feed. In this environment, the conveying system must handle large volumes of corn cobs and integrate seamlessly with other processing equipment, such as hammer mills or mixers. The key characteristics here include high throughput capacity, durability to withstand abrasive materials, and the ability to maintain consistent material flow rates. For example, a belt conveyor system might be designed to transport corn cobs from a storage silo to a hammer mill, with adjustable speed controls to match the processing capacity of the mill.
Another working scene is in biomass energy production, where corn cobs are used as a fuel source for power generation or heating. In this application, the conveying system must be capable of handling larger, irregularly shaped cobs and transporting them to a boiler or gasifier. The characteristics of such systems include robust construction to handle heavy loads, the ability to operate in harsh outdoor conditions, and the integration of dust control measures to minimize environmental impact. For instance, a screw conveyor might be used to transport corn cobs from a storage pile to a boiler, with a dust collection system attached to capture any airborne particles.
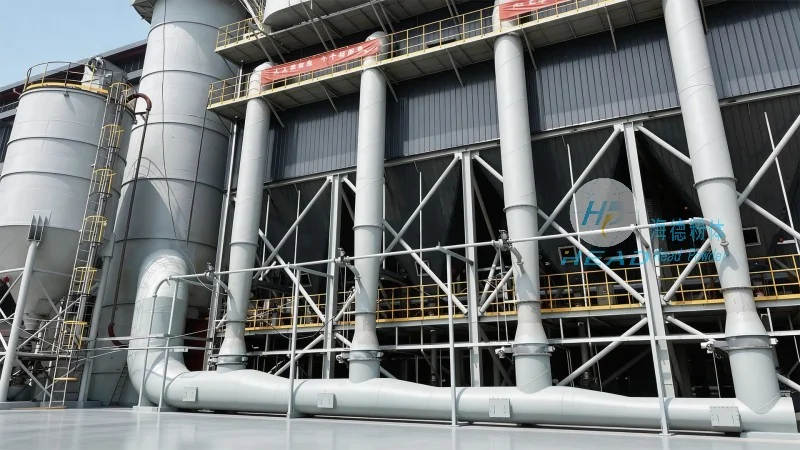
A third working scene is in agricultural processing facilities, where corn cobs are processed for use in bio-based products or as raw materials for other industries. In this environment, the conveying system may need to handle mixed materials, such as corn cobs combined with other agricultural residues, and separate them for further processing. The key characteristics here include flexibility in material handling, the ability to integrate with sorting or cleaning equipment, and the capacity to maintain material purity. For example, a pneumatic conveyor system might be used to transport corn cobs from a cleaning station to a storage bin, with a filter system to remove dust and debris before the material is stored.
Modern corn cob material conveying systems offer several advantages that make them indispensable in industrial applications. These features are designed to enhance efficiency, reduce costs, and improve safety in material handling operations.
First, the ability to handle large volumes of material efficiently. Conveying systems can transport significant quantities of corn cobs in a continuous manner, reducing the need for manual handling and minimizing labor costs. For example, a belt conveyor system can transport up to several tons of corn cobs per hour, depending on the system's design and power capacity. This high throughput capacity is particularly beneficial in feed mills or biomass plants where large-scale processing is required.
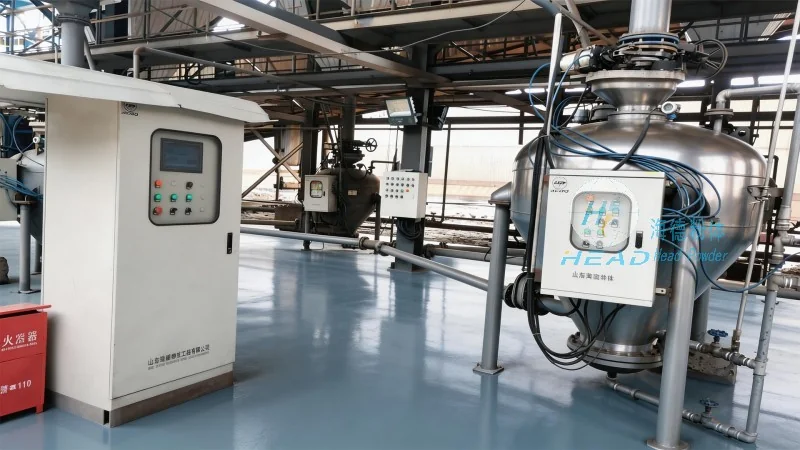
Second, the durability and reliability of the equipment. Corn cob material conveying systems are built to withstand the rigors of industrial use, with components designed to resist wear and tear from abrasive materials. For instance, screw conveyors use hardened steel screws and housing to handle the impact of corn cobs, while belt conveyors employ heavy-duty belts and pulleys to ensure long service life. This durability reduces maintenance costs and downtime, making the systems more cost-effective over their operational lifespan.
Third, the flexibility in system design and integration. Modern conveying systems can be customized to meet the specific needs of different applications, with options for horizontal, vertical, or inclined transport. They can also be integrated with other processing equipment, such as feeders, separators, and control systems, to create a comprehensive material handling solution. This flexibility allows companies to adapt their systems as their operations grow or change, ensuring long-term compatibility and efficiency.
Fourth, the emphasis on safety and environmental compliance. Corn cob material conveying systems are designed with safety features to protect operators and prevent accidents. For example, many systems include emergency stop buttons, safety guards on moving parts, and overload protection mechanisms to prevent equipment damage. Additionally, they often incorporate dust control measures to minimize environmental impact and comply with regulations. These features not only enhance workplace safety but also help companies meet environmental standards and avoid penalties.
Understanding the principles and working scene characteristics of corn cob material conveying systems is essential for optimizing industrial processes and improving operational efficiency. By selecting the right equipment and designing systems that align with specific application requirements, companies can achieve reliable, cost-effective material handling solutions. The key to success lies in considering material properties, system integration, and environmental factors when designing or upgrading conveying systems. As the demand for efficient material handling in agricultural and industrial sectors continues to grow, the importance of well-designed corn cob material conveying systems will only increase. Companies like Shandong HeadPowder Engineering Co., Ltd., based in China, play a vital role in providing advanced conveying solutions tailored to the needs of various industries, ensuring that corn cob material handling remains efficient, safe, and sustainable.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top