Coal ash, a byproduct of coal combustion in thermal power plants, presents significant challenges in handling and transportation due to its fine particle nature and potential environmental impact. The coal ash powder conveying system equipment, developed by Shandong HeadPowder Engineering Co., Ltd. (referred to as HeadPowder), addresses these challenges through advanced engineering solutions designed to ensure efficient, safe, and reliable transport of coal ash from production sites to disposal or utilization locations.
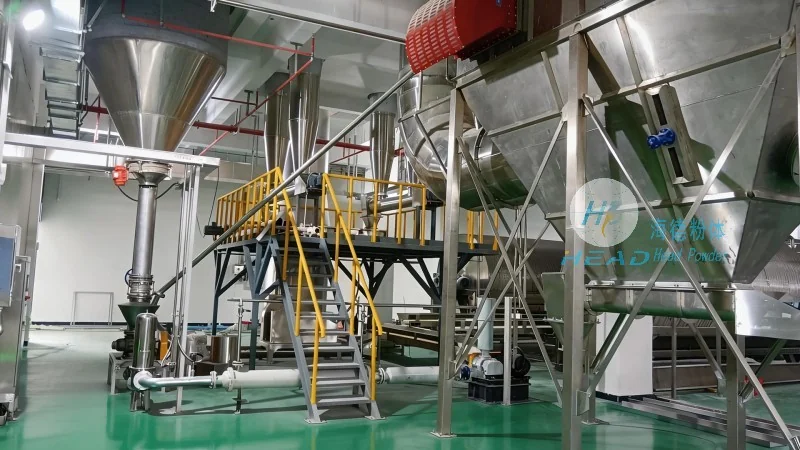
The core principle of the coal ash powder conveying system is based on pneumatic conveying technology, which utilizes air pressure to move fine particulate materials like coal ash through a network of pipes. The system typically operates under negative pressure (suction) or positive pressure (blowing) conditions, depending on the specific application and distance of transport. Key components include ash feeders, air blowers or vacuum pumps, conveying pipelines, and discharge units. The feeders ensure a consistent and controlled flow of coal ash into the system, while the air blowers provide the necessary pressure or vacuum to move the material through the pipes. The conveying pipelines are designed with appropriate diameters and materials to minimize particle segregation and prevent blockages, often incorporating features like bends, valves, and cleaning mechanisms to maintain system efficiency.
The coal ash powder conveying system is deployed in various industrial settings, each with distinct characteristics that influence the system's design and performance. In thermal power plants, the system is commonly used to transport coal ash from the bottom ash hopper or fly ash collection system to storage silos or disposal sites. The working environment in power plants is characterized by high temperatures, dust, and the need for continuous operation, requiring the equipment to be robust, durable, and capable of withstanding harsh conditions. The system's design often includes explosion-proof features and dust collection systems to comply with environmental regulations and ensure workplace safety.
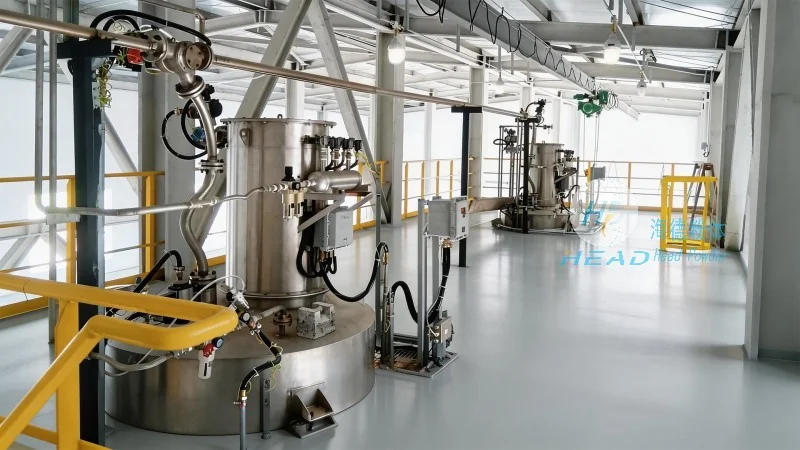
HeadPowder's coal ash powder conveying system is suitable for a range of applications, including: (1) Long-distance transport of coal ash from power plants to off-site disposal facilities or recycling plants, where the system can cover distances of several kilometers while maintaining material integrity. (2) On-site handling within power plant premises, such as moving coal ash from storage silos to processing units for further utilization, like cement production or road construction materials. (3) Integration with other industrial processes, where the system can be connected to downstream equipment to streamline material flow and improve overall plant efficiency. The versatility of the system allows it to adapt to different operational requirements, from small-scale local transport to large-scale industrial applications.
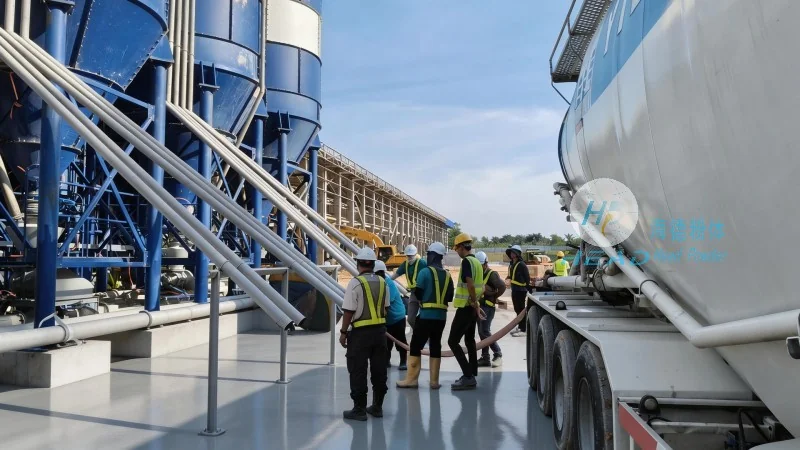
The coal ash powder conveying system from HeadPowder offers several advantages that make it an ideal solution for coal ash management. These include: (1) High efficiency in material transport, with minimal loss of coal ash during the process and reduced labor costs compared to traditional manual handling methods. (2) Low maintenance requirements, as the system is designed with durable components and self-cleaning features that minimize downtime and operational costs. (3) Environmental friendliness, as the system reduces dust emissions and prevents contamination of the surrounding environment, aligning with regulatory standards for industrial waste management. (4) Customization options, allowing the system to be tailored to specific plant layouts, transport distances, and material characteristics, ensuring optimal performance for each application.
Shandong HeadPowder Engineering Co., Ltd. provides advanced coal ash powder conveying system equipment that addresses the unique challenges of handling fine particulate materials in industrial settings. By leveraging pneumatic conveying technology and robust engineering design, the system ensures efficient, safe, and reliable transport of coal ash, supporting the sustainable management of coal ash byproducts and contributing to environmental compliance and operational efficiency in power plants and related industries. The company's commitment to quality and innovation ensures that its conveying systems meet the highest standards of performance and reliability, making them a trusted choice for coal ash handling applications worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top