For industries that rely on efficient and safe bulk powder transport, the negative pressure dilute phase conveying system stands out as a reliable solution. Developed by Shandong HeadPowder Engineering Co., Ltd., a prominent engineering firm based in Shandong, China, this equipment integrates advanced technology to meet the diverse needs of modern manufacturing and processing sectors.
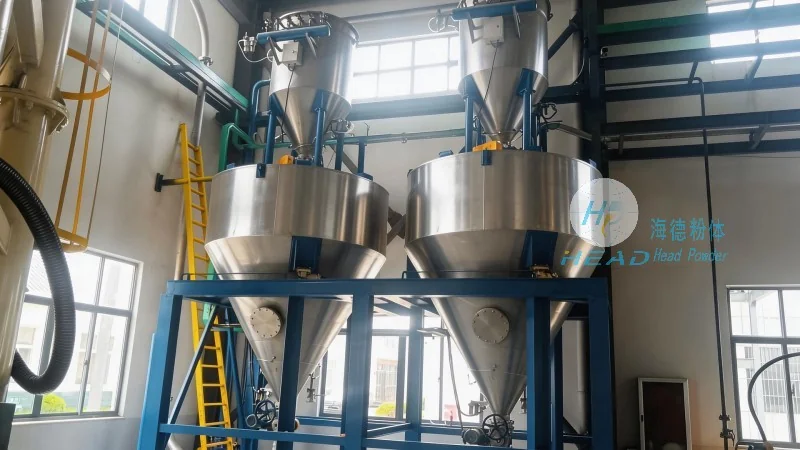
The system operates on the principle of creating a negative pressure zone within the conveying pipeline. By drawing air and powder particles from the source into the pipeline, the equipment uses a vacuum effect to move materials. This approach differs from positive pressure systems, which force material through the line using compressed air. The negative pressure method reduces the risk of dust explosion and minimizes the need for high-pressure components, making it suitable for handling sensitive or abrasive powders. The key is maintaining a consistent airflow rate that ensures the powder particles are entrained and transported smoothly without clogging or degradation.
One of the standout features of this system is its adaptability to various industrial applications. In manufacturing plants, it can efficiently transport raw materials from storage silos to production lines, ensuring a continuous and controlled flow. The system's ability to handle long-distance conveying with minimal maintenance makes it ideal for large-scale operations, such as in the chemical and pharmaceutical industries where precision and reliability are critical. For example, in a pharmaceutical factory, the system can convey active ingredients or excipients without cross-contamination, adhering to stringent quality standards.
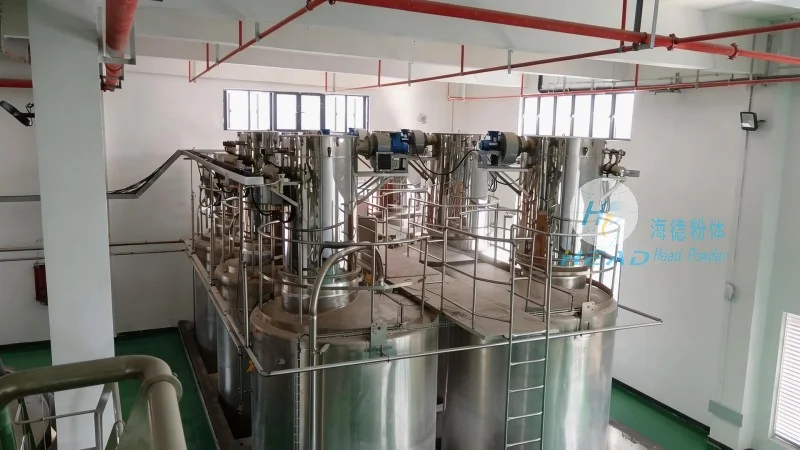
In environmental and waste management, the negative pressure dilute phase conveying system is particularly beneficial. It can effectively transport powders like fly ash or cement from processing facilities to disposal or recycling sites, while complying with strict emission regulations. The system's design allows for easy integration with existing infrastructure, reducing the need for extensive modifications and lowering overall operational costs. This makes it a cost-effective solution for industries seeking to improve their waste handling processes.
Shandong HeadPowder Engineering Co., Ltd. has successfully implemented this technology across a wide range of sectors. In the food processing industry, the system is used to convey flour, powdered milk, or other ingredients without compromising product quality. The negative pressure environment prevents contamination and maintains hygienic conditions, which is essential for food safety regulations. Similarly, in the mining sector, it can transport fine ore powders from crushing stations to storage areas, enhancing operational efficiency and safety by reducing manual handling.
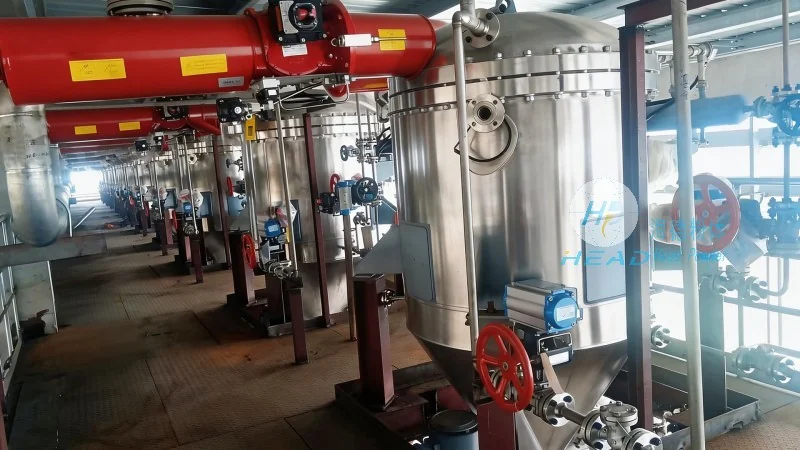
In the construction materials industry, the system is ideal for conveying cement, lime, or other powders to mixing plants or storage silos. The ability to handle high volumes with minimal energy consumption makes it a preferred choice for large-scale construction projects. Additionally, in the chemical industry, it can transport reactive powders safely, as the negative pressure reduces the risk of accidental ignition or explosion.
Compared to traditional positive pressure or dense phase pneumatic conveying systems, the negative pressure dilute phase conveying system offers several advantages. The lower pressure differentials result in reduced energy consumption, leading to significant cost savings over the equipment's lifespan. Furthermore, the system's ability to handle abrasive powders without excessive wear on components extends the lifespan of the equipment and reduces maintenance frequency. Another key benefit is the reduced risk of dust accumulation and explosion, making it safer for environments where powder handling is a regular process.
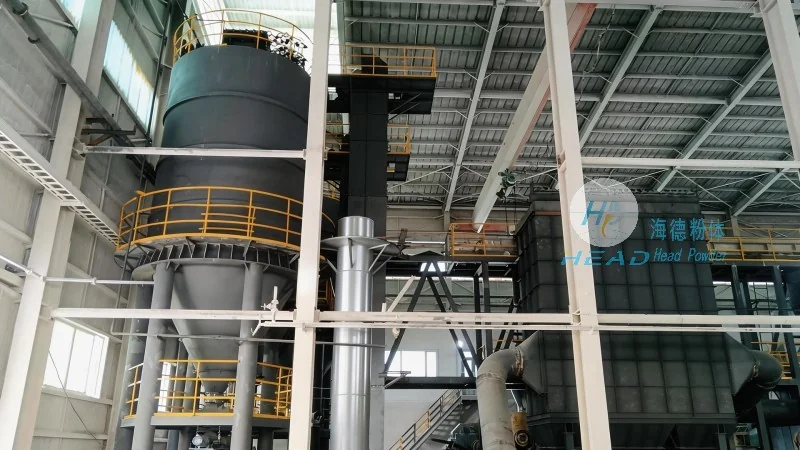
The system's versatility is another major advantage. It can handle a wide range of powder types, from fine powders that require gentle handling to coarse materials that can withstand higher velocities. This flexibility allows industries to use a single system for multiple applications, simplifying inventory management and operational complexity. Additionally, the negative pressure approach minimizes the need for high-pressure air compressors, which are often expensive and require regular maintenance.
For businesses in China and globally, the negative pressure dilute phase powder conveying system by Shandong HeadPowder Engineering Co., Ltd. represents a significant advancement in material handling technology. By combining efficient operation with safety and adaptability, this equipment addresses the challenges of transporting bulk powders while meeting modern industrial standards. As a result, industries can enhance productivity, reduce costs, and improve overall operational efficiency, making it an essential component in contemporary manufacturing and processing environments. With its proven performance and tailored solutions, HeadPowder continues to be a leader in providing reliable and innovative powder handling solutions to meet the evolving needs of global industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top