For industries that require efficient and reliable powder handling, negative pressure dilute phase powder conveying machines have emerged as a critical solution. These systems are designed to transport bulk powders over long distances with minimal pressure differentials, making them ideal for a wide range of applications. In this article, we will explore the fundamental principles behind these machines and the specific working scenarios where they excel.
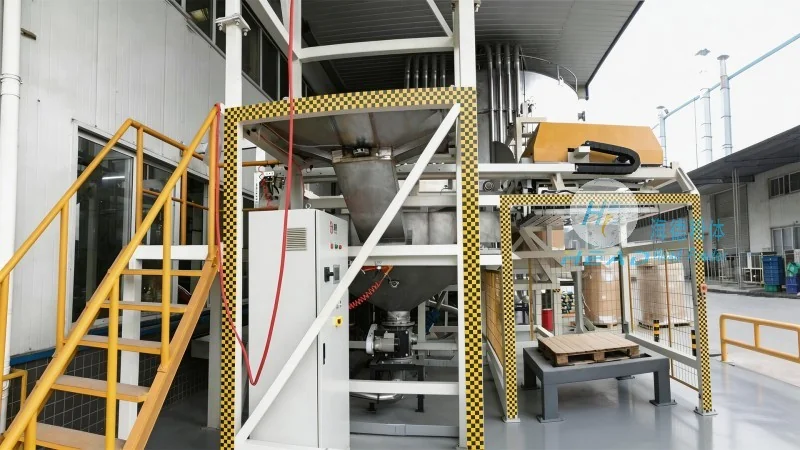
Negative pressure dilute phase powder conveying systems operate by creating a vacuum in the conveying line, which draws the powder particles into the system. The key components include a vacuum pump, a conveying pipe, and a dust collector or filter system. As the vacuum is maintained, the powder is carried through the pipe in a dilute phase, meaning the particles are suspended in air rather than being compacted or compressed. This method minimizes the risk of product degradation and ensures a consistent flow rate.
The principle of operation is based on the creation of a pressure differential between the source of the powder and the receiving end. The vacuum pump generates a low-pressure environment in the conveying line, which pulls the powder particles from the hopper or storage container into the pipe. The air and powder mixture then travels through the pipeline to the destination, where the powder is separated from the air using a cyclone or filter. This separation process allows the powder to be deposited at the target location while the air is either recirculated or vented, depending on the system design.
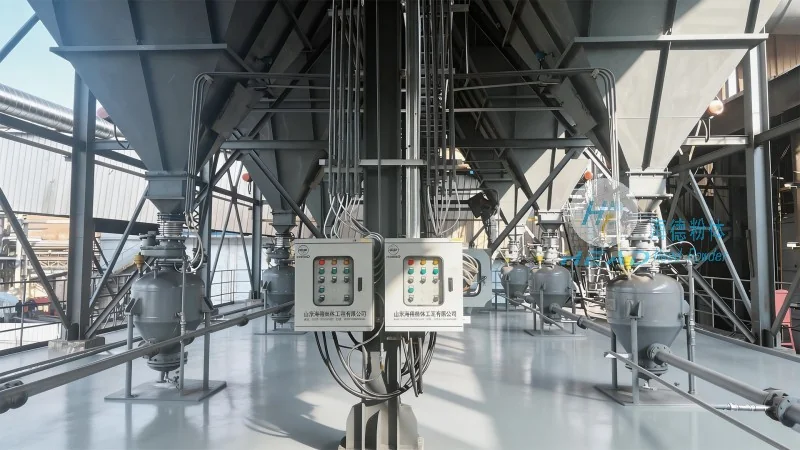
One of the primary advantages of negative pressure dilute phase conveying is its ability to handle a wide variety of powders, including those that are fine, abrasive, or sensitive to moisture. The low pressure and dilute phase operation reduce the risk of particle agglomeration and damage, preserving the quality of the material. Additionally, these systems are energy-efficient compared to positive pressure systems, as they require less power to maintain the vacuum. The compact design also makes them suitable for installation in confined spaces, and the flexible piping allows for easy integration into existing production lines.
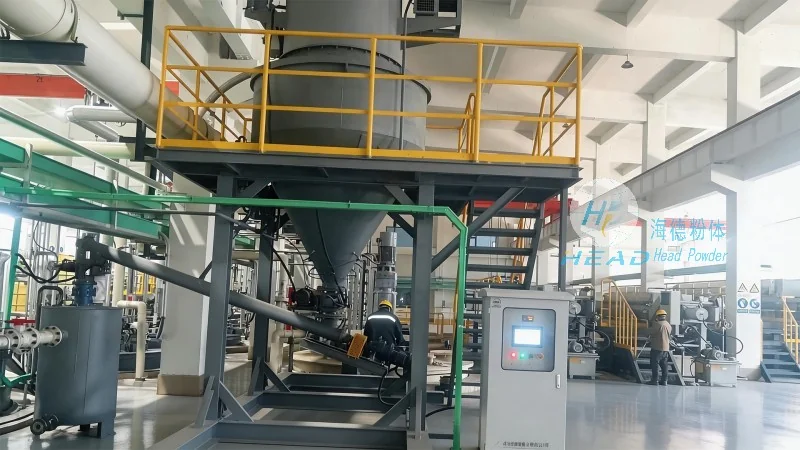
Negative pressure dilute phase powder conveyors are commonly used in industries such as pharmaceuticals, food processing, and chemical manufacturing. In pharmaceutical applications, they are used to transport active ingredients and excipients with high precision, ensuring that the product remains sterile and free from contamination. In the food industry, these systems are employed to handle powders like flour, sugar, and spices, maintaining the quality and freshness of the product. Chemical manufacturers use them to transport raw materials and intermediates, which may be hazardous or reactive, requiring a safe and controlled conveying process.
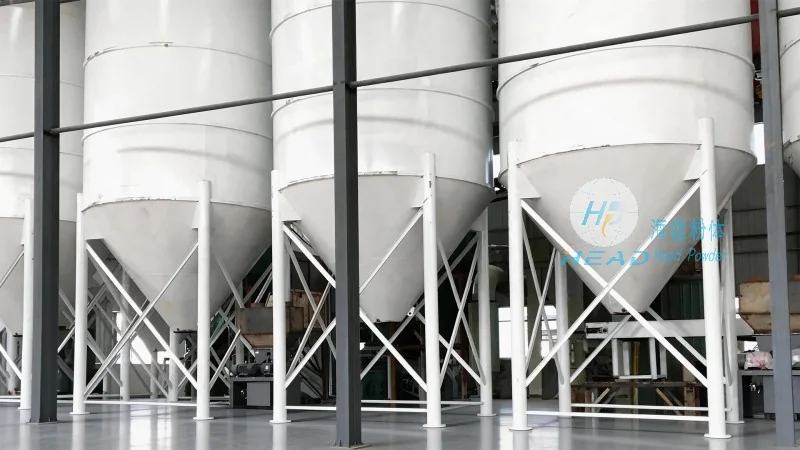
Proper installation of a negative pressure dilute phase powder conveying system is crucial for optimal performance. The system must be designed to handle the specific characteristics of the powder being conveyed, including particle size, density, and moisture content. Regular maintenance is also essential to ensure the system operates efficiently. This includes checking the vacuum pump for proper function, inspecting the filters and cyclones for clogging, and cleaning the conveying line to prevent buildup. By following these maintenance procedures, the system can achieve long-term reliability and minimize downtime.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of powder handling equipment based in Shandong, China. With years of experience in the industry, HeadPowder specializes in designing and manufacturing high-quality negative pressure dilute phase powder conveying systems tailored to the needs of various industries. The company's commitment to innovation and quality has made it a trusted partner for businesses seeking reliable and efficient powder transport solutions. HeadPowder's products are known for their durability, energy efficiency, and ease of maintenance, making them a preferred choice for companies worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top