HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of efficient corn powder conveying systems. This article explores the fundamental principles behind these systems and highlights key characteristics of their operational environments.
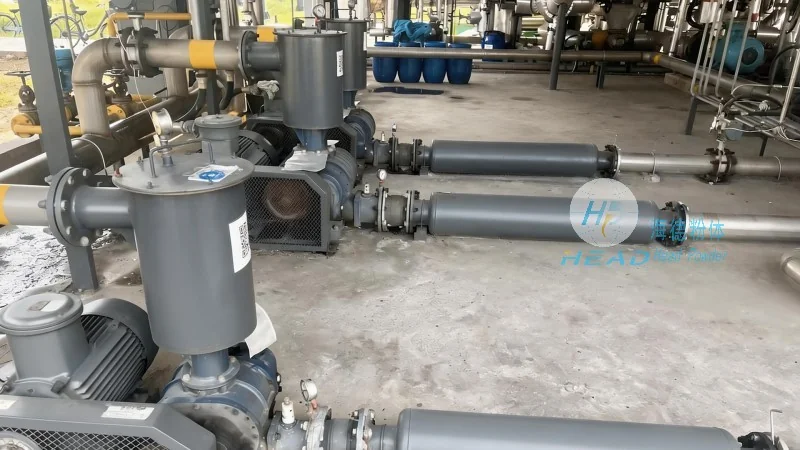
Corn powder conveying lines are engineered to transport bulk corn powder from one location to another with precision and efficiency. The primary principle involves utilizing mechanical or pneumatic forces to move the powder through a network of pipes, hoppers, and other components. For instance, pneumatic conveying systems employ compressed air to create a flow that propels the powder, while mechanical systems like screw conveyors use rotating screws to push the material forward. These mechanisms ensure consistent and reliable movement, minimizing product degradation and spillage.
The operational environments for corn powder conveying lines vary based on the application, but several common characteristics define their performance and suitability. One critical aspect is the need for dust control, as corn powder is often fine and can create airborne particles. Conveying systems are typically equipped with dust collection and filtration systems to maintain air quality and comply with safety regulations. Another key characteristic is the requirement for hygienic design, especially in food processing facilities where corn powder is used as an ingredient. Components such as stainless steel construction, smooth surfaces, and easy-to-clean features are standard to prevent contamination and ensure product safety.
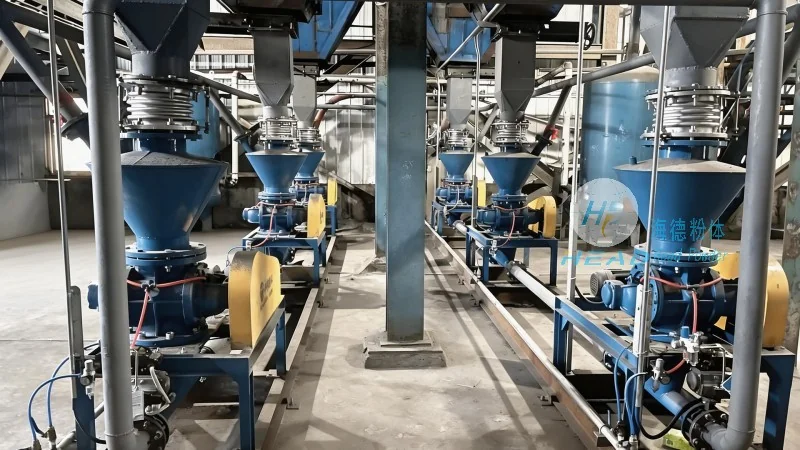
The versatility of corn powder conveying lines makes them suitable for a wide range of industrial applications. In the food industry, these systems are commonly used in corn milling plants, where they transport raw corn kernels into processing units and then move the resulting flour or meal to storage areas. The ability to handle fine powders without clogging is particularly important in these settings, as even minor blockages can disrupt production. In agricultural storage facilities, conveying lines are employed to transfer harvested corn from silos to processing centers, ensuring efficient inventory management and reducing manual handling risks. Additionally, in chemical and pharmaceutical sectors, where corn powder may be used as a raw material, the systems must meet stringent quality and purity standards, further emphasizing the importance of reliable and clean conveying processes.
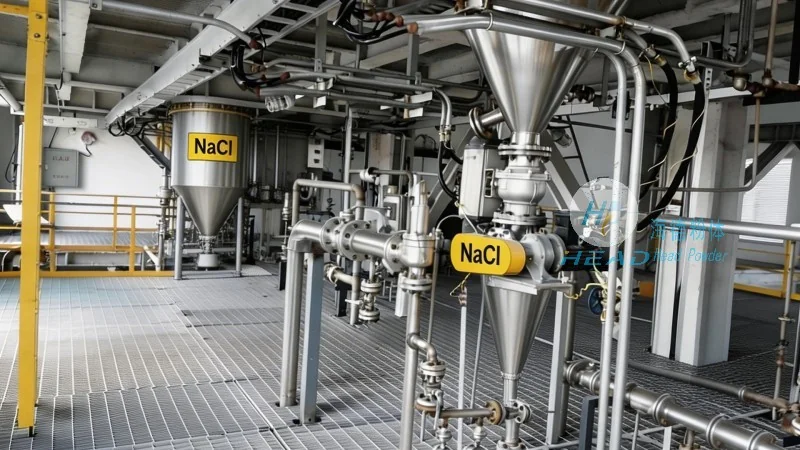
Efficiency is a paramount concern in corn powder conveying line operations. The design of the system, including the type of conveyor, pipe diameter, and air pressure (in pneumatic systems), directly impacts the flow rate and energy consumption. Optimized systems minimize energy waste while maximizing throughput, which is crucial for cost-effective operations. Regular maintenance is also essential to ensure long-term performance. This includes checking for wear and tear on components like screws, seals, and filters, as well as monitoring air pressure and flow rates. Proper maintenance not only extends the lifespan of the equipment but also prevents unexpected downtime, which can impact production schedules and overall productivity.
HeadPowder's corn powder conveying lines are engineered to meet the diverse needs of industrial applications, combining advanced principles with robust design. By understanding the core principles and operational characteristics of these systems, businesses can select the most suitable solution for their specific requirements, ensuring efficient, safe, and reliable corn powder handling. With a commitment to quality and innovation, HeadPowder continues to provide reliable solutions for the corn processing industry, supporting its clients in achieving optimal operational performance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top