Calcined ash, a byproduct from industrial processes such as cement production and metal smelting, requires efficient and reliable transportation methods for handling and utilization. The pneumatic conveying system offers a solution that combines technology and practicality, enabling the safe and effective movement of calcined ash from source to destination. This article, presented by Shandong HeadPowder Engineering Co., Ltd. (headpowder), explores the fundamental principles behind such systems and highlights the key working scene characteristics that make them suitable for various industrial applications.
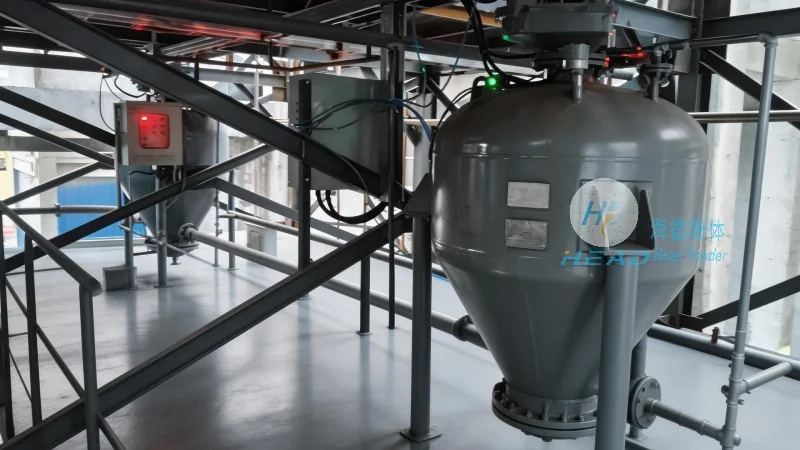
The core mechanism of a calcined ash pneumatic conveying system involves the use of air as the conveying medium to transport particulate materials. The system typically consists of a hopper for material storage, a conveyor line, and a receiver for the delivered material. As material is fed into the hopper, it is drawn into the conveyor line by a fan or blower that generates a high-velocity airflow. The air and ash mixture travels through the pipeline, with the ash particles suspended in the air stream. The receiver at the end of the line collects the ash as the air is filtered and discharged. The system operates based on the principle of fluidization, where the air flow maintains the ash particles in a suspended state, preventing clogging and ensuring smooth transport.
The working scene characteristics of calcined ash pneumatic conveying systems are tailored to meet the demands of industrial environments. These include: 1. **Material Handling Efficiency**: The system can handle large volumes of calcined ash with minimal downtime, ensuring continuous operation. 2. **Space Optimization**: Pneumatic conveying systems are compact and can be installed in confined spaces, making them suitable for facilities with limited floor area. 3. **Environmental Protection**: The enclosed pipeline design minimizes dust emissions, reducing the impact on the surrounding environment and complying with industrial regulations. 4. **Flexibility in Layout**: The system can be configured to follow the existing layout of the industrial site, allowing for easy integration with other equipment and processes. 5. **Safety and Reliability**: The use of sealed pipelines and controlled airflow reduces the risk of material spillage and dust explosions, enhancing workplace safety.
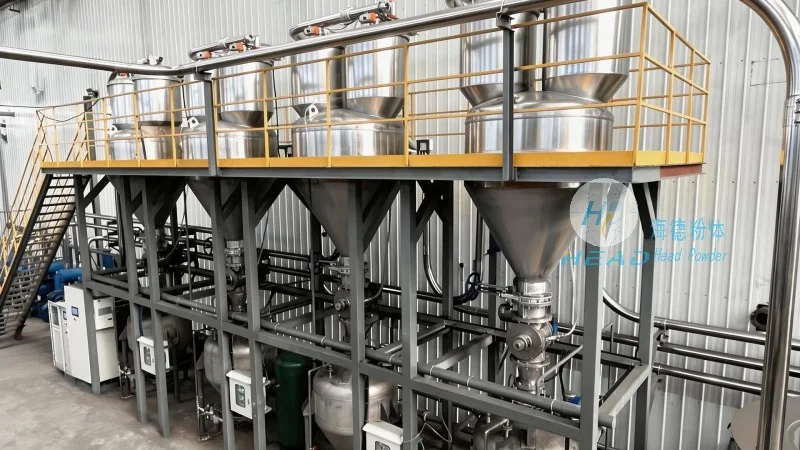
Calcined ash pneumatic conveying systems are widely used in various industrial sectors. In the cement industry, they are employed to transport calcined ash from the calcination kiln to the raw material storage or clinker production areas. In metal smelting, the system helps in moving ash from the furnace to disposal or recycling facilities. Additionally, in power plants, the system can be used to convey ash from the boiler to the ash handling system. The versatility of the system makes it adaptable to different production scales and operational requirements.
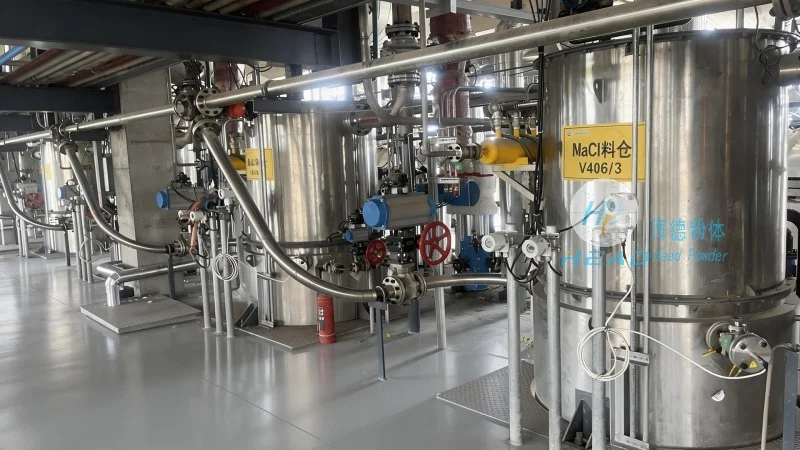
Implementing a pneumatic conveying system for calcined ash offers several advantages over traditional methods such as belt conveyors or bucket elevators. Firstly, it eliminates the need for physical contact between the ash and the conveyor components, reducing wear and tear and extending the system's lifespan. Secondly, the enclosed design prevents dust contamination, which is crucial for maintaining product quality and compliance with health and safety standards. Thirdly, the system provides better control over the material flow rate, allowing for precise dosing and integration with other processes. Lastly, the energy efficiency of pneumatic conveying, especially with modern fan technologies, reduces operational costs and environmental impact.
Calcined ash pneumatic conveying systems represent a sophisticated solution for the efficient handling of industrial byproducts. By leveraging the principles of fluidization and controlled airflow, these systems offer reliable, safe, and environmentally friendly transportation solutions. The working scene characteristics, including efficiency, space optimization, and flexibility, make them suitable for a wide range of industrial applications. As industries continue to seek sustainable and effective material handling methods, the adoption of pneumatic conveying systems for calcined ash is likely to increase, contributing to improved operational performance and environmental compliance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top