For industries dealing with rare earth ore powders, efficient material handling is crucial to ensure smooth production processes and maintain operational efficiency. Pneumatic conveying systems have emerged as a key technology in this sector, offering a reliable method to transport fine powders like rare earth ores. This article explores the fundamental principles of rare earth ore powder pneumatic conveying and highlights the key characteristics of its working scenes, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field.
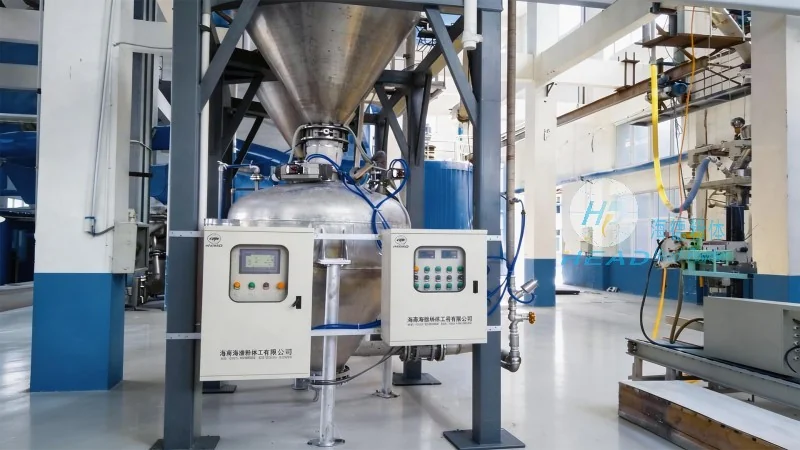
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials, including fine powders, through a pipeline using air or gas as the conveying medium. In the context of rare earth ore processing, this technology is particularly valuable due to the sensitivity of these materials to moisture, contamination, and degradation during handling. The core principle involves creating a flow of air within a pipeline that lifts and transports the ore powder particles. There are two primary types of pneumatic conveying systems: suction (or vacuum) systems and pressure systems. Suction systems use a vacuum to draw material from a source, such as a hopper or storage bin, into the pipeline. Pressure systems, on the other hand, use compressed air to push material through the pipeline. Both systems rely on the interaction between the air flow and the ore particles to achieve efficient transport.
The effectiveness of a pneumatic conveying system for rare earth ore powders depends on several critical components. The main elements include a blower or fan to generate the air flow, a pipeline network to guide the material, a hopper or feeder to introduce the ore powder, and a separator or cyclone to separate the material from the air at the discharge point. Additionally, filters are often incorporated to capture any fine particles that may escape the system, ensuring environmental compliance and product purity. The design of these components must consider the specific properties of rare earth ores, such as their particle size, density, and moisture content, to optimize performance and prevent system blockages or inefficiencies.
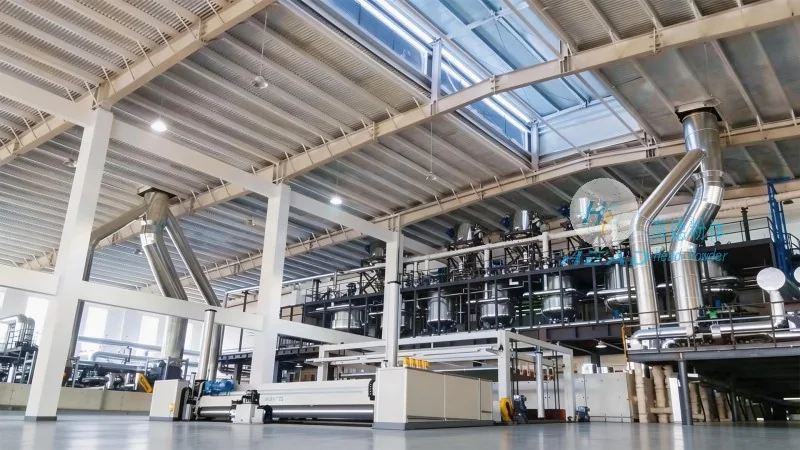
The working scenes where pneumatic conveying systems are applied in rare earth ore processing vary widely, each presenting unique challenges and requirements. One common scenario is in mining operations, where ore is extracted from underground or open-pit mines and transported to processing facilities. Here, the system must handle large volumes of ore powder and operate in harsh, dust-prone environments. Another typical application is in the processing plant itself, where the ore is crushed, ground, and separated into different grades. Pneumatic conveying is used to move the ground ore between various processing stages, such as magnetic separation, flotation, or chemical leaching. The key characteristics of these working scenes include high throughput requirements, the need for dust control, and the ability to handle abrasive or corrosive materials. Additionally, the systems must be designed for easy maintenance and cleaning to prevent contamination and ensure consistent product quality.
Compared to traditional methods like belt conveyors or bucket elevators, pneumatic conveying offers several advantages in the handling of rare earth ore powders. One of the most significant benefits is the reduction of dust generation and exposure, which is critical for worker safety and environmental compliance. The enclosed pipeline system prevents dust from escaping into the air, minimizing the risk of inhalation and contamination of the surrounding environment. Furthermore, pneumatic conveying systems can operate at higher speeds and with lower energy consumption compared to mechanical systems, leading to cost savings and improved efficiency. The ability to handle fine powders without segregation or degradation also enhances the quality of the final product, which is essential for the high-value applications of rare earth elements.
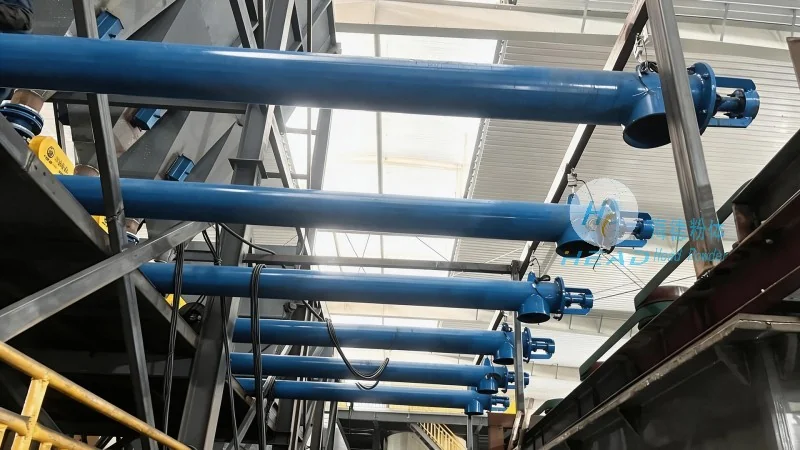
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, is a prominent manufacturer and supplier of pneumatic conveying systems tailored for rare earth ore processing. With years of experience in the industry, the company specializes in designing and implementing customized solutions that meet the specific needs of its clients. HeadPowder's expertise lies in understanding the unique challenges of rare earth ore powders, such as their fine particle size and potential for agglomeration, and developing systems that address these issues effectively. The company's products are engineered to provide high reliability, low maintenance, and optimal performance, ensuring that clients can achieve their production goals efficiently and sustainably. By leveraging advanced technology and a deep understanding of material handling, HeadPowder has established itself as a trusted partner in the rare earth ore processing sector.
In conclusion, pneumatic conveying systems play a vital role in the efficient and safe handling of rare earth ore powders. The principles of air-based transport, combined with specialized system design, enable industries to process these valuable materials with minimal loss and maximum efficiency. The working scene characteristics, such as high throughput and environmental considerations, make pneumatic conveying an ideal choice for modern rare earth ore processing facilities. As a leader in the field, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide solutions that meet the evolving needs of the industry, ensuring that rare earth ore processing remains a sustainable and profitable endeavor.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top