For industrial applications requiring the efficient transport of bulk powder materials, pneumatic conveying systems offer a reliable and versatile solution. This article explores the working principle and key characteristics of powder material pneumatic conveyors, providing insights into their operational mechanics and practical benefits.
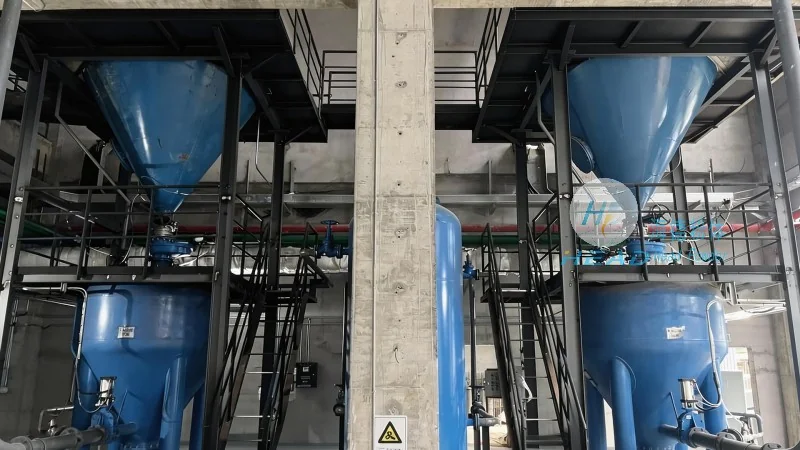
Pneumatic conveying equipment, commonly known as powder material pneumatic conveyors, is a technology used to transport dry bulk materials through a pipeline using air or other gas as the conveying medium. These systems are widely employed in industries such as food processing, pharmaceuticals, chemicals, and mining, where the need to handle fine powders without contamination or degradation is critical. The equipment is designed to ensure safe, efficient, and cost-effective material transfer, addressing challenges like dust control, material segregation, and system flexibility.
The core working principle of a pneumatic conveyor involves the creation of a pressure differential within the conveying pipeline. Air is introduced into the system, either by a positive pressure blower or a vacuum pump, to generate the necessary force for material movement. In positive pressure systems, air is forced into the pipeline, pushing the powder forward. In contrast, negative pressure systems use a vacuum to draw the material into the pipeline. The powder is typically fed into the system via a hopper or feeder, where it is mixed with the air stream. As the mixture travels through the pipeline, the air provides the kinetic energy required to move the powder particles, ensuring consistent and controlled transport. The system may include components like in-line mixers, cyclones for separation, and filters to maintain material purity and system efficiency.
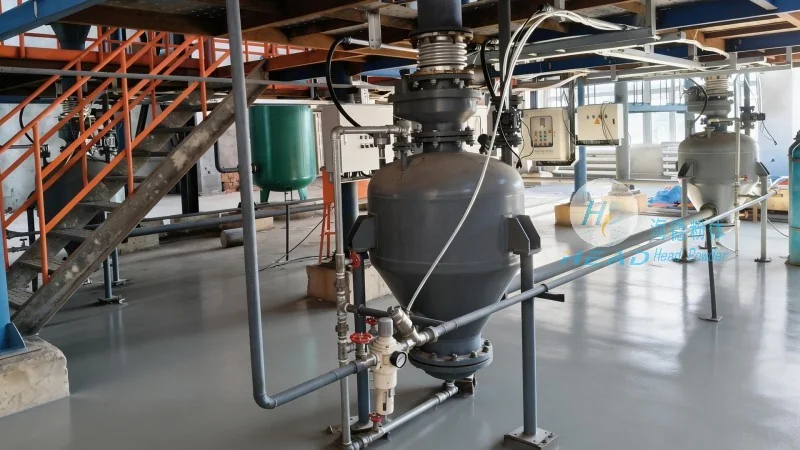
Powder material pneumatic conveyors offer several distinct advantages that make them preferable for many industrial applications. One of the primary benefits is the ability to handle fine and abrasive powders without the need for mechanical components that could cause wear or contamination. The enclosed pipeline system also provides excellent dust control, reducing environmental impact and improving workplace safety. Additionally, these systems are highly flexible, allowing for changes in material flow rates and pipeline layout with minimal modifications. They can transport materials over long distances and through complex layouts, including vertical lifts and horizontal turns, with consistent performance. The technology also enables gentle handling of sensitive materials, preserving their quality and preventing agglomeration or degradation. Furthermore, pneumatic conveying systems are generally low maintenance, as they have fewer moving parts compared to mechanical conveyors, reducing downtime and operational costs.
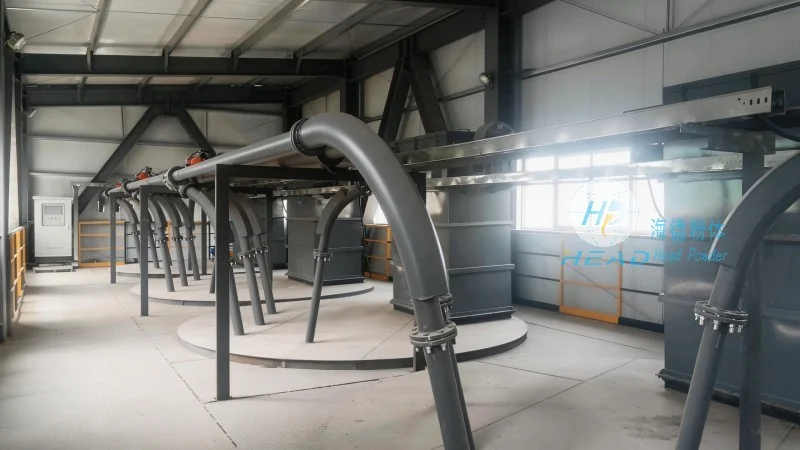
The versatility of powder material pneumatic conveyors makes them suitable for a wide range of applications. In the food industry, they are used to transport ingredients like flour, sugar, and spices, ensuring hygienic and contamination-free handling. In pharmaceutical manufacturing, the systems are employed to move active pharmaceutical ingredients (APIs) and excipients, maintaining strict purity standards. Chemical manufacturers utilize pneumatic conveyors for handling powders such as pigments, catalysts, and specialty chemicals, where precise control over material flow is essential. Mining and mineral processing industries also benefit from these systems for transporting ore powders and tailings. When selecting a pneumatic conveying system, several factors must be considered, including the type of material (e.g., dustiness, abrasiveness, moisture content), the required transport distance, and the desired flow rate. The choice between positive and negative pressure systems, as well as the design of the pipeline and feeding mechanisms, will depend on these specific operational requirements to ensure optimal performance and efficiency.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of powder handling equipment, specializes in the design, manufacturing, and supply of high-quality pneumatic conveying systems. With a focus on innovation and customer satisfaction, the company provides tailored solutions to meet the diverse needs of industrial clients. HeadPowder's products are engineered to deliver reliable performance, ensuring efficient material transport while maintaining the highest standards of safety and environmental compliance. The company's commitment to quality and technical expertise makes it a trusted partner for businesses seeking advanced powder handling solutions. Located in Shandong, China, HeadPowder leverages its local resources and industry knowledge to deliver robust and cost-effective equipment that enhances operational efficiency and productivity in various industrial sectors.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top