Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in the design and implementation of advanced pneumatic conveying systems tailored for phenolic powder handling. This article delves into the fundamental working principles and key characteristics of such systems, providing a comprehensive overview for industry professionals seeking efficient material transport solutions.
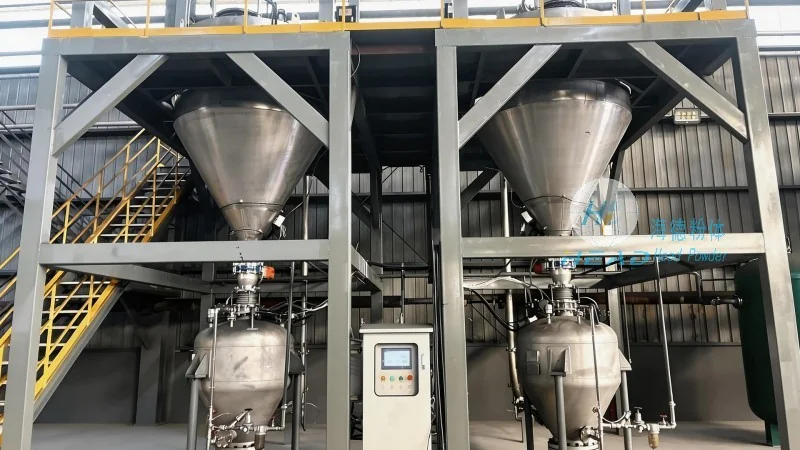
The core mechanism of a pneumatic conveying system involves the use of compressed air to transport bulk materials like phenolic powder through a pipeline network. The process typically begins with the material being introduced into a hopper or feeder, where it is then drawn into the conveying line by the pressure differential created by the air flow. Compressed air, often generated by a blower or compressor, moves the powder particles along the pipeline, ensuring a continuous and controlled flow. The system may employ different modes of operation, such as dilute phase or dense phase conveying, depending on the material characteristics and application requirements. Dilute phase systems use higher air velocities to keep particles suspended, while dense phase systems employ lower velocities and higher air pressure to maintain a more compact flow, reducing the risk of particle degradation or blockages.
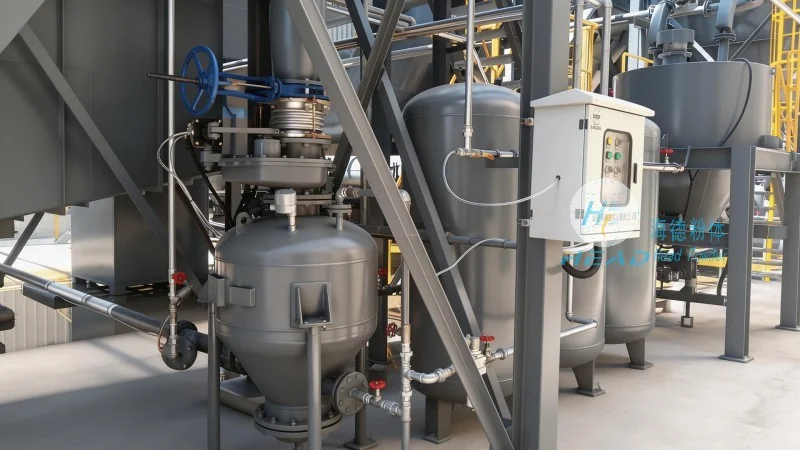
Phenolic powder pneumatic conveying systems offer several distinct advantages that make them ideal for industrial applications. Firstly, they provide a dust-free and enclosed transport environment, which is crucial for maintaining product quality and ensuring workplace safety. Unlike traditional mechanical conveying methods, which can generate significant dust and cause contamination, pneumatic systems keep the material contained within the pipeline, minimizing exposure to the air and reducing the risk of inhalation hazards. Secondly, these systems are highly flexible and can be easily integrated into existing production lines, allowing for seamless material transfer between different processing stages. The modular design of the equipment enables customization to suit specific operational needs, such as varying material flow rates or pipeline lengths. Additionally, pneumatic conveying systems are capable of handling a wide range of particle sizes and shapes, including fine powders like phenolic powder, without the need for additional processing steps. This adaptability makes them suitable for diverse applications, from manufacturing to packaging. Another notable feature is the energy efficiency of modern pneumatic systems, which utilize advanced blower technologies to optimize air usage and reduce operational costs. By minimizing energy consumption while maintaining high transport efficiency, these systems contribute to sustainable industrial practices.
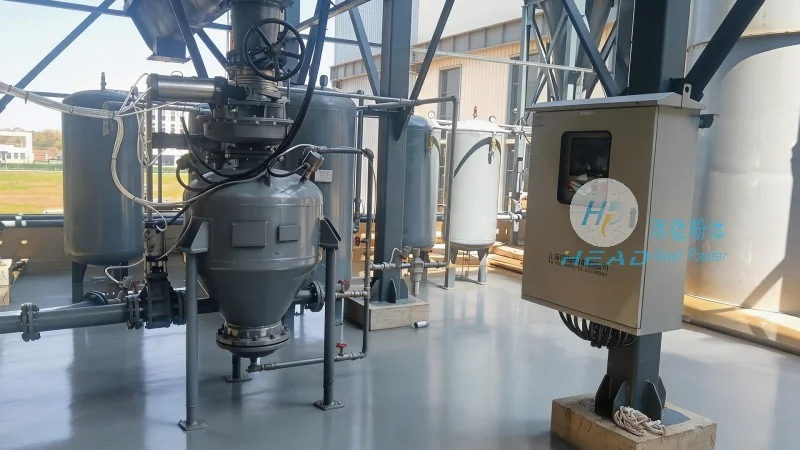
In industrial settings, phenolic powder pneumatic conveying systems are widely used in various sectors, including the chemical, pharmaceutical, and food industries. For instance, in the chemical manufacturing sector, these systems facilitate the transport of phenolic powders from storage silos to processing equipment, ensuring a consistent supply of raw materials. The enclosed nature of the system prevents cross-contamination and maintains the purity of the powder, which is critical for producing high-quality end products. In the pharmaceutical industry, where product safety and regulatory compliance are paramount, pneumatic conveying systems offer a hygienic and controlled method of material handling, reducing the risk of contamination and ensuring adherence to industry standards. The ability to handle fine powders without agglomeration or degradation also enhances the overall quality of the final product. Furthermore, the flexibility of the system allows for easy adjustments to accommodate changes in production volume or material specifications, providing operational flexibility that is essential in dynamic industrial environments. Overall, the combination of efficiency, safety, and adaptability makes phenolic powder pneumatic conveying systems a preferred choice for industries requiring reliable and effective material transport solutions.
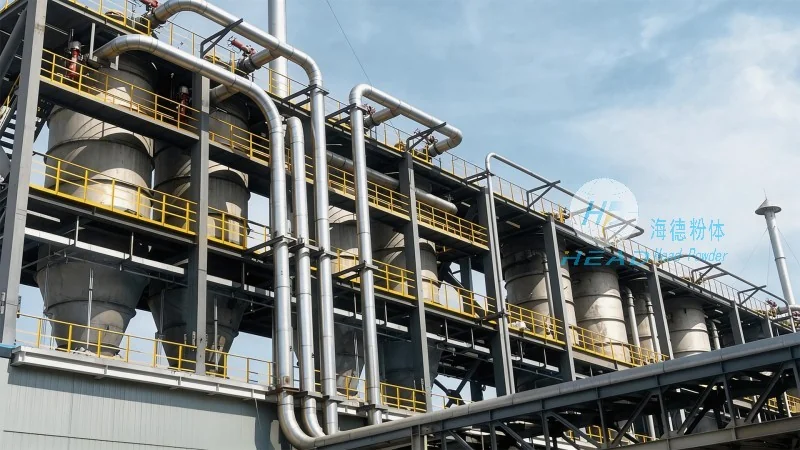
As a reputable company based in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. has established itself as a trusted provider of advanced pneumatic conveying solutions. With a focus on innovation and customer satisfaction, the company offers tailored systems that meet the unique needs of each client. By leveraging years of experience and expertise in material handling technology, HeadPowder ensures that its systems are designed to deliver optimal performance, reliability, and durability. The company's commitment to quality and safety is reflected in its adherence to industry standards and rigorous testing protocols, providing customers with peace of mind regarding the performance and longevity of their equipment. Whether for new installations or system upgrades, HeadPowder stands ready to support businesses in optimizing their material transport processes and enhancing overall operational efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top