Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer and supplier specializing in pneumatic conveying systems for various industrial applications. With a focus on high-efficiency and reliable material handling solutions, the company has established itself as a trusted partner in the field of bulk material transport, particularly for sensitive materials like nitrate ammonium fertilizer. This article explores the working principle and key characteristics of pneumatic conveying systems designed for nitrate ammonium fertilizer, highlighting the technical aspects and operational advantages of such systems.
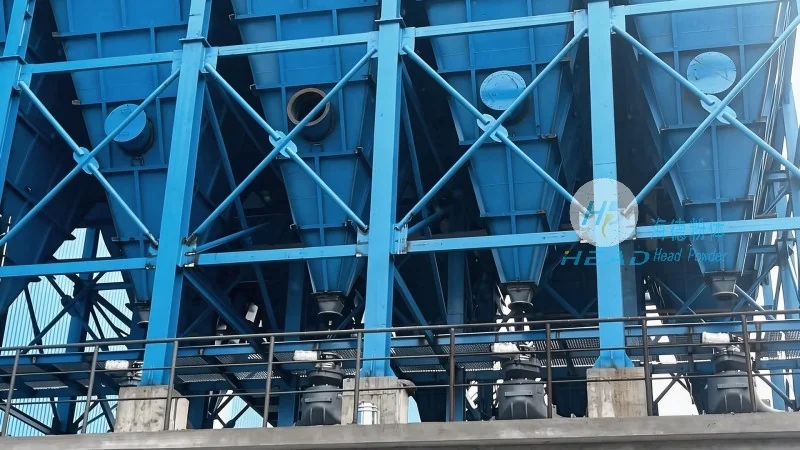
The pneumatic conveying system for nitrate ammonium fertilizer operates on the principle of using compressed air to transport bulk materials through a pipeline network. The process involves several key components, including a hopper for material storage, a feeder to control the flow rate, a compressor to generate the necessary air pressure, and a pipeline system that delivers the material to the destination. The material is typically fed into the system in a dry, granular form, and the compressed air creates a flow that propels the fertilizer particles through the pipeline. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance requirements and minimizing the risk of material contamination.
During the conveying process, the air and material mixture travels through the pipeline at a controlled velocity. The velocity is crucial as it must be sufficient to overcome the gravitational forces acting on the fertilizer particles while preventing excessive pressure drops that could lead to material deposition or blockages. The system often incorporates features such as air locks, cyclones, or filters to separate the material from the air stream at the discharge point, ensuring that the fertilizer is delivered in a clean and dry state. This separation process is critical for maintaining the quality of the product and preventing any potential hazards associated with the handling of nitrate-based materials.
One of the primary characteristics of pneumatic conveying systems for nitrate ammonium fertilizer is their ability to handle delicate and sensitive materials without causing degradation or damage. The air-based transport method minimizes friction and impact, which is essential for preserving the granular structure and chemical integrity of the fertilizer. This is particularly important for nitrate ammonium, as these compounds are susceptible to moisture absorption and chemical reactions if exposed to adverse conditions. By maintaining a dry and controlled environment within the pipeline, the system ensures that the fertilizer remains in optimal condition throughout the conveying process.
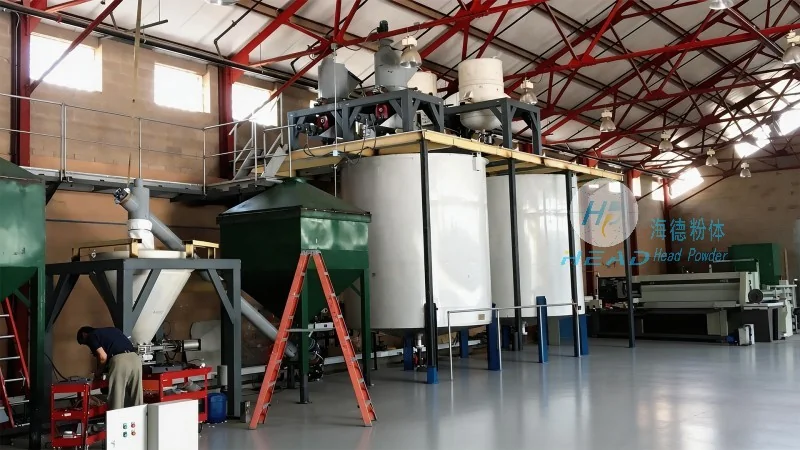
Another significant characteristic is the system's flexibility in terms of layout and integration with existing facilities. Pneumatic conveying systems can be customized to fit various plant configurations, allowing for horizontal, vertical, or mixed-direction transport of the fertilizer. This adaptability makes it suitable for a wide range of applications, from small-scale agricultural operations to large industrial production lines. The modular design of the system also facilitates easy expansion or modification as production needs change, providing long-term operational benefits.
Efficiency and energy consumption are also notable characteristics of these systems. Modern pneumatic conveying technologies utilize advanced control systems to optimize air pressure and flow rates, reducing energy waste and operational costs. The use of high-efficiency compressors and optimized pipeline designs further enhances the overall performance of the system. Additionally, the lack of moving parts in the conveying line reduces wear and tear, leading to lower maintenance costs and extended equipment lifespan. This combination of efficiency and reliability makes pneumatic conveying an attractive option for industries seeking sustainable and cost-effective material handling solutions.
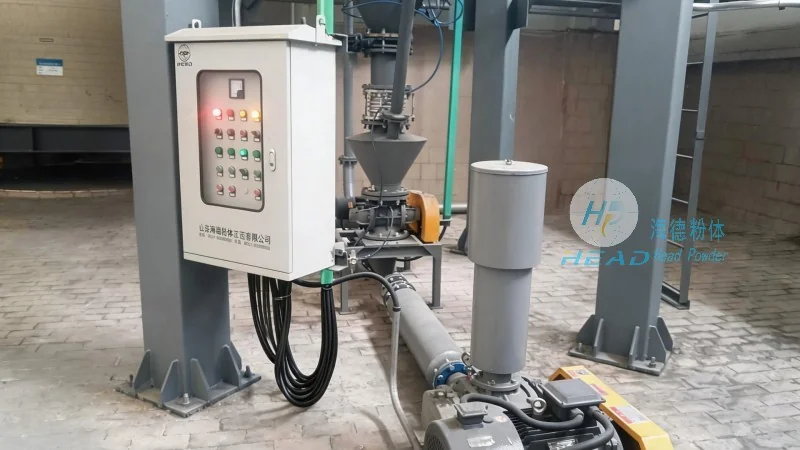
When implementing a pneumatic conveying system for nitrate ammonium fertilizer, several operational advantages become apparent. The system offers a continuous and uninterrupted flow of material, which is essential for maintaining production schedules and meeting demand. Unlike mechanical systems that may experience downtime due to maintenance or blockages, pneumatic conveying minimizes such interruptions, leading to higher overall productivity. The ability to transport materials over long distances without the need for intermediate storage or transfer points also simplifies the logistics of fertilizer distribution.
However, there are also considerations to keep in mind when using pneumatic conveying for nitrate ammonium. The system requires careful control of air pressure and flow to prevent material degradation or pipeline blockages. The presence of moisture in the air or material can lead to corrosion or caking, which may affect the system's performance over time. Regular maintenance, including cleaning of filters and pipelines, is necessary to ensure the system operates efficiently and safely. Additionally, the system's initial investment and energy consumption should be evaluated against the long-term benefits, as the cost-effectiveness of pneumatic conveying depends on the specific operational parameters and material handling requirements.
Shandong HeadPowder Engineering Co., Ltd. specializes in providing advanced pneumatic conveying solutions tailored to the unique needs of nitrate ammonium fertilizer handling. By leveraging the principles of air-based transport, these systems offer a reliable, efficient, and flexible method for moving bulk materials while preserving their quality and integrity. The working principle, characterized by the use of compressed air to propel material through pipelines, combined with key characteristics such as material protection, system adaptability, and energy efficiency, makes pneumatic conveying an ideal choice for industries requiring robust and sustainable material handling solutions. As the demand for high-quality fertilizer continues to grow, the adoption of such advanced systems will play a crucial role in meeting production and distribution needs while ensuring operational excellence and environmental responsibility.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top