Understanding the working principle and characteristics of pneumatic conveying for small-bag materials is crucial for industries that rely on efficient material handling solutions. This article provides a detailed overview, focusing on the technical aspects and practical applications of this method, while highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. as a leading provider in the field.
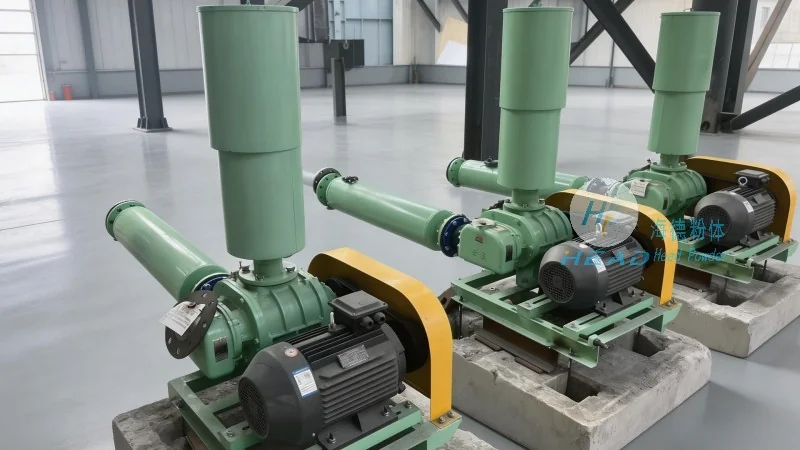
Pneumatic conveying for small-bag materials operates on the principle of using air to transport bulk materials from one location to another. The process typically involves a series of components that work in tandem to ensure smooth and efficient material transfer. At the core of the system is a hopper or feeder where the small-bag materials are loaded. An air compressor or blower generates the necessary airflow, which is then directed into the conveying line. As the air flows through the line, it picks up the material particles and transports them to the destination point, such as a silo, storage tank, or processing unit. The system may include features like cyclones or filters to separate the material from the air, ensuring that the material is delivered in a clean and controlled manner. The entire process is controlled by a system of valves, sensors, and controls that monitor the flow rate, pressure, and other critical parameters to maintain optimal performance.
When evaluating pneumatic conveying systems for small-bag materials, several key characteristics stand out as important factors for consideration. These characteristics influence the system's efficiency, reliability, and suitability for specific applications. First, the system's capacity and throughput are critical. The ability to handle varying material types and quantities ensures that the system can meet the demands of different production processes. Second, the system's flexibility is a significant advantage. Pneumatic conveying systems can be easily adapted to different layouts and configurations, allowing for customization to fit specific facility requirements. Third, the system's energy efficiency is an important consideration. Modern systems are designed to minimize energy consumption while maintaining high performance, reducing operational costs for the user. Fourth, the system's durability and maintenance requirements are also key factors. High-quality materials and robust construction ensure long-term reliability, while easy maintenance procedures keep downtime to a minimum. Finally, the system's safety features are essential for protecting personnel and equipment. Advanced safety controls and monitoring systems prevent accidents and ensure compliance with industry standards.
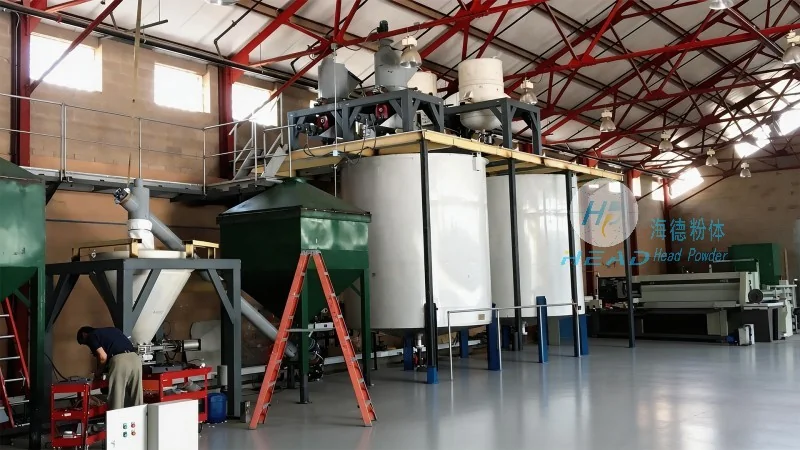
Implementing pneumatic conveying for small-bag materials offers numerous advantages that make it a preferred choice for many industries. One of the primary benefits is the ability to handle a wide range of materials, including powders, granules, and fine particles. This versatility allows the system to be used in various applications, from food processing to chemical manufacturing. Another advantage is the system's ability to maintain material integrity. Unlike mechanical conveying methods, which can cause material degradation or contamination, pneumatic conveying minimizes these risks by using air as the transport medium. This is particularly important for sensitive materials that require careful handling. Additionally, pneumatic conveying systems are relatively compact and can be installed in tight spaces, making them suitable for facilities with limited floor space. The system's ability to operate in a closed loop also helps to control dust and emissions, improving workplace safety and environmental compliance. Finally, the system's automation capabilities enhance operational efficiency. With advanced control systems, the conveying process can be monitored and adjusted in real-time, ensuring consistent performance and reducing the need for manual intervention.
Pneumatic conveying systems for small-bag materials are widely used in various industries due to their adaptability and efficiency. In the food and beverage industry, these systems are commonly used to transport ingredients such as flour, sugar, and spices from storage to processing areas. The ability to maintain product quality and prevent contamination is a key factor in this application. In the chemical industry, pneumatic conveying is used to handle a variety of powders and granules, including chemicals, pigments, and pharmaceuticals. The system's ability to handle hazardous materials safely is a significant advantage. In the pharmaceutical industry, the system's clean and controlled operation is essential for maintaining product purity and meeting regulatory requirements. In the agricultural industry, pneumatic conveying is used to transport grains, seeds, and other agricultural products from storage to processing facilities. The system's ability to handle bulk materials efficiently reduces labor costs and improves productivity. Finally, in the construction industry, pneumatic conveying is used to transport cement, sand, and other building materials to construction sites. The system's ability to transport materials over long distances without the need for additional equipment makes it a cost-effective solution.
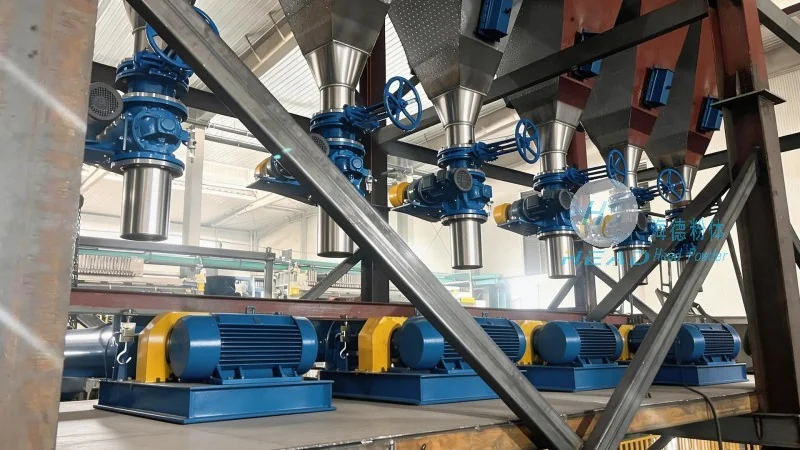
When selecting a pneumatic conveying system for small-bag materials, several factors need to be considered to ensure the best fit for the specific application. First, the type of material being conveyed is a critical factor. Different materials have different properties, such as particle size, density, and moisture content, which affect the system's design and performance. For example, fine powders may require a different system configuration than coarse granules. Second, the distance and layout of the conveying system are important considerations. The system's capacity and pressure requirements will vary based on the distance and number of turns in the line. Third, the system's integration with existing equipment is a key factor. The system should be compatible with existing storage and processing equipment to ensure seamless operation. Fourth, the system's maintenance and operational costs are important considerations. The initial cost of the system should be balanced against long-term maintenance and operational expenses. Finally, the system's reliability and performance are critical factors. The system should be able to operate continuously without frequent breakdowns, ensuring that production processes are not interrupted.
Pneumatic conveying for small-bag materials is a highly effective and versatile method for material handling. By understanding the working principle and characteristics of these systems, industries can make informed decisions about implementing the right solution for their specific needs. Shandong HeadPowder Engineering Co., Ltd. offers expertise and high-quality solutions in this field, providing customers with reliable and efficient pneumatic conveying systems that meet their requirements. Whether for food processing, chemical manufacturing, or other industries, pneumatic conveying systems offer numerous advantages that enhance operational efficiency and product quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top