Soap granule powder pneumatic conveying equipment is a specialized system engineered to transport soap granules and other fine powders efficiently and safely. This equipment is widely utilized across various industries, including chemical, food, and pharmaceutical sectors, where the handling of granular materials demands precision and minimal contamination. The system operates by leveraging air pressure or vacuum to move powder particles through a network of pipes, ensuring a clean and dust-free process.
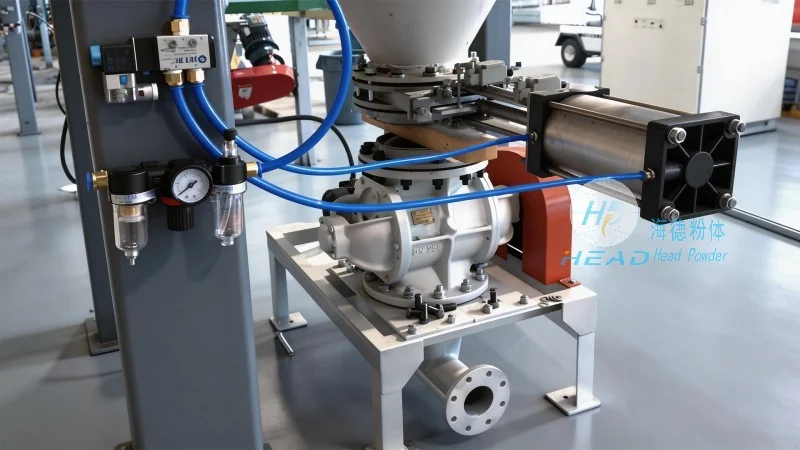
The core working principle of soap granule powder pneumatic conveying equipment centers on the movement of powder particles suspended in a gas stream. Typically, the system employs either positive pressure (air blow) or negative pressure (suction) to generate the necessary force for material transport. In the positive pressure system, a blower or compressor supplies compressed air into the conveying line, creating an upward flow that lifts the soap granules from the hopper. The particles are then carried through the pipeline to the destination, where a separator or cyclone separates the powder from the air. In the negative pressure system, a vacuum pump creates a low-pressure environment, drawing the powder from the source and transporting it to the receiving container. The choice between positive and negative pressure depends on factors such as the distance of transport, the type of powder, and the required flow rate.
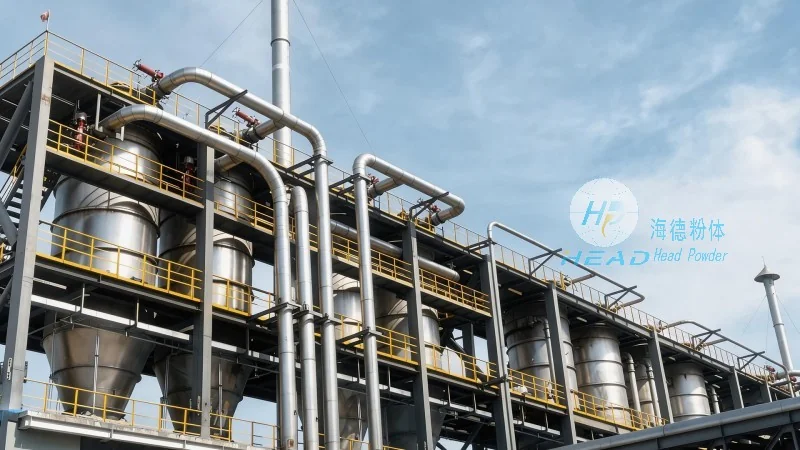
Soap granule powder pneumatic conveying equipment offers several advantages that make it a preferred choice for material handling. One of the primary features is its ability to handle delicate or sensitive materials like soap granules without causing degradation or contamination. The system minimizes direct contact between the powder and mechanical components, reducing the risk of particle breakage or contamination from external sources. Additionally, the equipment is designed to operate with low energy consumption, making it cost-effective for long-term use. It also provides a dust-free environment, which is crucial for maintaining hygiene standards in industries such as food and pharmaceuticals. The flexibility of the system allows for easy integration with existing production lines, and it can be customized to accommodate different particle sizes and flow rates. Another notable feature is the self-cleaning capability of some models, which helps prevent clogging and ensures consistent performance over time.
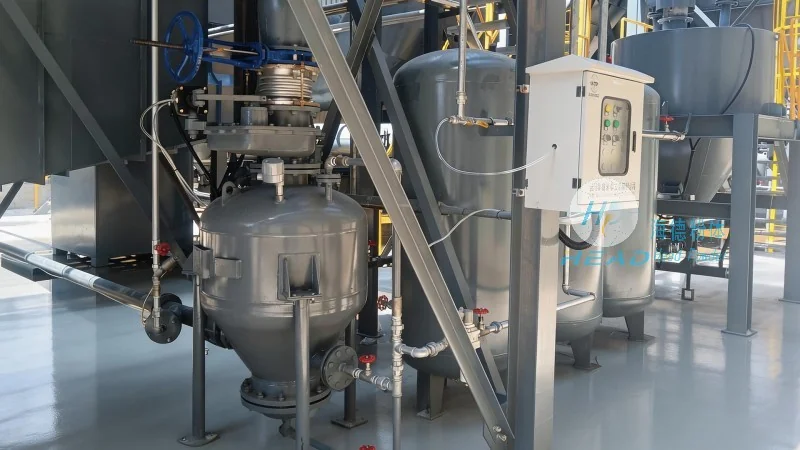
The performance of soap granule powder pneumatic conveying equipment is defined by several technical specifications that ensure optimal operation. The conveying capacity, measured in kilograms per hour or cubic meters per hour, depends on the system's design and the type of powder being transported. For soap granules, typical capacities range from 100 to 5000 kg/h, depending on the particle size and the air flow rate. The pressure requirements vary between positive and negative systems; positive pressure systems usually operate at pressures of 0.5 to 1.5 bar, while negative pressure systems may require higher vacuum levels, often between 0.5 to 1 bar. The pipeline diameter is another critical specification, as it affects the flow velocity and pressure drop. Common diameters range from 50 mm to 200 mm, selected based on the expected flow rate and the length of the conveying line. The equipment also includes components such as rotary valves or star feeders at the inlet to control the flow rate and prevent backflow. Separators or filters are integrated to capture any residual powder from the air stream, ensuring that the exhaust is clean and compliant with environmental regulations.
Soap granule powder pneumatic conveying equipment is applied in various industrial settings where the efficient and hygienic transport of soap granules is essential. In the chemical industry, it is used to move raw soap granules from storage silos to processing units, ensuring a continuous supply without manual handling. In the food industry, the equipment is crucial for transporting soap granules used in cleaning and sanitizing processes, maintaining strict hygiene standards. The pharmaceutical industry also benefits from this technology, as it allows for the safe and controlled transport of soap granules used in manufacturing or cleaning of equipment. The benefits of using this equipment include increased production efficiency, reduced labor costs, and improved product quality. By eliminating manual handling, the system minimizes the risk of human error and contamination, leading to higher product purity and consistency. Additionally, the dust-free operation contributes to a safer working environment, reducing the risk of respiratory issues for workers. The flexibility of the system also allows for easy adaptation to changing production demands, making it a reliable solution for dynamic industrial processes.
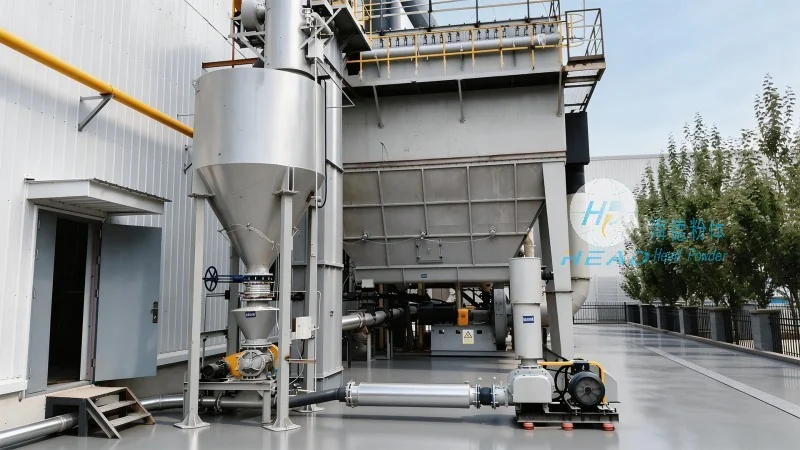
HeadPowder, a leading manufacturer of pneumatic conveying equipment, specializes in providing customized solutions for various powder handling applications. With a strong focus on innovation and quality, the company has developed advanced systems tailored to the unique needs of industries such as soap manufacturing. Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, leverages years of experience and technical expertise to deliver high-performance equipment that meets international standards. The company's products are designed to enhance operational efficiency, reduce maintenance costs, and ensure compliance with environmental regulations. By partnering with HeadPowder, businesses can benefit from reliable and durable equipment that supports their production goals while maintaining safety and hygiene standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top