Glucose material handling systems are critical components in various industrial processes, particularly in the food and pharmaceutical sectors where precise and efficient transport of glucose is essential. These systems are designed to ensure the safe and reliable movement of glucose from storage to processing units, maintaining product quality and operational efficiency. The following sections will delve into the working principles and key features of such equipment, providing a comprehensive understanding for industry professionals.
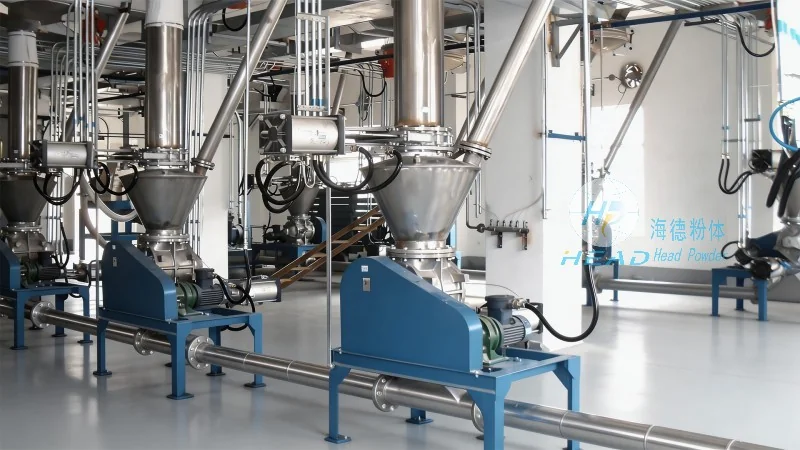
The core functionality of a glucose material handling system revolves around the integration of several mechanical and control components. At its foundation, the system typically includes storage silos or hoppers that hold the raw glucose material. From these storage units, the material is transferred through a network of conveying equipment, such as screw conveyors, belt conveyors, or pneumatic systems, depending on the specific application and material characteristics. The conveying process is driven by motors or air pressure, which move the glucose through pipelines or conveyor belts to the processing or packaging areas.
Control systems play a pivotal role in regulating the flow and speed of the material. Sensors and level indicators monitor the material levels in the silos and conveyors, ensuring that the system operates within optimal parameters. These sensors send signals to the control panel, which adjusts the motor speed or air pressure to maintain a consistent flow rate. Additionally, safety features, such as emergency stop buttons and overload protection, are integrated to prevent accidents and equipment damage during operation.
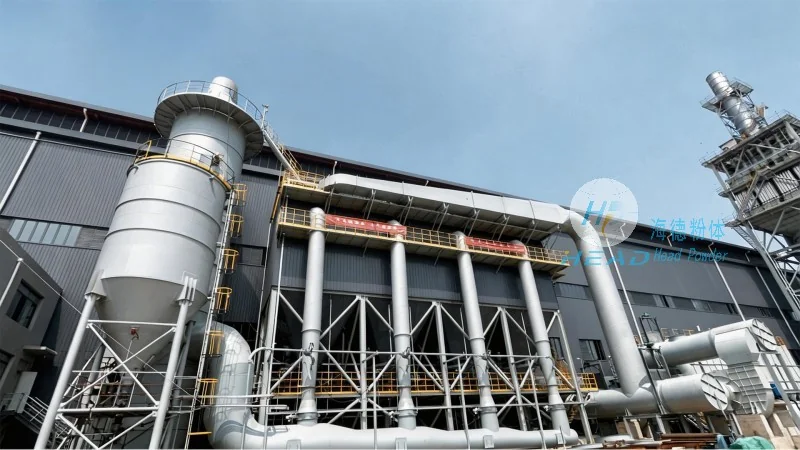
Several distinct features make glucose material handling systems highly effective and adaptable to diverse industrial needs. Firstly, the systems are engineered for hygienic operation, which is crucial in food and pharmaceutical industries. This includes smooth, easy-to-clean surfaces, stainless steel construction, and sealed components that prevent contamination and maintain product purity. The design also minimizes material buildup and residue, reducing the risk of microbial growth and ensuring compliance with regulatory standards.
Another notable feature is the system's flexibility in handling different glucose forms, such as granules, powders, or liquid solutions. This adaptability allows the equipment to be used in various production stages, from raw material storage to intermediate processing or final packaging. The modular design of many systems enables easy integration with existing production lines, reducing installation time and costs.
Efficiency and reliability are also key attributes. Advanced control technologies, such as variable frequency drives (VFDs), optimize energy consumption by adjusting motor speed based on the actual load. This not only reduces operational costs but also extends the lifespan of the equipment. Moreover, the systems are built to withstand the demands of continuous operation, with robust components that minimize downtime and maintenance requirements.
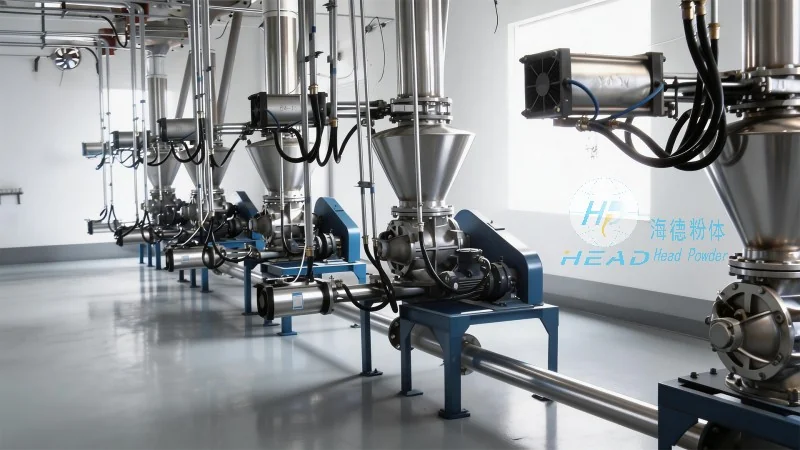
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in the design, production, and installation of high-quality glucose material handling systems. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner for industries requiring reliable and efficient material transport solutions. HeadPowder's systems are engineered to meet international standards and are tailored to the specific needs of each client, ensuring optimal performance and longevity.
HeadPowder is headquartered in Shandong, China, where the company leverages advanced manufacturing facilities and a skilled workforce to deliver superior products. The company's focus on research and development ensures that its systems incorporate the latest technologies and best practices, providing customers with competitive advantages in their respective markets. By prioritizing quality, safety, and efficiency, HeadPowder continues to set industry benchmarks for glucose material handling equipment.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top