HeadPowder, a leading enterprise in the field of material handling solutions, specializes in the efficient and reliable transport of cobalt hydroxide. This article delves into the working principles and key characteristics of cobalt hydroxide material handling systems, providing a comprehensive overview for industry professionals and potential clients. Based in Shandong, China, HeadPowder Engineering Co., Ltd. has developed advanced systems tailored to meet the specific demands of cobalt hydroxide processing and transportation, ensuring high-quality, safe, and sustainable operations.
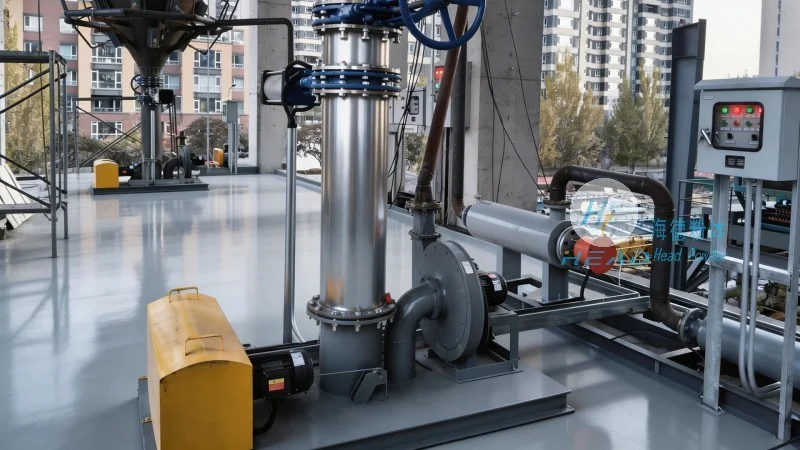
Cobalt hydroxide is a critical raw material widely used in the production of lithium-ion batteries, particularly in the manufacturing of cobalt-based cathode materials. The safe and efficient handling of this material is essential to ensure product quality, minimize environmental risks, and enhance operational efficiency. HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, has developed advanced systems tailored to meet the specific demands of cobalt hydroxide processing and transportation. These systems are designed to handle the unique properties of cobalt hydroxide, such as its fine particle size, hygroscopic nature, and potential for static charge accumulation.
The material handling process for cobalt hydroxide typically involves several integrated steps, each designed to optimize the flow of material from storage to processing units. The core working principle revolves around the use of specialized equipment such as conveyor belts, pneumatic conveying systems, and automated storage and retrieval systems (AS/RS). These systems work in tandem to ensure that cobalt hydroxide is moved with precision, minimal dust generation, and adherence to safety standards. The process begins with the receipt of raw cobalt hydroxide, which is often stored in bulk containers or silos. From there, the material is transferred to conveyor belts for initial transport to processing areas.
Conveyor belts, for instance, are commonly employed for horizontal and slight incline transport, allowing for continuous movement of bulk cobalt hydroxide. The design of these belts often incorporates anti-static and dust-proof features to prevent material buildup and ensure compliance with industrial safety regulations. The belts may be equipped with variable speed drives to adjust the flow rate based on production needs, providing flexibility in handling different material volumes. Pneumatic conveying systems, on the other hand, utilize air pressure to transport fine or powdery cobalt hydroxide through pipelines, offering flexibility in routing and reduced risk of contamination compared to mechanical systems. These systems typically use positive pressure or negative pressure to move material, with positive pressure being more common for long-distance transport and negative pressure for short distances or to prevent dust leakage.
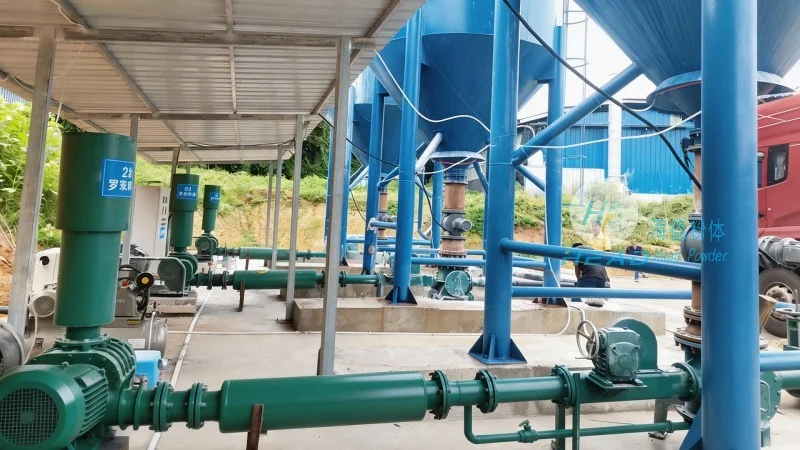
Automated storage and retrieval systems (AS/RS) play a crucial role in managing inventory and facilitating the smooth transition between different stages of the production process. These systems use robotic arms or automated cranes to retrieve and store cobalt hydroxide containers, ensuring that material is always available when needed while maintaining organized storage. The integration of these technologies ensures a seamless workflow, from raw material intake to final product dispatch. The AS/RS can be integrated with inventory management software, allowing for real-time tracking of material levels and automated reordering when stock falls below a certain threshold. This integration enhances operational efficiency and reduces the risk of stockouts or overstocking.
HeadPowder's cobalt hydroxide material handling systems are characterized by several distinct features that set them apart in the industry. Firstly, the systems are engineered for high efficiency, with optimized throughput rates that minimize downtime and maximize production capacity. This is achieved through the use of high-capacity conveyor belts, efficient pneumatic conveying networks, and intelligent inventory management software. The conveyor systems are designed with wide, heavy-duty belts capable of handling large volumes of cobalt hydroxide without slipping or material degradation. The pneumatic conveying lines are equipped with filters and cyclones to separate any material that may have escaped the system, ensuring that the air is clean and the material remains pure.
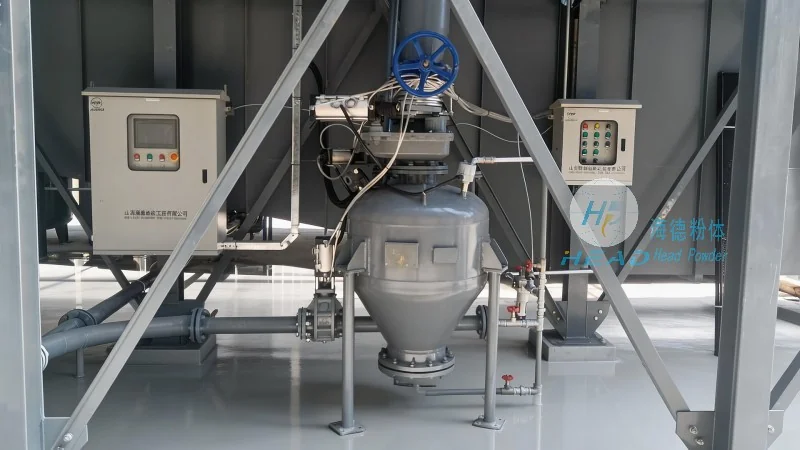
Secondly, the systems prioritize safety and environmental protection. Anti-static and dust-proof designs reduce the risk of fire hazards and dust explosions, while enclosed systems and filtration mechanisms minimize the release of airborne particles into the environment. This commitment to safety aligns with global regulatory standards and enhances the overall sustainability of cobalt hydroxide processing operations. The systems may also include explosion-proof components and fire suppression systems to further enhance safety. Additionally, the use of closed-loop conveyor systems and dust collection systems helps to reduce the environmental impact of cobalt hydroxide handling, making the process more sustainable.
Thirdly, the systems offer flexibility and adaptability to varying production needs. Modular designs allow for easy expansion or reconfiguration of the material handling infrastructure as production scales or product specifications change. This flexibility ensures that the systems can evolve with the evolving demands of the cobalt hydroxide industry, providing long-term value to clients. The modular approach also allows for the integration of new technologies as they become available, such as advanced sensors or AI-driven control systems, to further enhance performance and efficiency.
HeadPowder Engineering Co., Ltd. provides advanced cobalt hydroxide material handling solutions that combine cutting-edge technology with robust engineering principles. By understanding the working principles and key characteristics of these systems, businesses can enhance their operational efficiency, ensure product quality, and maintain compliance with industry standards. With a focus on innovation and customer satisfaction, HeadPowder continues to be a trusted partner in the development of efficient material handling solutions for the cobalt hydroxide sector. The company's commitment to quality, safety, and sustainability ensures that clients receive reliable and effective systems that meet their specific needs and contribute to the success of their operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top