HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced powder conveying systems for industrial applications. This article delves into the working principles and key features of soda ash powder conveying systems, highlighting how these solutions enhance operational efficiency and reliability in bulk material handling.
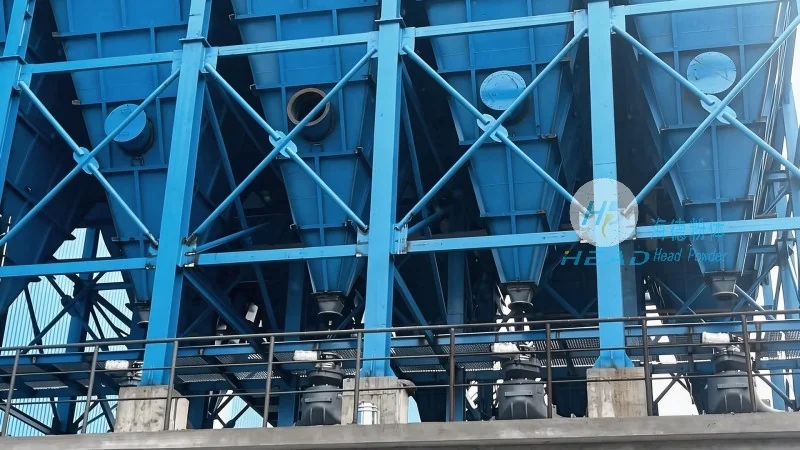
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer and supplier of powder handling equipment. With a strong presence in the industrial sector, the company has built a reputation for delivering high-quality, customized solutions tailored to the unique needs of clients. HeadPowder’s team of experienced engineers and technicians leverages cutting-edge technology and rigorous quality control measures to ensure that every system meets the highest standards of performance and durability.
The core of a soda ash powder conveying system lies in its ability to transport fine powders like soda ash efficiently and safely. These systems typically consist of several key components, including feeders, conveyors, and control units, all working in tandem to ensure smooth material flow. The process begins with the material being fed into a hopper or storage silo, where it is then transferred to the conveyor via a feeder mechanism. Common types of conveyors used in such systems include pneumatic conveying lines, screw conveyors, and bucket elevators, each chosen based on the specific characteristics of the soda ash and the operational requirements of the facility.
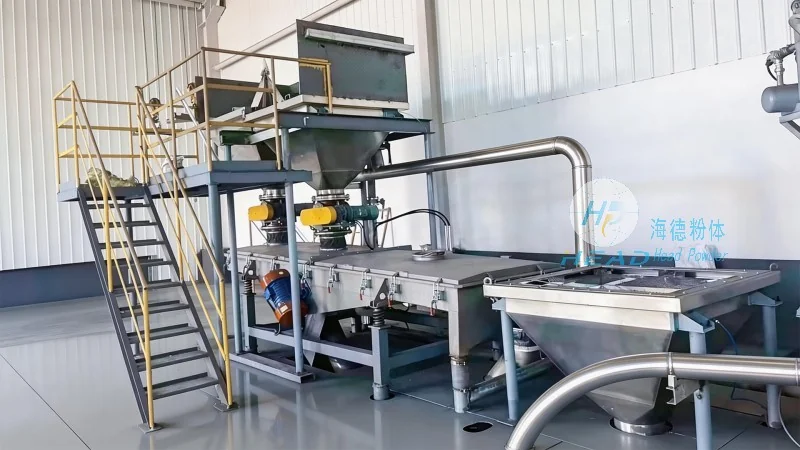
Pneumatic conveying, for instance, utilizes compressed air to move the powder through a pipeline, offering advantages such as low maintenance and the ability to handle fine powders without the need for mechanical contact. Screw conveyors, on the other hand, rely on rotating screws to push the material forward, making them suitable for horizontal or slight incline applications. The control unit plays a critical role in regulating the flow rate, pressure, and other parameters to maintain optimal performance and prevent issues like blockages or overloading.
HeadPowder’s soda ash powder conveying systems are designed with several distinctive features that set them apart in the industry. One of the primary advantages is their high efficiency in material transport, which minimizes downtime and maximizes production output. The systems are engineered to handle varying particle sizes and moisture content, ensuring consistent performance even with challenging material properties. Additionally, the equipment is built with corrosion-resistant materials to withstand the chemical nature of soda ash, extending its service life and reducing maintenance costs.
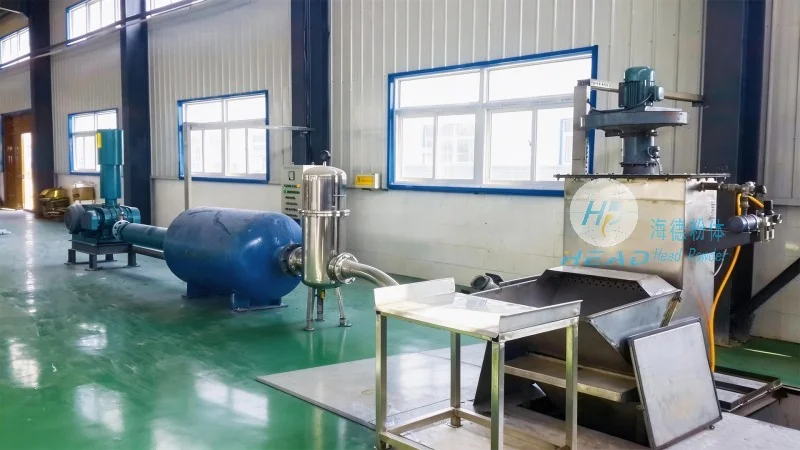
Another notable feature is the system’s adaptability to different operational environments. Whether installed in a manufacturing plant, a storage facility, or a processing line, the conveying systems can be customized to fit specific space constraints and integration requirements. The integration of advanced sensors and monitoring tools allows for real-time tracking of material flow, enabling operators to quickly identify and address any issues that may arise. This proactive approach enhances overall system reliability and reduces the risk of material loss or contamination.
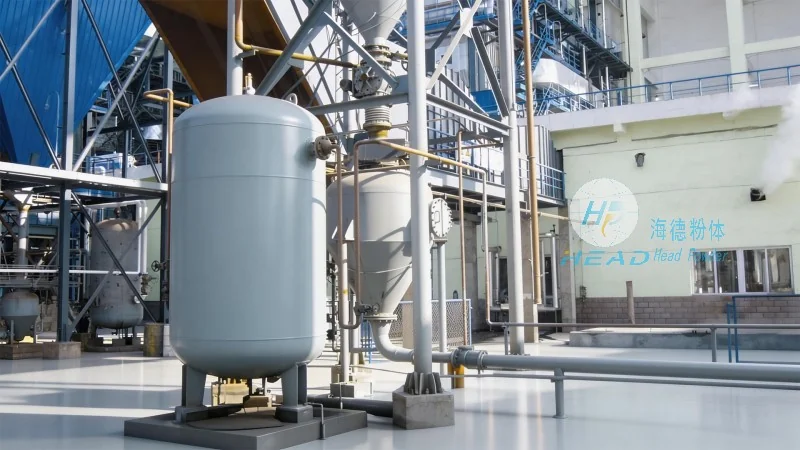
The systems also prioritize safety and compliance with industry standards. By incorporating features such as dust suppression and explosion-proof designs, HeadPowder ensures that the conveying process is conducted in a secure manner, minimizing the risk of accidents or environmental hazards. This commitment to safety aligns with the company’s dedication to providing sustainable and responsible solutions for its clients.
HeadPowder’s soda ash powder conveying systems represent a sophisticated solution for the efficient and reliable handling of soda ash in industrial settings. By combining advanced engineering, robust design, and user-friendly controls, these systems address the unique challenges of powder transport while delivering superior performance. With a strong foundation in Shandong, China, HeadPowder continues to innovate and provide tailored solutions that meet the evolving needs of the industry, ensuring long-term success for its clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top