HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for calcium nitrite applications. With a strong presence in the region, the company has established itself as a reliable partner for industries requiring efficient material handling solutions. The calcium nitrite pneumatic conveying system is a critical piece of equipment for transporting calcium nitrite, a compound widely used in various industrial processes, from chemical manufacturing to food processing and beyond.
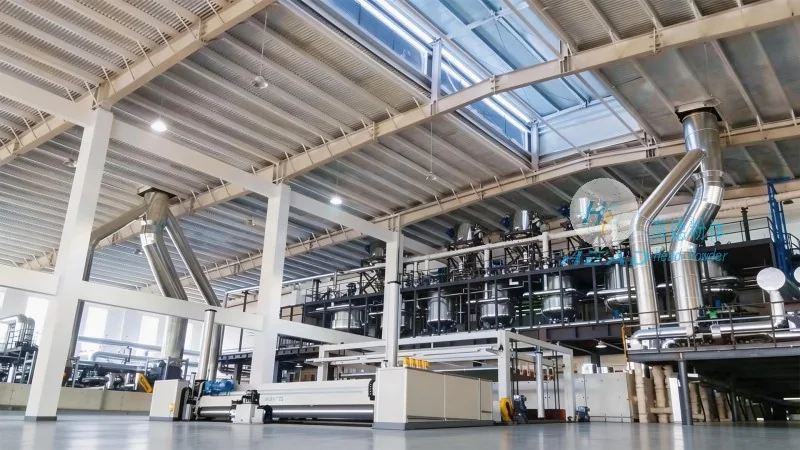
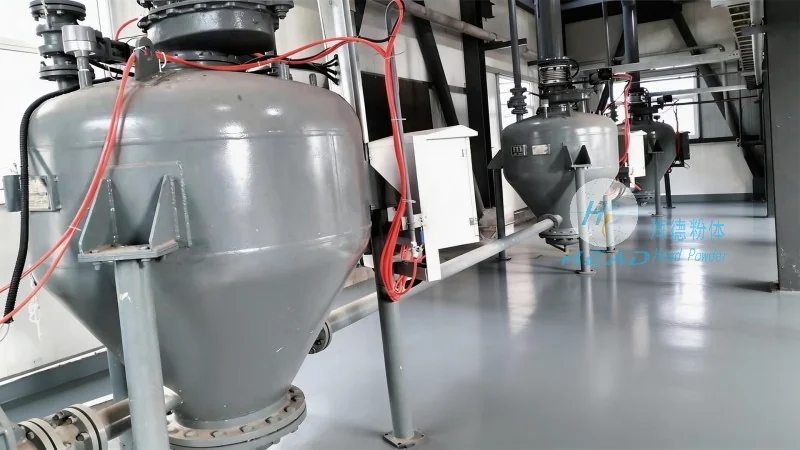
The core mechanism of the calcium nitrite pneumatic conveying system involves the use of air or gas to transport the material through a pipeline. This process, known as pneumatic conveying, operates by creating a pressure differential between the inlet and outlet of the system. The system typically consists of a hopper for material storage, a rotary valve for controlled discharge, a conveyor line, and a receiver for the discharged material. As the material is fed into the system, the rotary valve regulates the flow, ensuring a consistent feed rate. Simultaneously, a blower or compressor generates the necessary air pressure, which propels the calcium nitrite particles through the pipeline. The air velocity is carefully controlled to maintain the material in a suspended state, preventing blockages and ensuring smooth transport. The system may also incorporate features such as pulse jets or cyclones to enhance separation and prevent material buildup in the pipeline. The entire process is designed to be energy-efficient and reliable, minimizing downtime and maximizing throughput for calcium nitrite handling operations.
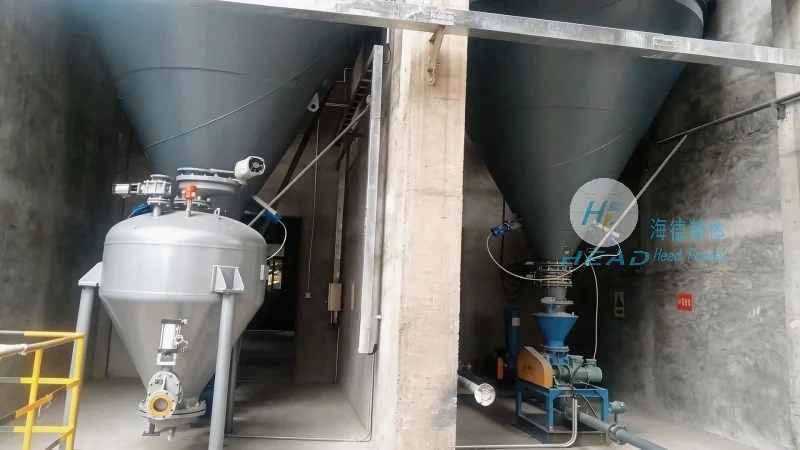
The calcium nitrite pneumatic conveying system offered by HeadPowder is equipped with several distinctive features that set it apart from conventional methods. Firstly, the system is designed for high efficiency, with minimal material loss and low maintenance requirements. The use of air as the conveying medium eliminates the need for mechanical components like belts or screws, reducing wear and tear and extending the equipment's lifespan. This design also contributes to a cleaner and more hygienic operation, which is particularly important in industries such as food and pharmaceuticals where contamination control is paramount. Secondly, the system provides excellent control over material flow, allowing for precise regulation of the discharge rate. This feature is crucial for maintaining consistent product quality and preventing overloading or underloading of downstream processes. Additionally, the system is highly adaptable, capable of handling a wide range of calcium nitrite particle sizes and moisture content without compromising performance. The modular design of the equipment enables easy integration into existing production lines, reducing installation time and costs. Furthermore, the system is equipped with safety features such as pressure relief valves and emergency shut-off mechanisms, ensuring safe operation even under abnormal conditions. These features collectively contribute to a robust and reliable solution for calcium nitrite transportation, meeting the stringent demands of modern industrial applications.
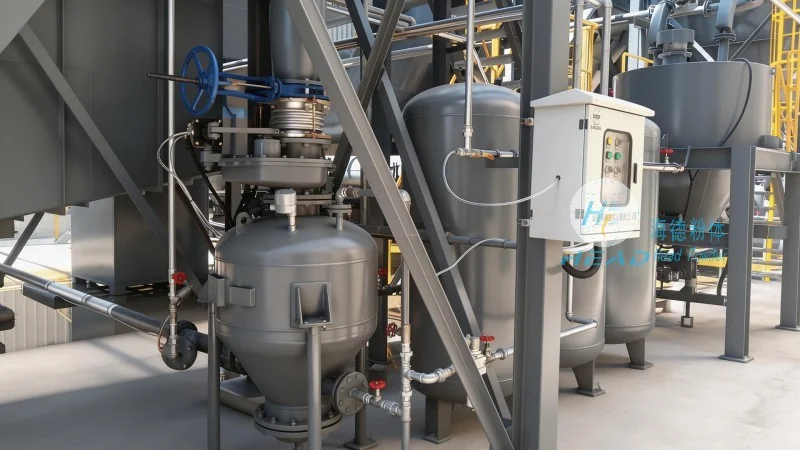
The calcium nitrite pneumatic conveying system is widely utilized in various industrial sectors due to its versatility and efficiency. In the chemical industry, it is commonly employed for transporting calcium nitrite used in the production of fertilizers, explosives, and other chemical compounds. The system's ability to handle abrasive materials and maintain consistent flow rates makes it ideal for these applications. In the food industry, the system is used for transporting calcium nitrite used as a food additive, ensuring that the material is handled hygienically and without contamination. The system's clean design and easy maintenance features align with the strict regulatory requirements of the food sector. Similarly, in the pharmaceutical industry, the system is employed for transporting calcium nitrite used in drug formulations, where precision and purity are critical. The system's ability to maintain a sterile environment and prevent cross-contamination is a key advantage. Beyond these sectors, the system is also used in the mining and construction industries for transporting calcium nitrite used as a stabilizer or additive in concrete and other building materials. The system's high throughput and reliability make it suitable for large-scale operations in these industries. Overall, the calcium nitrite pneumatic conveying system provides significant benefits to industries by improving operational efficiency, reducing costs, and enhancing product quality. By eliminating the need for manual handling and reducing material loss, the system contributes to a more sustainable and cost-effective material handling process.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top