Pharmaceutical material handling conveyors are specialized systems engineered to transport and manage various materials within pharmaceutical manufacturing facilities. These systems are crucial for ensuring efficient, safe, and compliant material flow, which is essential for maintaining high standards in drug production. The design of such conveyors integrates multiple factors, including material type, processing requirements, and regulatory compliance, to deliver reliable performance in a controlled environment.
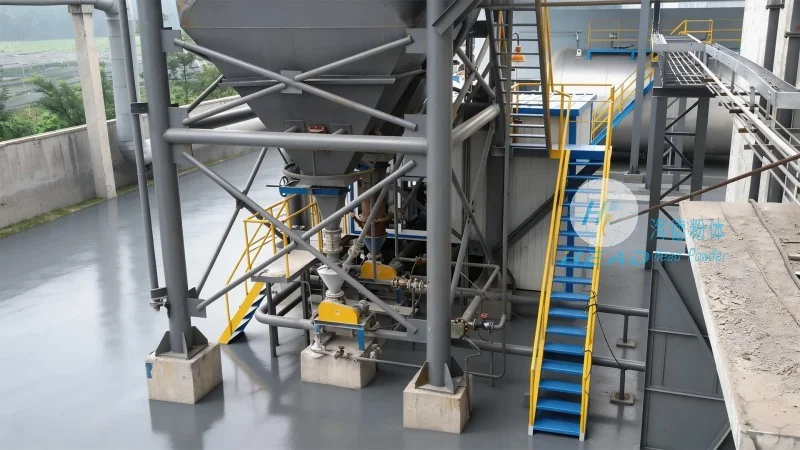
HeadPowder Engineering Co., Ltd., a leading provider based in Shandong, China, specializes in designing and manufacturing these critical systems. A typical pharmaceutical material handling conveyor consists of several key components, including conveyor belts, rollers, idlers, and control systems. The choice of materials for these components is paramount, as they must meet stringent hygiene and safety standards. For instance, stainless steel is commonly used for conveyor surfaces to prevent contamination and facilitate cleaning. Additionally, the system may incorporate sensors and automation controls to monitor and adjust the flow of materials in real-time, ensuring precision and minimizing errors.
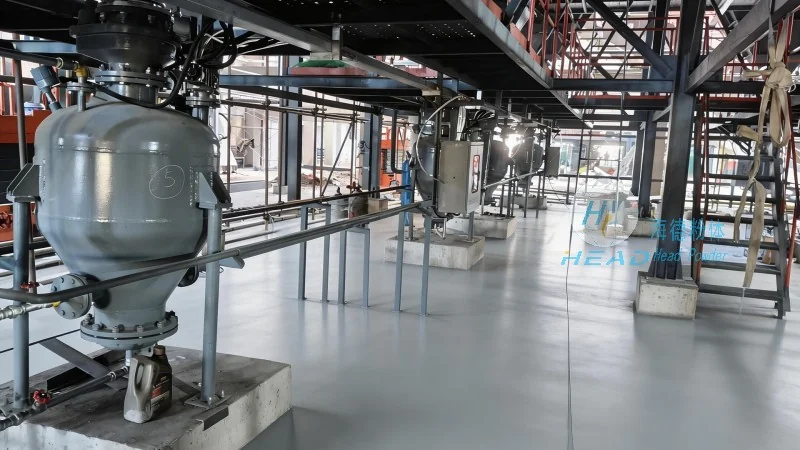
The design principles of pharmaceutical material handling conveyors are guided by several critical considerations. First, the system must prioritize hygiene and cleanliness to prevent cross-contamination, which is a major concern in pharmaceutical production. This involves using smooth, non-porous surfaces and easy-to-clean designs. Second, the conveyor must be capable of handling a variety of materials, from raw ingredients to finished products, with flexibility in speed and direction. Third, safety is a top priority, as the system operates in environments where human interaction is common. Features such as emergency stop buttons, safety guards, and interlocking mechanisms are integrated to protect operators and maintain operational safety. Fourth, the design must align with regulatory standards, such as those set by the FDA or other international bodies, to ensure compliance and avoid penalties.
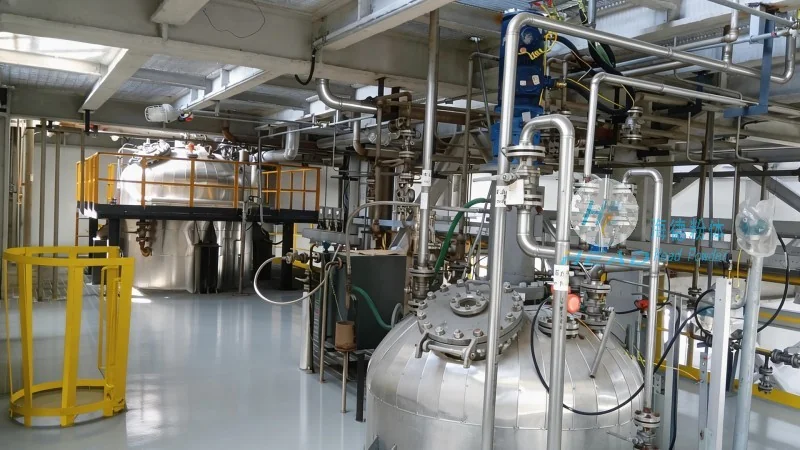
Pharmaceutical material handling conveyors offer numerous benefits that enhance operational efficiency and product quality. By automating material movement, these systems reduce manual labor, minimize human error, and improve overall throughput. They also enable better inventory management by providing real-time tracking of materials as they move through different stages of production. In addition, the consistent and controlled flow of materials helps maintain product integrity, ensuring that each batch meets the required specifications. HeadPowder Engineering Co., Ltd. leverages advanced engineering and manufacturing capabilities to tailor these systems to the specific needs of pharmaceutical clients, ensuring that each solution is optimized for performance, safety, and compliance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top