When it comes to efficiently moving materials in various industrial settings, mobile material handling equipment plays a crucial role. These versatile systems are designed to transport goods, raw materials, or finished products with ease, offering flexibility and adaptability that fixed systems often lack. Understanding what these equipment are and the underlying design principles is essential for businesses seeking to optimize their material handling processes, as companies like Shandong HeadPowder Engineering Co., Ltd. specialize in providing tailored solutions for such needs.
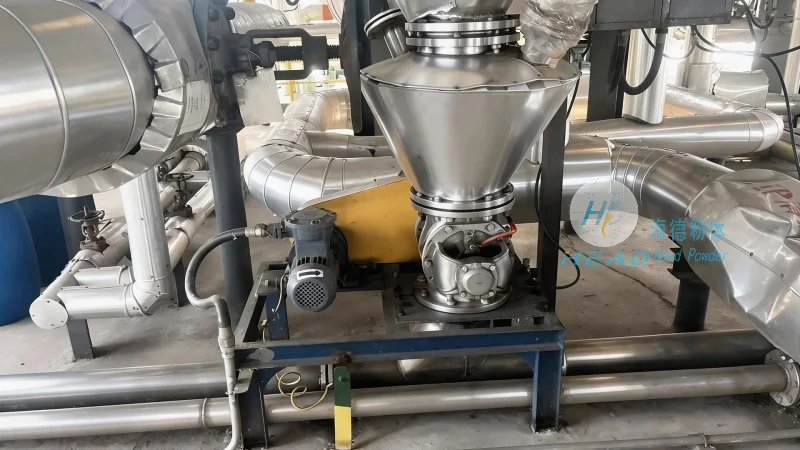
Mobile material handling equipment refers to a range of machinery and systems that can be moved or repositioned as needed within a facility or between different work areas. Unlike static conveyor systems or fixed cranes, these devices are designed for mobility, allowing them to adapt to changing production needs and spatial constraints. The primary goal of such equipment is to enhance productivity, reduce labor costs, and improve overall operational efficiency in material handling tasks. With roots in industrial engineering, these systems are now widely used across sectors, including manufacturing, logistics, and warehousing.
At the core of mobile material handling equipment are several key components that work together to facilitate smooth material movement. These typically include a power source (such as electric motors or hydraulic systems), a load-bearing structure (like a chassis or frame), and a mechanism for movement (such as wheels, tracks, or caterpillar treads). The design of these components is critical to ensuring the equipment can handle different loads, operate in various environments, and maintain stability during transport. For instance, the choice of wheels or tracks depends on the surface conditions and load requirements, with rubber tires suitable for smooth floors and steel tracks for rough terrain.
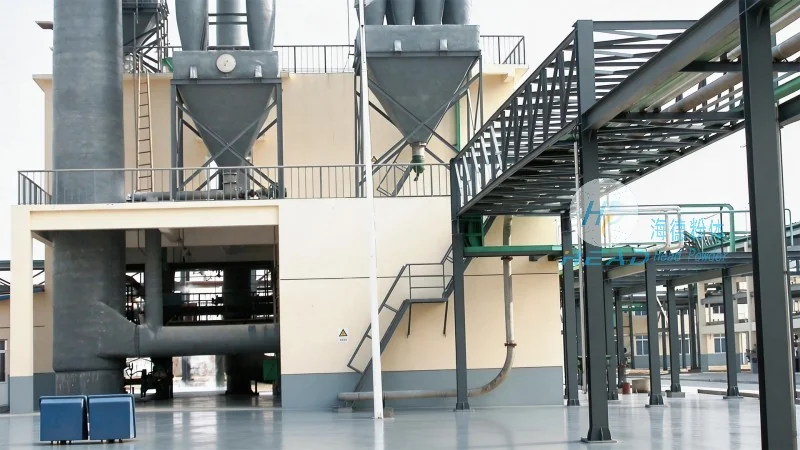
One of the most common types of mobile material handling equipment is the mobile conveyor system. These systems often feature adjustable heights and lengths, allowing them to be configured to suit specific workflow requirements. They may include features like belt conveyors, roller conveyors, or chain conveyors, which can be used to transport items horizontally, vertically, or at an incline. The flexibility of mobile conveyors makes them ideal for applications in manufacturing, warehousing, and distribution centers where space is limited or where production lines need to be reconfigured frequently. Such systems are particularly valuable in environments where fixed infrastructure may not be feasible or cost-effective.
The design of mobile material handling equipment is guided by several fundamental principles aimed at maximizing functionality, safety, and efficiency. These principles include load capacity, mobility, durability, and adaptability. Engineers and designers must consider the weight and dimensions of the materials to be handled, ensuring the equipment can safely carry the load without compromising stability. Mobility is another critical factor, as the equipment needs to move smoothly across different surfaces, whether it's a smooth factory floor or uneven terrain. This requires careful consideration of the power source and movement mechanism to ensure consistent performance.
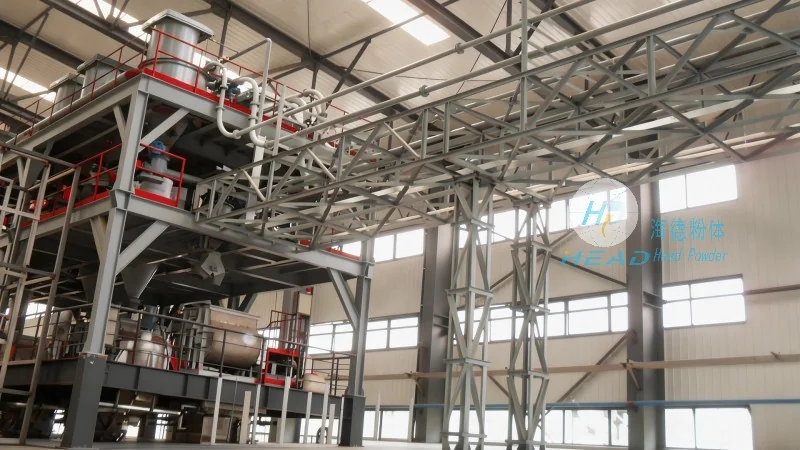
Durability is essential, especially in industrial environments where equipment is subjected to heavy use and potential wear and tear. Materials such as robust steel or high-grade polymers are often used in the construction of these devices to ensure longevity. Additionally, the design must allow for easy maintenance and repair, as downtime can significantly impact operational efficiency. This includes features like accessible components and modular designs that simplify servicing. Adaptability is also a key design principle, as mobile equipment should be able to integrate with existing systems and workflows, providing seamless material flow without disrupting production processes. This may involve compatibility with existing conveyor networks or the ability to connect to automation systems.
Mobile material handling equipment finds applications in a wide range of industries, including manufacturing, logistics, and warehousing. In manufacturing facilities, these systems are used to transport raw materials to production lines and finished products to storage areas. They can also be used in assembly lines to move components between workstations, improving the flow of production and reducing bottlenecks. For example, in automotive manufacturing, mobile conveyors can transport car parts from one assembly station to the next, streamlining the production process. In logistics and distribution centers, mobile conveyors are often employed to move packages and goods between different sections of the facility, such as from receiving docks to shipping areas. This helps to optimize space utilization and reduce the time required for order fulfillment.
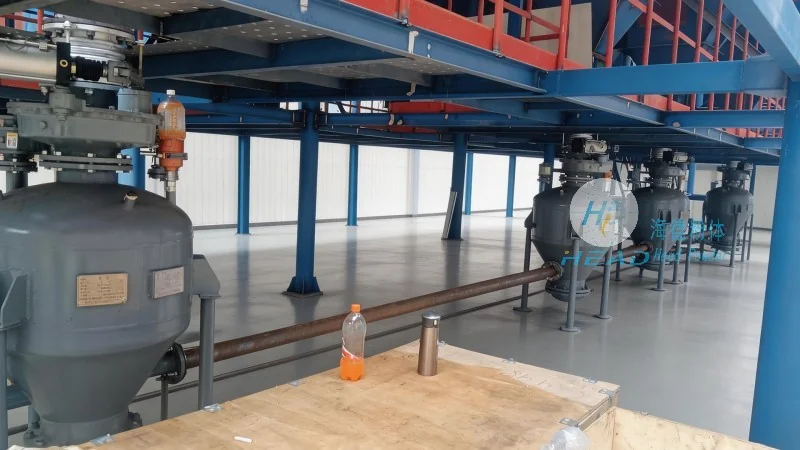
The benefits of using mobile material handling equipment are numerous. By providing flexibility and adaptability, these systems allow businesses to respond quickly to changes in demand or production schedules. This can lead to increased productivity and reduced costs, as labor and equipment utilization are optimized. Additionally, the use of mobile equipment can improve safety in the workplace by reducing the need for manual lifting and transporting of heavy loads, thereby minimizing the risk of injuries. This not only enhances worker safety but also reduces the likelihood of workplace accidents and associated costs.
Mobile material handling equipment is a vital component of modern industrial operations, offering solutions that enhance efficiency, flexibility, and safety in material handling processes. By understanding the design principles and applications of these systems, businesses can make informed decisions about implementing the right equipment to meet their specific needs. As technology continues to advance, mobile material handling equipment is likely to become even more sophisticated, with features like automation and smart sensors that further improve operational performance. Companies like Shandong HeadPowder Engineering Co., Ltd. play a key role in developing and supplying such equipment, helping businesses across China and beyond to optimize their material handling operations and achieve greater productivity.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top