For businesses in the food processing industry, especially those dealing with peanut products, the efficient handling and transportation of peanut powder is a critical aspect of production. A peanut powder conveyor is a specialized piece of equipment designed to move bulk peanut powder from one location to another within a processing facility. This equipment is essential for maintaining production flow, ensuring product quality, and enhancing operational efficiency. In this article, we will delve into what a peanut powder conveyor is and explore the key design principles that make it effective for handling this specific material.
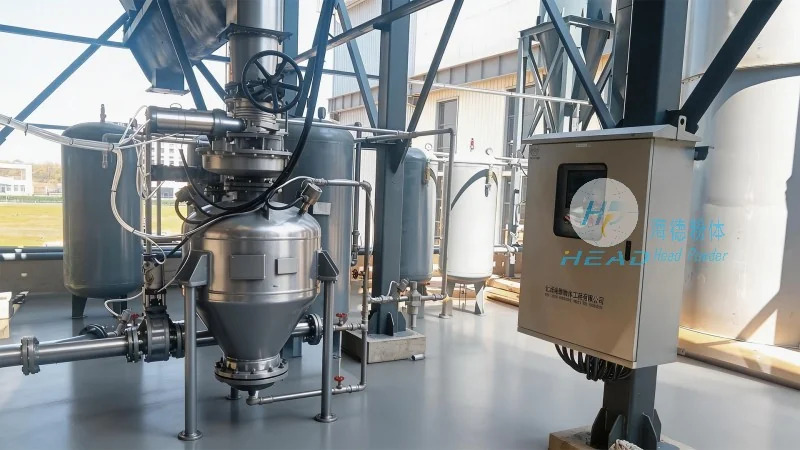
A peanut powder conveyor is a type of bulk material handling equipment specifically engineered to transport peanut powder. Unlike traditional conveyors that handle solid or semi-solid materials, a peanut powder conveyor is designed to manage fine, powdery substances like peanut flour or ground peanuts. The primary function of this equipment is to move the powder from a storage silo or processing area to a packaging or further processing unit. This process is crucial for maintaining a continuous production line and reducing manual handling, which can lead to contamination or loss of product.
The design of a peanut powder conveyor is based on several critical principles to ensure optimal performance with peanut powder. These principles include material compatibility, dust control, and efficient flow management. Material compatibility is paramount because peanut powder can be sensitive to certain materials that might cause contamination or degrade the product. Therefore, the conveyor components, such as the hopper, conveyor belt, and housing, are typically made from food-grade materials like stainless steel or food-safe plastics. This ensures that the peanut powder remains pure and free from any unwanted residues.
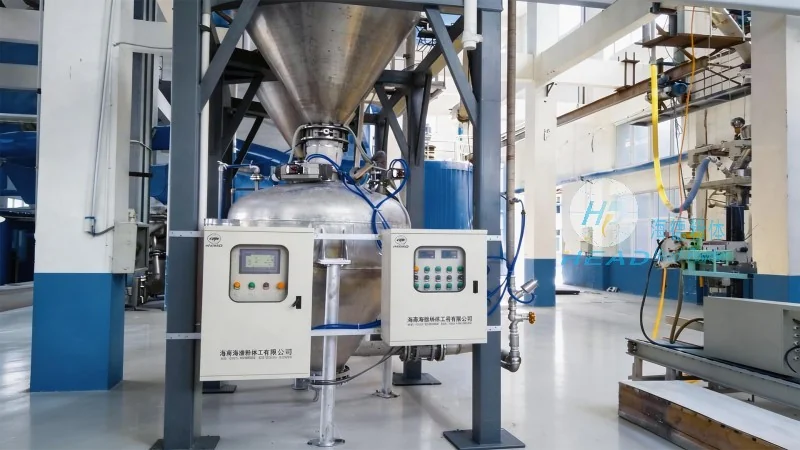
Dust control is another essential design principle. Peanut powder is a fine material that can easily generate dust, which not only poses health risks to workers but also can lead to product loss and equipment damage. Peanut powder conveyors are equipped with sealed housing and dust collection systems to minimize dust emissions. The design often includes features like airtight seals and integrated dust filters to capture and contain the powder, ensuring a clean and safe working environment.
Efficient flow management is critical for the smooth operation of a peanut powder conveyor. The design incorporates elements like a properly sized hopper with a sloped bottom to prevent material bridging or caking. The conveyor belt or screw mechanism is engineered to provide consistent and uniform movement of the powder, preventing blockages and ensuring a steady flow rate. Additionally, the conveyor may include adjustable speed controls and sensors to monitor the flow and adjust as needed, optimizing the handling process for different peanut powder compositions and production demands.
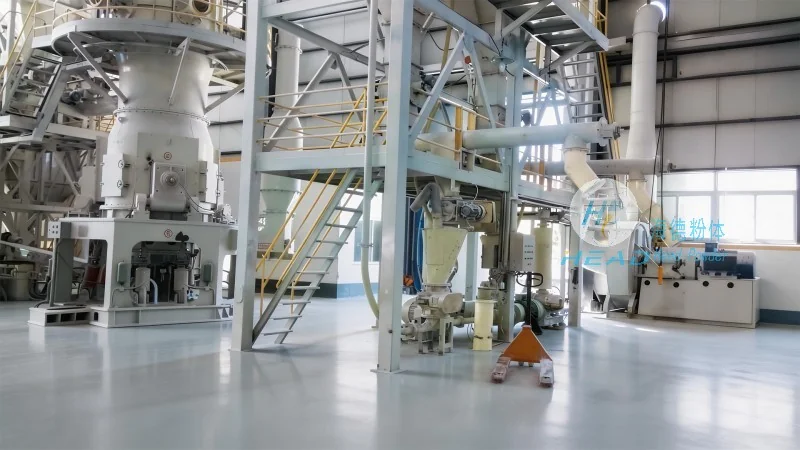
The structure of a peanut powder conveyor typically consists of several key components that work together to facilitate the transport of peanut powder. The main components include a hopper, a conveyor mechanism (such as a screw or belt), a drive system, and a control panel. The hopper is the upper part of the conveyor where the peanut powder is loaded. It is designed with a wide opening to allow easy loading and a sloped interior to facilitate the flow of the powder into the conveyor mechanism. The conveyor mechanism, which can be a screw conveyor or a belt conveyor, is responsible for moving the powder along the length of the conveyor. The drive system provides the necessary power to operate the conveyor, and the control panel allows operators to adjust settings such as speed and direction.
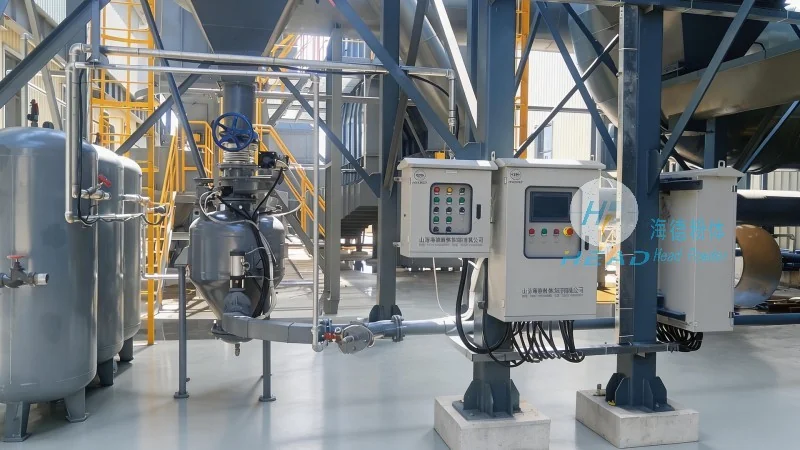
Implementing a peanut powder conveyor in a peanut processing facility offers several benefits. Firstly, it enhances operational efficiency by automating the material handling process, reducing the need for manual labor and minimizing the risk of product loss or contamination. Secondly, it improves product quality by maintaining a consistent flow of powder, which helps in achieving uniform product characteristics. Thirdly, it ensures a safer working environment by reducing dust exposure and minimizing the risk of accidents associated with manual handling of bulk materials. Additionally, the design of peanut powder conveyors allows for easy integration into existing production lines, making it a versatile solution for various peanut processing applications.
In conclusion, a peanut powder conveyor is a vital piece of equipment for the efficient handling and transportation of peanut powder in food processing facilities. Its design is based on principles of material compatibility, dust control, and efficient flow management, ensuring that it can handle the unique properties of peanut powder effectively. By understanding these design principles and the components of a peanut powder conveyor, businesses can make informed decisions about implementing this equipment to enhance their production processes. The benefits of using such equipment, including improved efficiency, product quality, and safety, make it an essential investment for any peanut processing operation.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top