What is a Small Bag Weighing and Quantitative Powder Conveying Line? What Are Its Design Principles?
Release time:2026-09-15 16:01:17
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Manager Zhang
Small bag weighing and quantitative powder conveying lines are specialized industrial systems designed for the precise handling, weighing, and packaging of bulk powders. These systems are widely used in various industries, including pharmaceuticals, food processing, chemicals, and manufacturing, where accurate measurement and consistent quality of powders are critical. The primary function of such a line is to ensure that each bag is filled with the exact required weight of material, minimizing waste and maximizing efficiency in production processes.
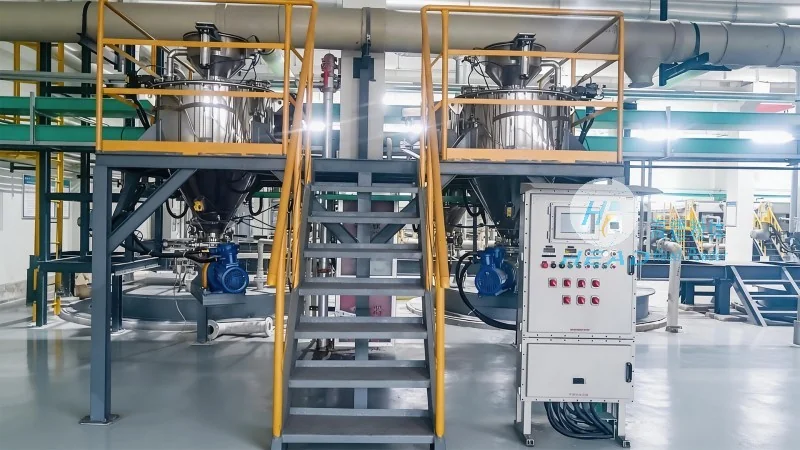
Key Components of a Small Bag Weighing and Quantitative Powder Conveying Line
The design of a small bag weighing and quantitative powder conveying line typically involves several key components that work in concert to achieve accurate and reliable operation. These components include:
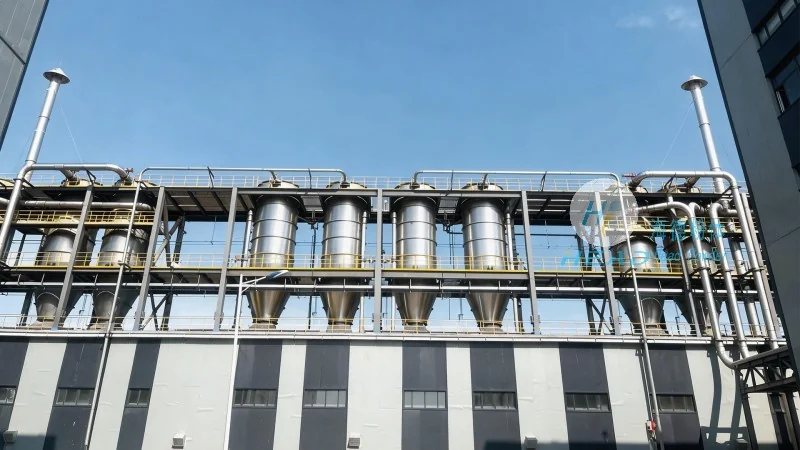
- Pneumatic Conveying System: This system is responsible for transporting the bulk powder from the storage silo or hopper to the weighing and filling station. It uses air pressure to move the powder through a network of pipes, ensuring a consistent flow rate and preventing material degradation.
- Weighing Scale: The core of the quantitative process, the weighing scale is equipped with high-precision load cells that measure the weight of the powder as it is being filled into the bag. Modern scales often use digital technology to provide real-time weight data and can be integrated with control systems for automated operation.
- Bag Filling and Sealing Unit: This component is responsible for filling the bag with the measured amount of powder and then sealing it to prevent contamination or spillage. It may include mechanisms such as bag openers, fill nozzles, and sealing devices (e.g., heat sealers or tape sealers).
- Control System: A sophisticated control system manages the entire operation, coordinating the movement of the powder, the weighing process, and the filling/sealing actions. It often includes programmable logic controllers (PLCs) and human-machine interfaces (HMIs) that allow operators to set parameters, monitor performance, and troubleshoot issues.
Design Principles of Small Bag Weighing and Quantitative Powder Conveying Lines
The design principles of these lines are centered on precision, efficiency, and reliability. Key design considerations include:
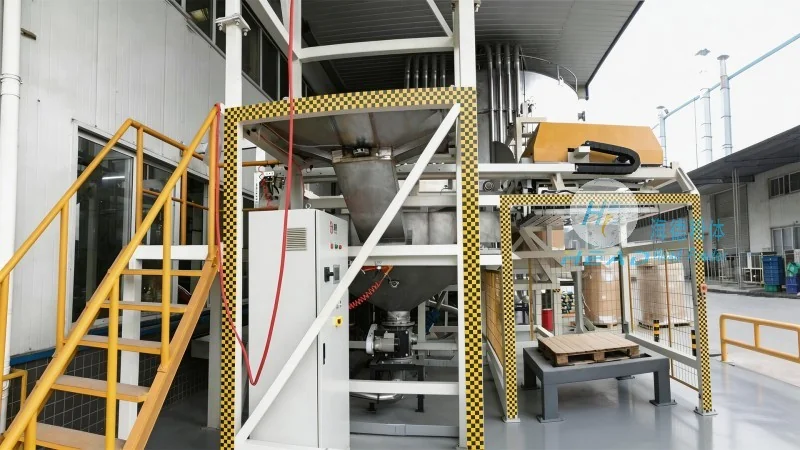
- Precision and Accuracy: The primary design principle is to achieve high levels of accuracy in weighing and filling. This is achieved through the use of high-precision load cells, calibration procedures, and feedback control systems that adjust the filling rate in real-time to maintain the target weight.
- Material Compatibility: The components of the system are designed to be compatible with a wide range of powders, including those that are hygroscopic, abrasive, or prone to caking. Materials such as stainless steel, food-grade plastics, and specialized coatings are used to prevent material contamination and equipment wear.
- Flow Control and Uniformity: Ensuring consistent powder flow is crucial for accurate weighing. The design incorporates features such as airlocks, rotary valves, and adjustable air pressure to maintain a uniform flow rate, preventing surges or drops that could affect the weight measurement.
- Automation and Integration: Modern designs emphasize automation to reduce labor costs and improve consistency. The control system integrates all components, allowing for fully automated operation from bag loading to sealing, with minimal human intervention.
Applications and Benefits of Small Bag Weighing and Quantitative Powder Conveying Lines
Small bag weighing and quantitative powder conveying lines are used in a variety of applications across different industries. In the pharmaceutical industry, they are essential for packaging active pharmaceutical ingredients (APIs) and excipients with strict weight tolerances. In the food industry, they are used for packaging flour, sugar, spices, and other food powders, ensuring consistent product quality and meeting regulatory requirements. In the chemical industry, they are used for packaging raw materials and intermediates, where precise dosing is critical for process control.
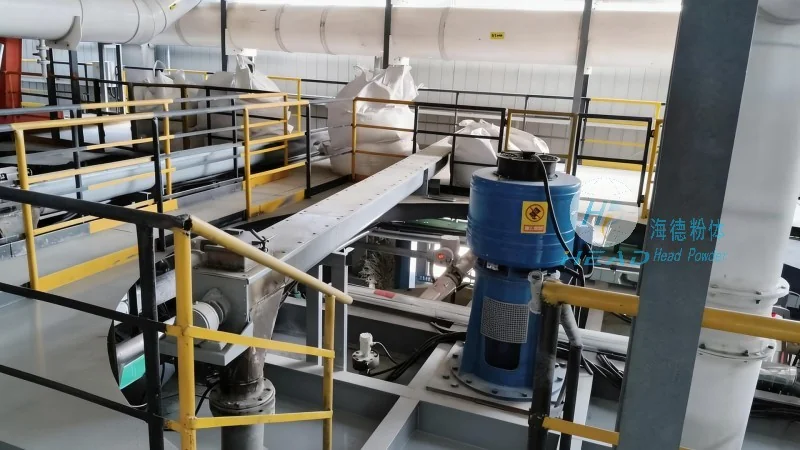
The benefits of using such systems include improved product quality through consistent weight and purity, reduced material waste due to accurate filling, increased production efficiency through automation, and enhanced safety through enclosed systems that minimize dust exposure and prevent contamination.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China
