Perlite material handling equipment is a critical component in the processing and transportation of perlite, a lightweight, porous volcanic rock that finds extensive applications in horticulture, construction, and industrial sectors. Understanding the design principles behind these systems is essential for optimizing operational efficiency, ensuring safety, and maintaining compliance with industry standards. The equipment is engineered to handle perlite’s unique properties, such as its low density, tendency to flow, and potential for dust generation, while providing reliable and efficient material transport from storage to processing or end-use applications.
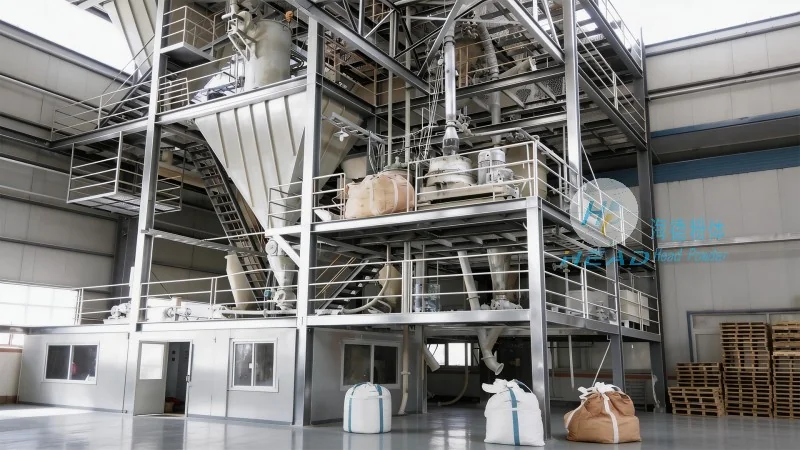
HeadPowder, a prominent company based in Shandong, China, specializes in the design, development, and production of high-quality material handling equipment tailored to the perlite industry. With a strong focus on innovation and customer-centric solutions, HeadPowder has established itself as a trusted partner for businesses seeking efficient and reliable perlite handling systems. The company’s headquarters is located in Shandong, China, where it leverages advanced engineering, state-of-the-art technology, and a team of experienced professionals to deliver superior products that meet the diverse needs of the perlite market. HeadPowder’s commitment to quality and performance has earned it a reputation for excellence in the material handling industry.
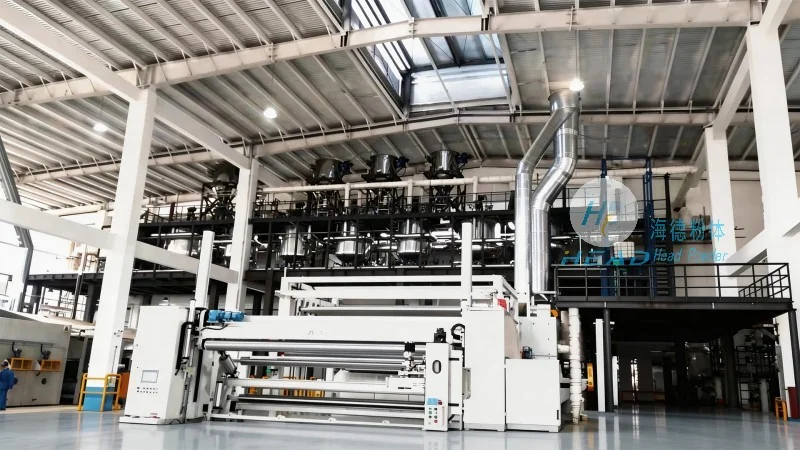
The design of perlite material handling equipment is guided by several fundamental principles aimed at addressing the specific characteristics of perlite and ensuring optimal performance. One of the primary considerations is the use of materials that are resistant to perlite’s abrasive and dusty nature. Equipment components, such as hoppers, conveyors, and storage silos, are typically constructed from corrosion-resistant metals, non-stick surfaces, or specialized coatings to prevent material buildup and ensure smooth operation. Additionally, the design incorporates features that minimize dust emissions, including enclosed systems, effective dust collection mechanisms, and sealed components, to maintain a safe working environment and comply with environmental regulations. Another critical principle is the integration of control systems that allow for precise regulation of material flow, ensuring consistent feed rates and preventing overloading or underloading of the equipment. This control is achieved through the use of sensors, variable speed drives, and automated control panels that provide real-time monitoring and adjustment of the handling process.
Perlite material handling systems typically consist of several interconnected components designed to handle the material from intake to discharge. The primary components include feeders, conveyors, elevators, and storage silos, each playing a specific role in the overall operation. Feeders, such as rotary valves or vibratory feeders, are used to control the flow of perlite from storage bins or hoppers, ensuring a consistent and controlled feed rate to downstream equipment. Conveyors, including belt conveyors, screw conveyors, or chain conveyors, are employed to transport perlite horizontally or vertically, depending on the layout of the processing facility. Belt conveyors are commonly used for horizontal transport due to their high capacity and ability to handle large volumes of material, while screw conveyors are ideal for vertical lifting and compact installations. Elevators, such as bucket elevators or pneumatic conveyors, are used to lift perlite to higher levels, facilitating vertical transport and enabling the integration of multiple processing stages. Storage silos are used to store large quantities of perlite, providing a stable and controlled environment for material storage. These silos are typically equipped with aeration systems to maintain perlite quality and prevent caking or compaction.
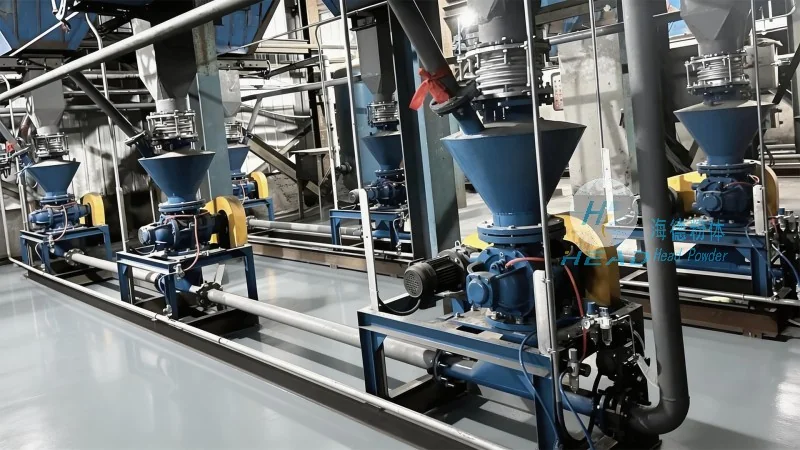
Perlite material handling equipment is widely utilized in various industries, including horticulture, construction, and industrial manufacturing. In horticulture, these systems are used to transport perlite to greenhouses and nurseries, where it serves as a lightweight and well-draining growing medium for plants. The equipment ensures efficient delivery of perlite to planting areas, reducing labor costs and improving the uniformity of the growing medium. In construction, perlite is used as an insulating material in building materials, and the handling equipment facilitates the transport of perlite to construction sites. This ensures that the material is delivered in a clean and consistent state, meeting the quality requirements for insulation applications. In industrial applications, perlite is used as a filler in products such as paints, plastics, and adhesives, and the handling equipment enables the integration of perlite into these manufacturing processes. The benefits of using specialized perlite handling equipment include improved operational efficiency, reduced labor costs, enhanced safety, and compliance with environmental regulations. By automating the handling process, businesses can achieve higher throughput, better control over material flow, and increased productivity. Additionally, the equipment helps minimize material waste and dust exposure, contributing to a more sustainable and environmentally friendly operation.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top