Dilute phase material handling equipment is a critical component in various industrial processes, designed to transport bulk materials in a low concentration state. This type of equipment is widely used in industries such as cement, chemical, and mining, where efficient and reliable material transport is essential for operational efficiency. The core function of dilute phase systems is to move powders or granular materials through a pipeline using a high-velocity gas stream, creating a suspension that allows for smooth and continuous transport.
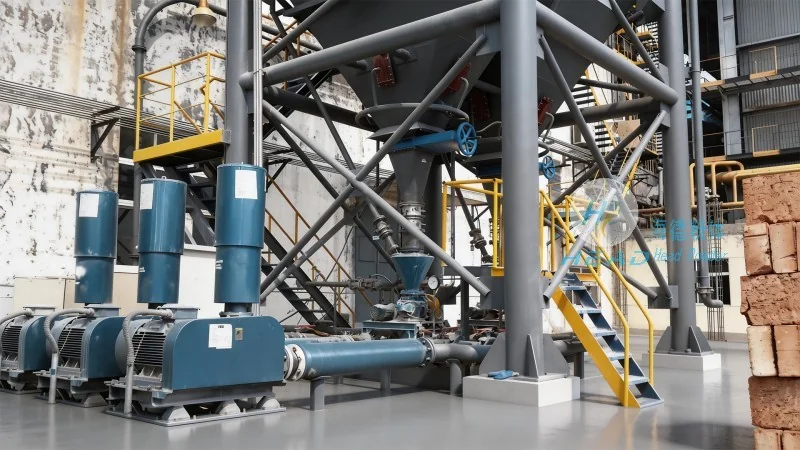
The design of dilute phase material handling equipment is based on several fundamental principles that ensure optimal performance and efficiency. The primary principle is the creation of a stable suspension of the material in the gas stream. This is achieved by maintaining a specific gas velocity that is sufficient to keep the particles in suspension while minimizing pressure drop and energy consumption. Another crucial design principle is the selection of appropriate components, including the feeder, pipeline, and separator. The feeder must be capable of delivering the material at a consistent rate, while the pipeline must be sized and configured to handle the flow without excessive friction losses. The separator, typically a cyclone or bag filter, is designed to separate the material from the gas stream at the end of the transport line, ensuring that the material is recovered and the gas is cleaned before being recirculated or discharged.
Understanding the individual components of a dilute phase material handling system is essential for grasping how the equipment operates. The feeder is the first component in the system, responsible for feeding the material into the pipeline. There are various types of feeders, including rotary valves, star feeders, and screw feeders, each designed for specific material characteristics and flow rates. The pipeline is the main conduit through which the material and gas are transported. It is typically made of materials such as stainless steel or plastic, depending on the material being handled and the operating conditions. The pipeline must be designed to minimize pressure drop, which is a key factor in energy efficiency. The separator is the final component, responsible for separating the material from the gas. This is typically achieved through centrifugal force in a cyclone separator or by filtration in a bag filter. The separated material is collected and can be reused in the process, while the gas is cleaned and either recirculated back into the system or discharged to the atmosphere.
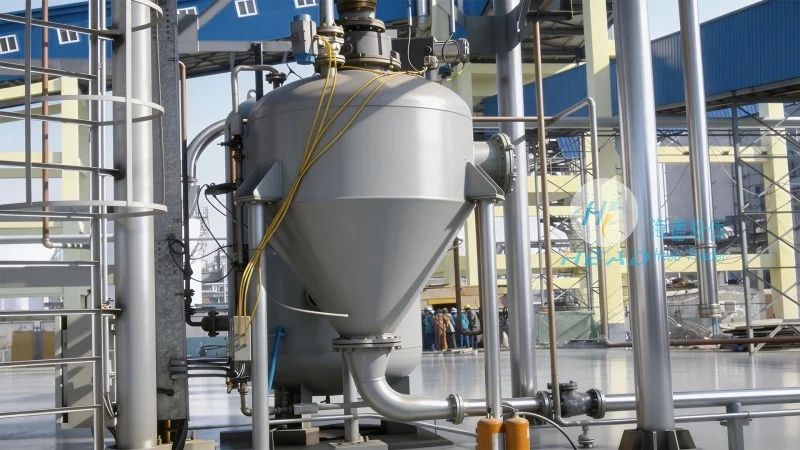
There are several advantages to using dilute phase material handling equipment in industrial applications. One of the main advantages is the high efficiency of material transport. By using a high-velocity gas stream, the equipment can transport materials over long distances with minimal pressure drop, reducing energy consumption compared to other methods such as pneumatic conveying with higher material concentrations. Another advantage is the ability to handle a wide range of materials, from fine powders to coarse granules. The design of the system can be adjusted to accommodate different particle sizes and flow rates, making it versatile for various industrial needs. Additionally, dilute phase systems are generally more cost-effective to install and maintain compared to other material handling methods, as they require less complex infrastructure and can be integrated into existing processes with relative ease.
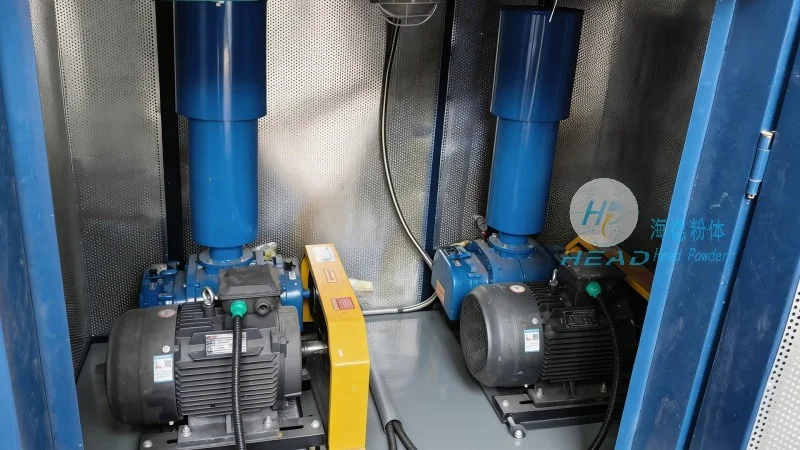
Dilute phase material handling equipment is used in a variety of industrial applications where the transport of bulk materials is required. In the cement industry, for example, these systems are used to transport raw materials such as limestone and clay from storage silos to the production line. In the chemical industry, they are used to transport powders and granules used in the manufacturing of chemicals, pharmaceuticals, and other products. In the mining industry, they are used to transport ore and other materials from the mine to processing facilities. The versatility of dilute phase systems makes them suitable for a wide range of applications, from small-scale operations to large-scale industrial plants.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of dilute phase material handling equipment. The company is based in Shandong, China, and has a strong reputation for providing high-quality, reliable equipment that meets the needs of various industrial sectors. HeadPowder specializes in the design, manufacturing, and installation of dilute phase systems, with a focus on providing customized solutions for each client's specific requirements. The company's products are known for their durability, efficiency, and ease of maintenance, making them a preferred choice for many industrial applications. HeadPowder's team of engineers and technicians are experienced in the design and operation of dilute phase systems, and they work closely with clients to ensure that the equipment is optimized for their specific processes. The company also provides after-sales support, including maintenance and repair services, to ensure that the equipment operates at peak performance throughout its lifespan.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top