Soil powder conveying systems are specialized equipment designed to transport soil and other fine particulate materials efficiently and safely. These systems are crucial in various industries, including construction, mining, and environmental remediation, where the handling of loose, powdery soil is a common requirement. Understanding the components and design principles of such systems is essential for optimizing material handling processes and ensuring operational efficiency.
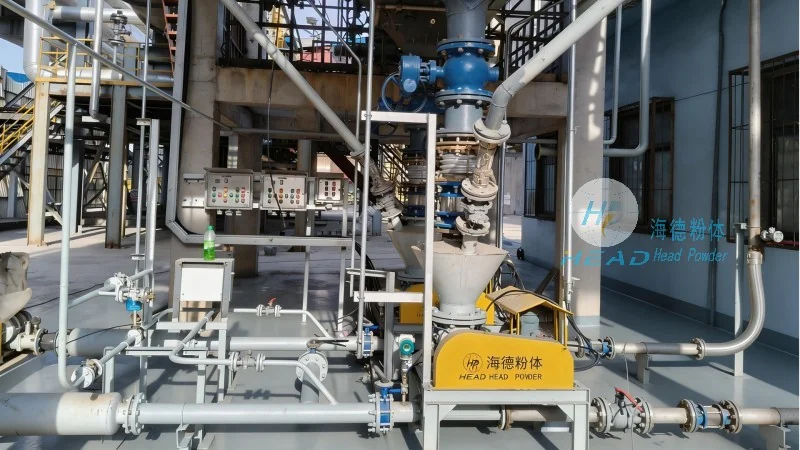
At the core of soil powder conveying systems is the ability to move fine soil particles from one location to another without significant loss or degradation. These systems are engineered to address the unique challenges of handling powdery materials, which can be prone to dust generation, clogging, and uneven flow. The design of these systems incorporates advanced engineering principles to ensure reliable and consistent performance in demanding environments.
The primary components of a soil powder conveying system typically include a hopper for material storage, a conveyor mechanism (such as a screw conveyor or pneumatic duct), a control system for regulating flow, and a dust collection or filtration unit to manage airborne particles. Each component plays a critical role in the overall functionality of the system. The hopper is designed to hold the soil powder in a contained manner, preventing spillage and ensuring a steady feed to the conveyor. The conveyor mechanism is the heart of the system, responsible for transporting the material through the duct or along the screw path. Control systems allow operators to adjust the speed and flow rate, adapting to varying material conditions. Finally, the dust collection unit helps maintain air quality and prevents dust from escaping into the environment.
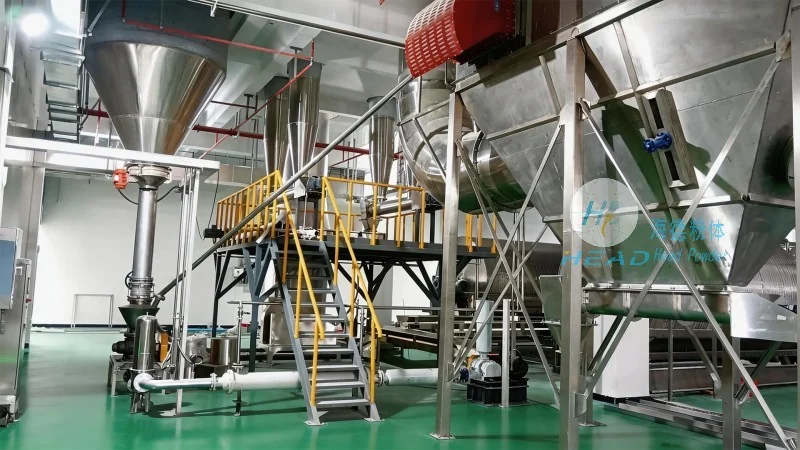
The design principles of soil powder conveying systems focus on maximizing efficiency, minimizing material loss, and ensuring safety. One key principle is the use of enclosed systems to contain dust and prevent environmental contamination. This is achieved through the use of sealed hoppers, ducts, and conveyor components that prevent air leakage and dust escape. Another important principle is the selection of appropriate conveyor types based on the properties of the soil powder. For example, screw conveyors are often used for granular or slightly cohesive materials, while pneumatic conveying systems are better suited for fine, dry powders that are prone to clogging.
Material flow optimization is another critical design consideration. Engineers design the system to ensure smooth and consistent material flow, avoiding dead zones or areas where material can accumulate and cause blockages. This involves careful consideration of the angle of the conveyor, the speed of the conveyor mechanism, and the size and shape of the ducts or screw flights. Additionally, the system is designed to handle variations in material moisture content and particle size, ensuring reliable performance under different operating conditions.
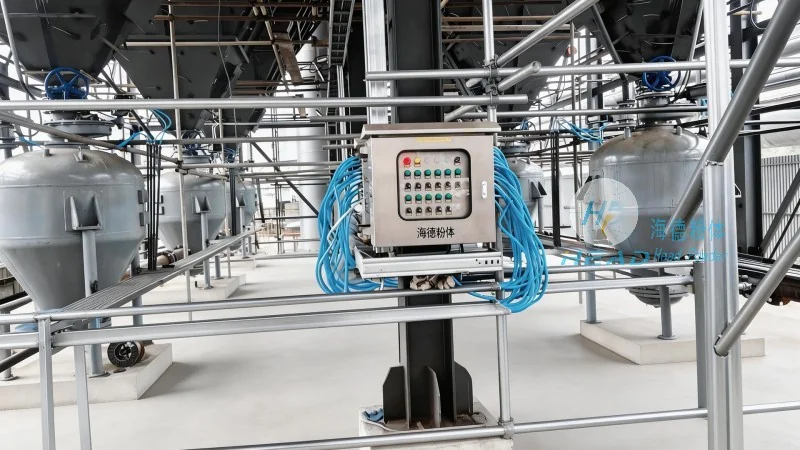
Proper operation and maintenance are essential for the long-term performance of soil powder conveying systems. Regular inspection of components such as hoppers, ducts, and conveyor mechanisms is necessary to detect and address issues like wear and tear or clogging. The control system should be calibrated regularly to ensure accurate flow regulation. Additionally, the dust collection unit must be maintained to ensure it is functioning effectively, preventing dust buildup and potential health hazards. By adhering to proper operational and maintenance practices, users can maximize the lifespan and efficiency of their soil powder conveying systems.
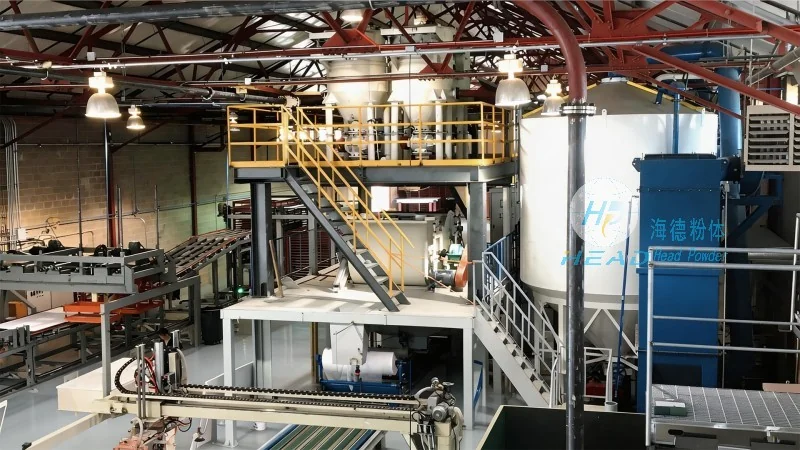
Soil powder conveying systems are widely used in various industries where the handling of fine soil particles is required. In construction, these systems are used for transporting soil from excavation sites to disposal or reuse locations. In mining, they are used to move soil and other powdery materials from processing facilities to storage or transport vehicles. In environmental remediation, they are used to handle contaminated soil during cleanup operations. The efficiency and reliability of these systems contribute significantly to the productivity and safety of operations in these industries.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of soil powder conveying systems and related equipment. With a focus on innovation and quality, the company provides customized solutions tailored to the specific needs of its clients. HeadPowder's products are designed to meet the highest standards of performance and safety, ensuring reliable operation in demanding environments. The company's commitment to customer satisfaction and technical excellence has made it a trusted partner in the industry. Located in Shandong, China, HeadPowder leverages its expertise and advanced manufacturing capabilities to deliver top-tier soil powder conveying systems to customers worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top