For industrial applications involving the handling of sulfate nickel crystal powders, a specialized conveying line is essential to ensure efficient and safe material transport. This equipment is designed to manage the unique properties of nickel sulfate crystals, which include their fine particle size, hygroscopic nature, and potential for dust generation. The sulfate nickel crystal powder conveying line is a critical component in processing facilities that rely on nickel sulfate for battery production, chemical synthesis, or other industrial processes.
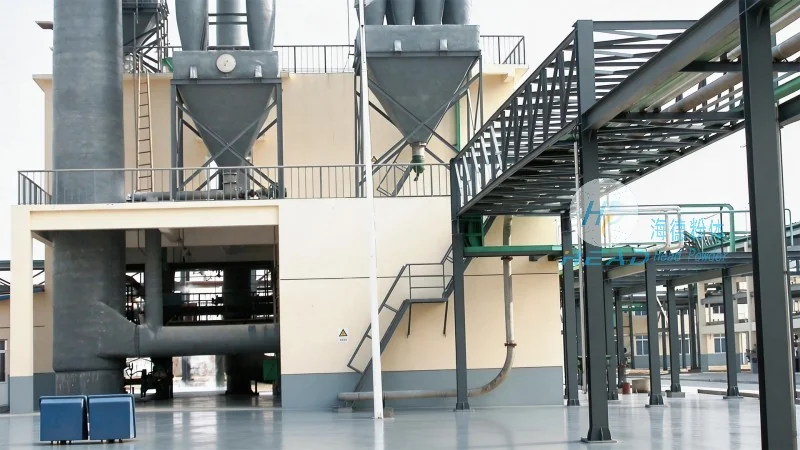
The sulfate nickel crystal powder conveying line is a system engineered to transport nickel sulfate crystals from storage or processing areas to downstream equipment such as reactors, mixers, or packaging units. It typically consists of several key components, including hoppers, feeders, conveyors (like screw or pneumatic conveyors), and control systems. The design of this line is tailored to address the challenges posed by nickel sulfate crystals, such as their tendency to clump or adhere to surfaces, which can impede smooth flow and cause blockages. By integrating advanced materials and engineering solutions, the conveying line ensures consistent and reliable material movement while minimizing operational risks.
The design principles for a sulfate nickel crystal powder conveying line are centered on optimizing material flow, maintaining product integrity, and ensuring operational safety. One of the primary design considerations is the prevention of material degradation or contamination during transport. This is achieved through the use of corrosion-resistant materials, such as stainless steel, for components that come into direct contact with the nickel sulfate crystals. The conveying system is also designed to minimize exposure to moisture and air, as nickel sulfate is hygroscopic and can absorb water, leading to changes in its physical properties. Additionally, the line incorporates features like vibration or agitation to prevent caking and ensure uniform flow of the powder.
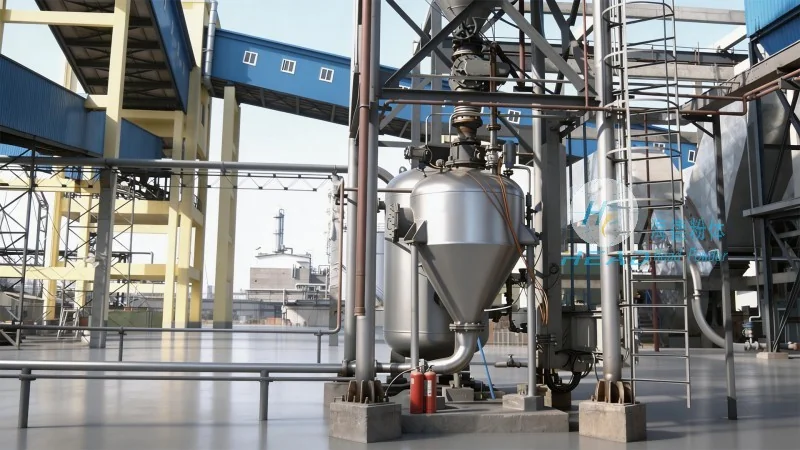
The sulfate nickel crystal powder conveying line comprises several interconnected components, each serving a specific function to facilitate efficient material handling. The hopper is the initial storage unit, designed with a sloped bottom to promote gravity-assisted flow of the crystals. It is equipped with a level indicator to monitor the material volume and a discharge valve for controlled release. The feeder, often a rotary or vibratory type, regulates the flow rate of the nickel sulfate crystals from the hopper to the conveyor. This component is critical for maintaining a consistent feed rate, preventing overloading or underloading of the conveying system. The conveyor itself, which can be either a screw conveyor or a pneumatic system, transports the material through the line. Screw conveyors are commonly used for bulk material handling due to their ability to handle high volumes and maintain a stable flow. Pneumatic conveyors, on the other hand, use air pressure to move the powder, which is advantageous for handling fine powders and minimizing dust generation. The control system integrates sensors and automation to monitor the conveying process, adjust flow rates, and alert operators to any abnormalities, ensuring smooth and safe operation.
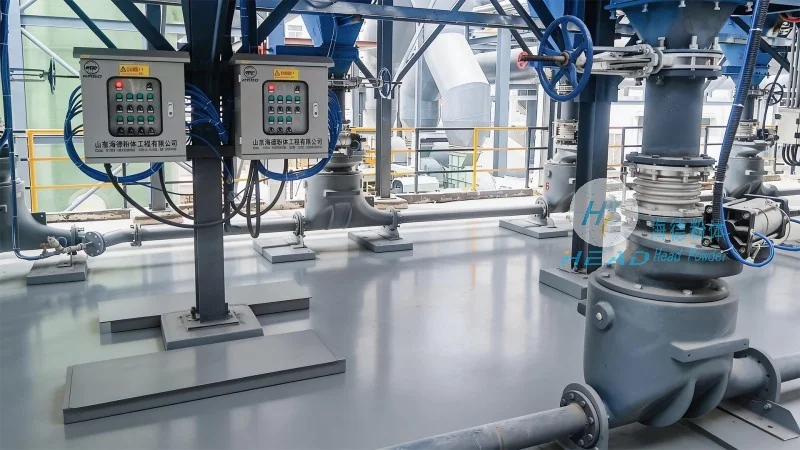
Proper operation and regular maintenance are essential to maximize the efficiency and longevity of the sulfate nickel crystal powder conveying line. Operators must follow specific guidelines to prevent issues such as clogging or material buildup. Regular cleaning of the hopper, feeder, and conveyor is necessary to remove any accumulated crystals that could cause blockages. The use of lubricants and wear-resistant parts in the feeder and conveyor components helps to extend their service life. Additionally, monitoring the temperature and humidity levels in the conveying line is important, as these factors can affect the physical properties of the nickel sulfate crystals. By adhering to these operational and maintenance practices, the conveying line can operate at optimal performance levels, ensuring consistent material transport and reducing downtime.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of specialized conveying equipment for the chemical and battery industries. With a focus on innovation and quality, HeadPowder has developed advanced sulfate nickel crystal powder conveying lines that meet the stringent requirements of modern industrial applications. The company's expertise lies in designing systems that are tailored to the unique characteristics of nickel sulfate crystals, ensuring reliable and efficient material handling. HeadPowder's facilities are located in Shandong, China, where the company leverages local resources and expertise to deliver high-quality products and services to clients worldwide. By choosing HeadPowder, industrial facilities can benefit from state-of-the-art conveying solutions that enhance productivity, reduce operational costs, and ensure compliance with safety and environmental standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top